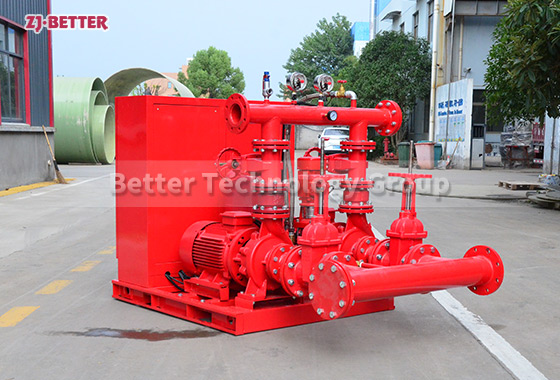
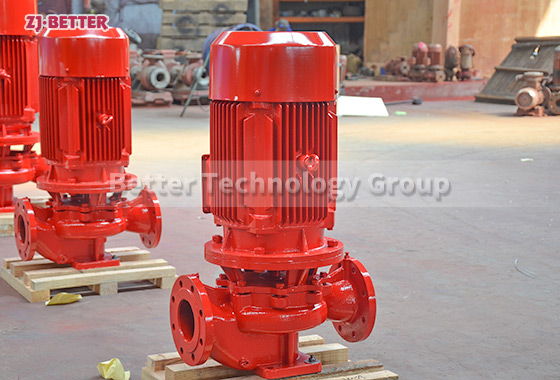
-UL Standard: Flow:100-3000 GPM Head: 90-250 PSI – NON-UL Standard: Flow:100-10000GPM Head: 40-250 PSI
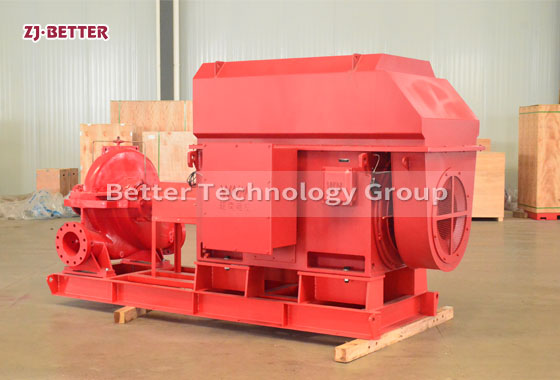
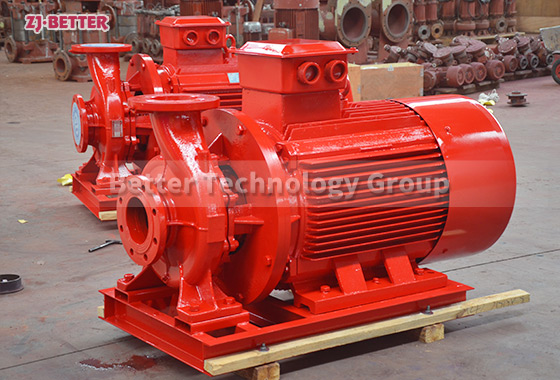
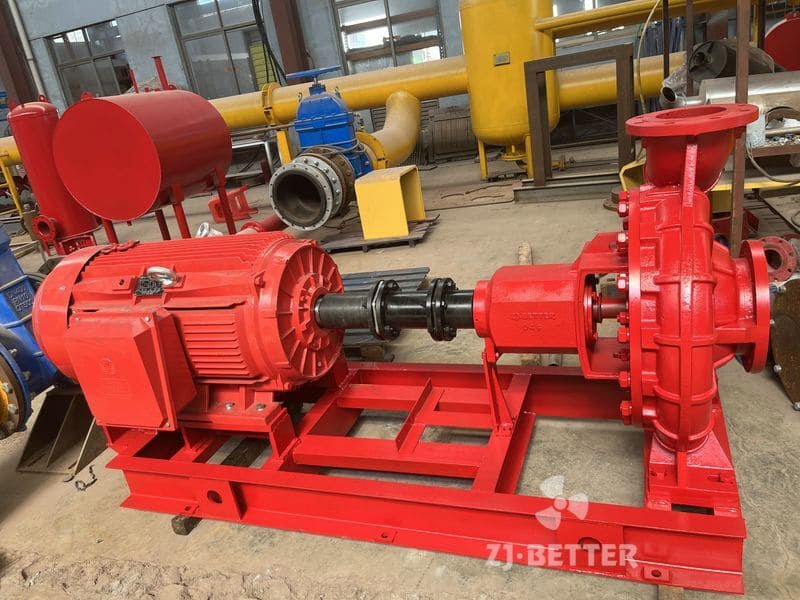
This kind of electric fire pump set is used of OTS pump with high-voltage motor driven.
Flow:50-5000 GPM Head:3-16 Bar (40-232 psi ) Power:11-1000 kw Frequency:50 or 60 Hz ISO end-suction pumps find wide application in large hotels, hospitals, schools, office buildings, supermarkets, commercial residences, subway stations, train stations, airports, various transportation tunnels, petrochemical plants, thermal power plants, oil storage tanks, large warehouses, industrial and mining enterprises, seawater injection, etc.
With proper maintenance and regular testing, an electric fire pump can have a lifespan of 20-30 years or more. Regular inspections and timely repairs are key to ensuring its longevity and reliability.
The XBD-W horizontal single-stage fire pump is a reliable and efficient fire protection solution. Designed with advanced technology, this pump offers powerful drainage capabilities and dependable performance, providing outstanding fire protection for buildings and industrial facilities. This article highlights the features and advantages of the XBD-W horizontal single-stage fire pump, explaining why it is the ideal choice for your fire suppression system.
Regular testing is crucial. Weekly churn tests, monthly flow tests, and annual full performance tests are recommended to ensure the pump operates correctly and meets required standards.
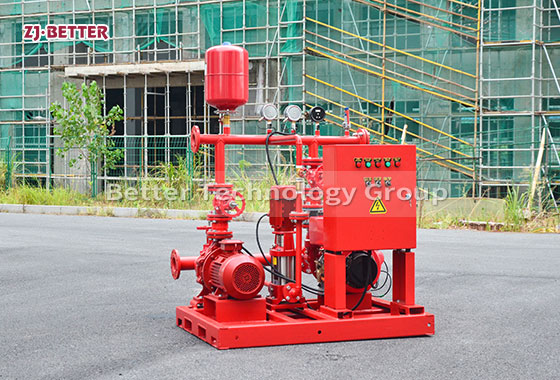
3 sets electric pump product process It is XA model, and suitable for high flow and pressure This model is 350gpm 120 psi
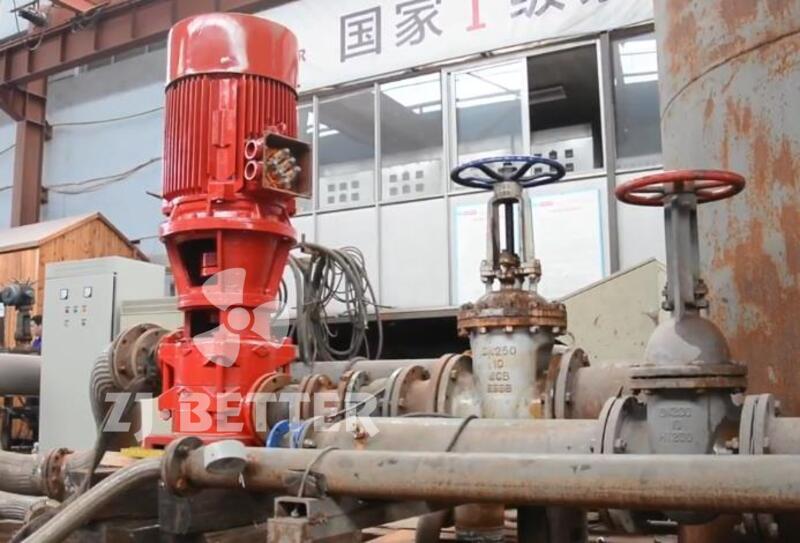
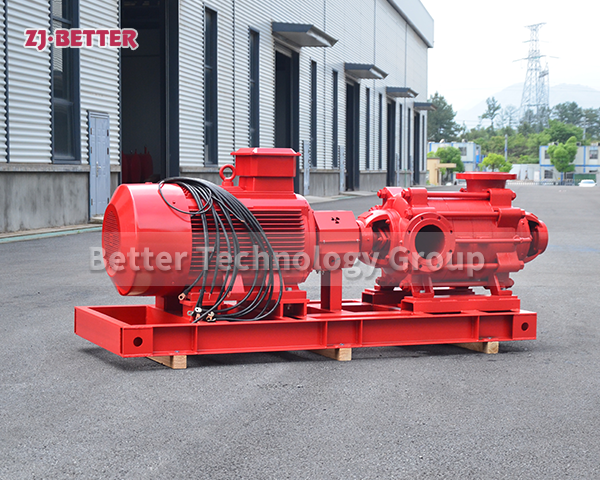
The video shows the testing for a vertical multistage fire pump. Multistage pumps can be used to meet high pressure.
Flow:50-7500 GPM Head:3-20 Bar Vertical Turbine Fire Pumps play a versatile role in various applications. They are essential in water management, agriculture for irrigation, and industrial processes dealing with different liquids. These pumps excel in emergency fire response, ensuring a swift and reliable water supply. Crucial for urban water systems, they meet the constant demand for clean water.
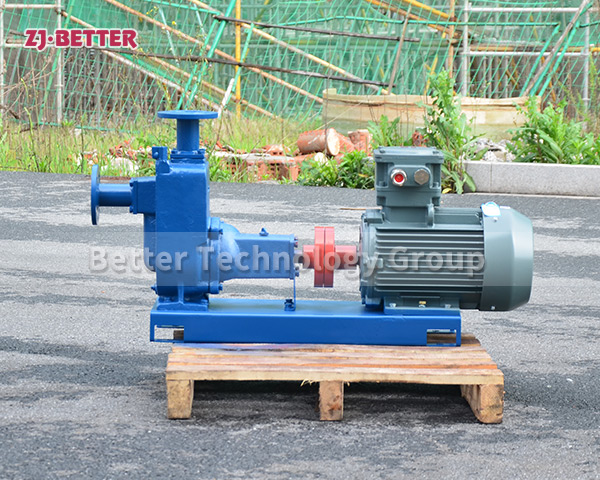
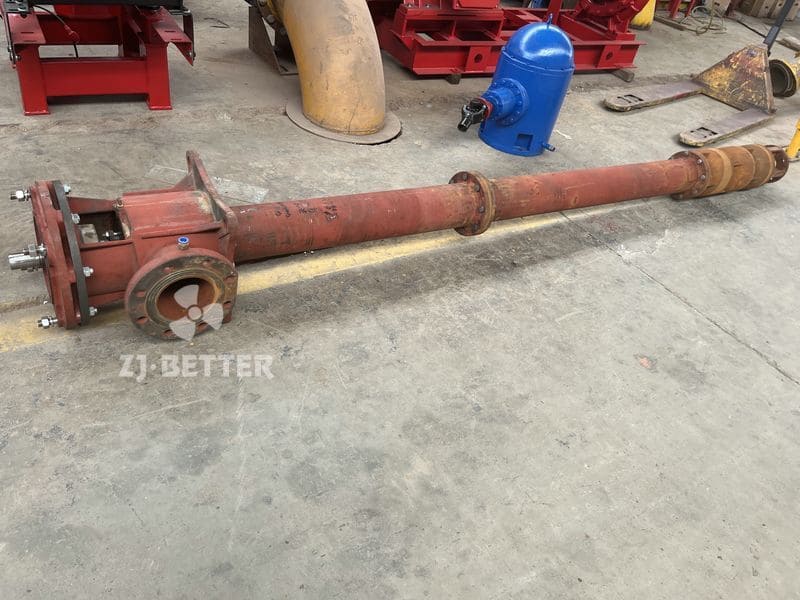
This product is a 400gpm@90psi Vertical turbine pump, which is a kind of centrifugal pump. From the perspective of centrifugal pump, it is improved from the performance of the submerged pump. This pump can be used to transport rainwater, oxidation Iron sheet water, sewage, corrosive industrial wastewater, seawater and other liquids. Widely used in water companies, sewage treatment plants, steel plants, mines and other industrial and mining enterprises, as well as municipal water supply and drainage, farmland irrigation, flood control and drainage projects.
·UL Standard: Flow:50-500GPM Head:6-16 Bar(90-230PSI) ·Non-UL Standard: Flow:50-5000 GPM Head:3-16 Bar(40-232 psi)
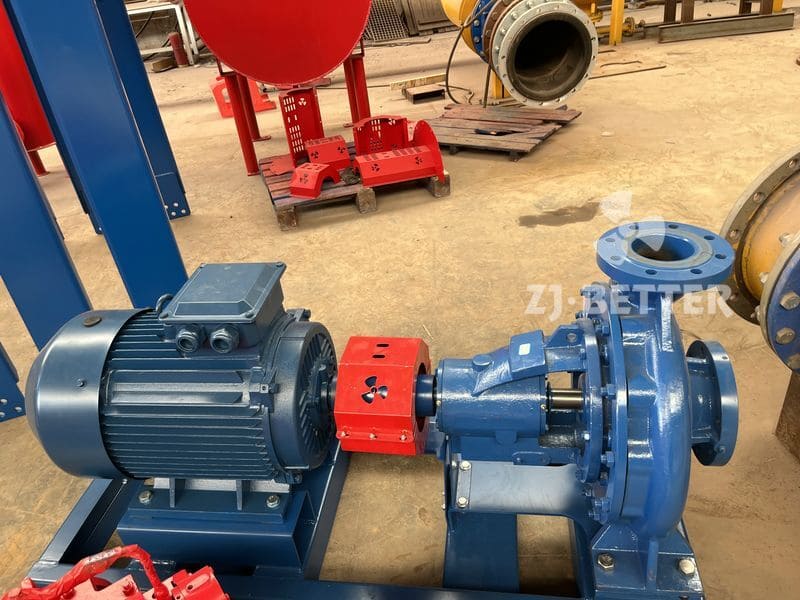
Flow:500 GPM Head:9 bar ISO end-suction pumps find wide application in industries such as chemical, petroleum, pharmaceutical, food and beverage, and water treatment, where they are used for fluid transportation, circulation systems, heating, and cooling systems, among others.
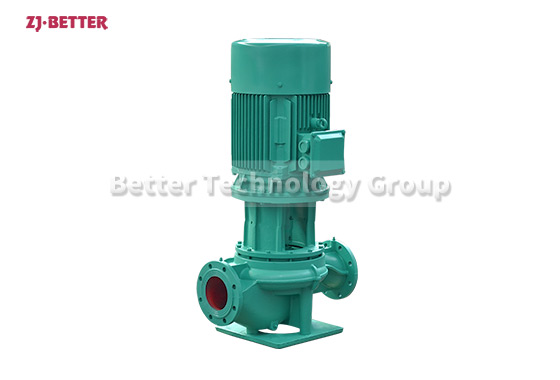
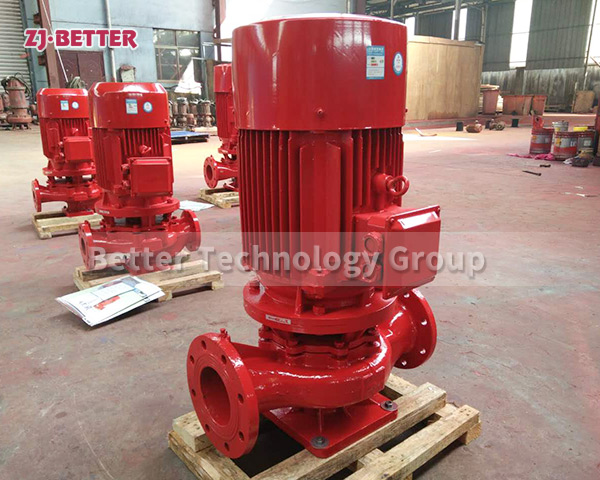
The Vertical Single stage fire pump is specifically designed for fixed fire protection systems in a wide range of settings, including businesses, construction projects, and high-rise buildings. It is a vital component in fire hydrant extinguishing systems, automatic sprinkler fire suppression systems, and more.
The Horizontal Multistage Pump is an exceptional engineering solution that offers high performance and reliability for fluid handling applications. With its unique multistage impeller design, it delivers efficient and incremental pressure boosting for high-pressure and high-flow scenarios. Whether used in water supply systems, industrial processes, irrigation, or building cooling, this pump ensures stable water pressure and flow.
The XBD-L Vertical Single stage single suction fire pump is specifically designed for fixed fire protection systems in a wide range of settings, including businesses, construction projects, and high-rise buildings. It is a vital component in fire hydrant extinguishing systems, automatic sprinkler fire suppression systems, and more. This pump set is capable of delivering clear water and water-like media with physical and chemical properties similar to water, without solid particles, at temperatures below 100°C. It is also suitable for fire protection, domestic water supply, shared water supply systems, as well as building and municipal water supply and drainage applications.
The single-suction pump sucks in horizontally and axially, and spit out radially upwards. The pump is a suspension structure, and the rotor parts can be withdrawn for maintenance without disassembling the inlet and outlet pipelines during maintenance. The pump is connected with the motor through a common elastic coupling or an extended elastic coupling, and the shaft seal of the pump is sealed with a soft packing. The bearing is a single row radial ball bearing, lubricated with lubricating oil. From the motor side, the pump rotates clockwise.
Flow:25≤Q≤5000GPM Head:50<H≤300m Speed:1500-3550 rpm Frequency:50 Hz or 60 Hz
The air conditioning circulation pump, also known as a chilled water pump, is a vital component of air conditioning systems used for circulating refrigerant or chilled water. It plays a crucial role in heat exchange and temperature regulation. The pump consists of an electric motor, pump body, impeller, sealing device, and control system. It enables the circulation of the refrigerant or chilled water to absorb or release heat, thereby achieving the desired cooling effect and regulating indoor temperatures. Key features of air conditioning pumps include high efficiency, control and automation capabilities, and diverse options to suit different system requirements. The selection of an appropriate air conditioning pump should consider specific system needs, flow rates, head pressures, and mediums. Consulting with professionals and adhering to maintenance guidelines ensures the safe and reliable operation of the pump within air conditioning systems.
The XBD-DL vertical multistage fire pump is a top-tier technology designed to enhance the safety and efficiency of building fire protection systems. With advanced design and technology, this pump offers excellent corrosion resistance and durability, making it suitable for various environmental conditions. Its high-performance turbine blade design and efficient motor ensure powerful water pressure and flow, enabling rapid and effective water delivery. The intelligent monitoring system and fault alarm function enhance the pump’s reliability and availability. By choosing the XBD-DL vertical multistage fire pump, you gain an innovative and efficient solution to enhance the safety and efficiency of your fire protection system.
The electric motor fire pump is manufactured with good structure and technology, with a wide range of performance, simple operation and long-term use. The electric motor fire pump is aimed at various fire water environments, so the selection should also be based on the actual demand environment, performance parameters, etc.
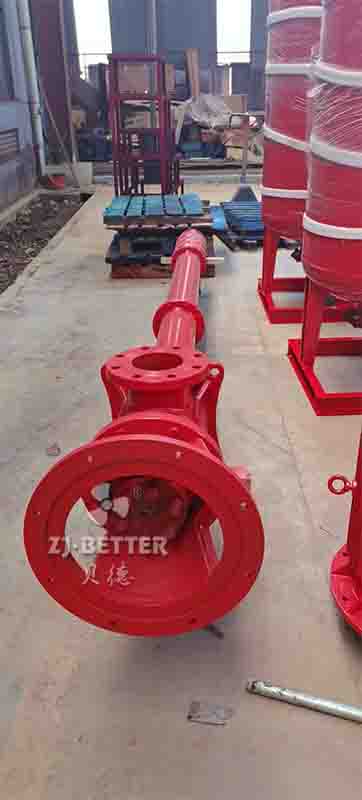
Vertical long axis pump is also called vertical long axis submerged sewage pump, which has the advantages of high efficiency and energy saving, convenient operation, low noise and easy maintenance. It can be used to transport clean water or sewage containing solid particles, such as iron filings, coal powder, sand, etc., and the transport temperature is lower than 80 ¡ãC.
Vertical multi-stage fire pumps are mainly used in engineering construction enterprises and institutions. The system includes fixed fire protection systems, indoor fire hydrant fire extinguishing systems in high-rise buildings, and automatic sprinkler fire extinguishing systems. A medium similar to water in nature, the public water supply system can be used for fire protection, life, production, construction, etc.
Electric fire pumps offer several advantages compared to other types of fire pumps, such as diesel-driven or steam-driven pumps. Here are some of the key advantages of electric fire pumps
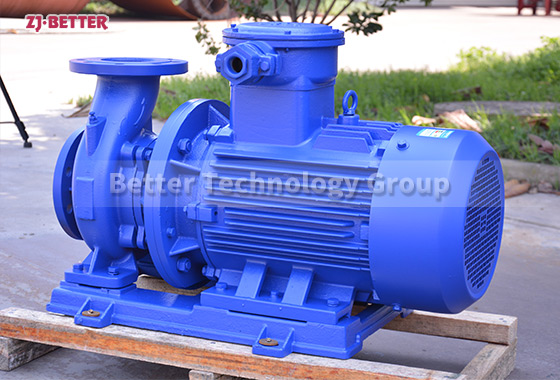
The horizontal pipeline pump is a horizontally arranged pumping device used for conveying liquids or gases. It consists of an electric motor, pump body, impeller, and sealing device. Compared to vertical pipeline pumps, the horizontal pipeline pump offers advantages such as a smaller space requirement, convenient maintenance, stable operation, and wide applicability. Its horizontal layout helps reduce axial and radial loads, thereby enhancing the pump’s stability and operational efficiency. The horizontal pipeline pump is suitable for conveying various liquids or gases and can be selected based on specific process requirements and medium characteristics. It is recommended to consult with professional engineers or pump suppliers when purchasing and using a horizontal pipeline pump to ensure the selection of suitable equipment.
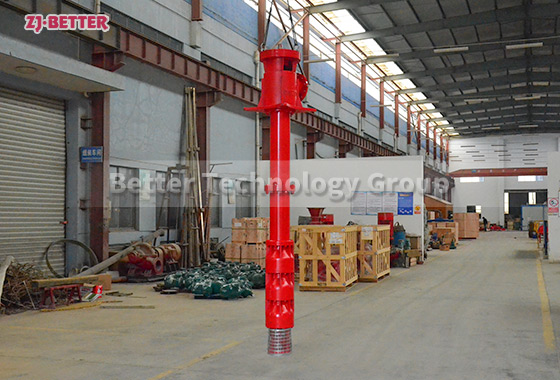
Flow:50-7500 GPM Head:3-20 Bar The Vertical Turbine Fire Pump is a high-performance engineering pump known for its unique long shaft design and exceptional capabilities. It offers advantages such as suitability for deep-buried pump stations, improved transmission efficiency, and reduced energy consumption. With excellent corrosion resistance and reliability, it can handle various fluids in diverse environments. It is a reliable solution for water supply, sewage treatment, and chemical processes.
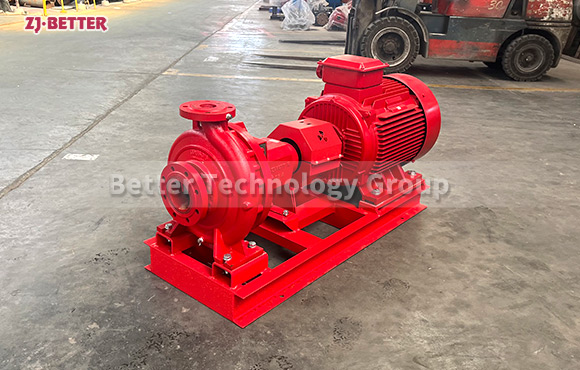
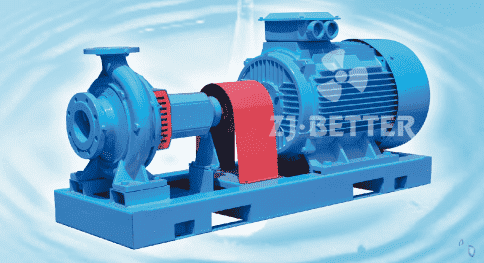
End suction centrifugal pump is a kind of centrifugal pump. Same name: end suction pump The back-pull structure allows the impeller, main shaft and bearings to be installed and replaced without removing the pump casing. The robust structure minimizes misalignment and deformation of the water pipes.
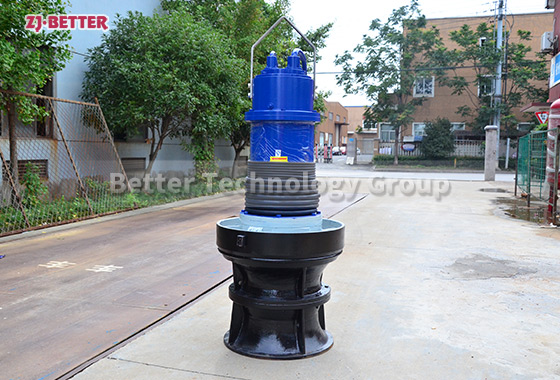
The submersible axial-flow pump is a special type of submersible pump designed for handling large flow rates with relatively low head conditions. It has a wide range of applications, including agricultural irrigation, urban water supply and drainage, municipal flood control and emergency rescue, as well as various water conservancy projects.
ISO end-suction pumps offer high efficiency, high flow capacities, and the ability to withstand high pressures. The suction inlet is designed to efficiently intake fluids, while the pump itself is constructed to be compact, making it suitable for installation and maintenance in limited spaces. They also provide multiple material options to accommodate different fluid mediums, including corrosive and high-temperature substances. ISO end-suction pumps find wide application in industries such as chemical, petroleum, pharmaceutical, food and beverage, and water treatment, where they are used for fluid transportation, circulation systems, heating, and cooling systems, among others. In conclusion, ISO end-suction pumps are reliable and efficient industrial pumps that meet global standards, making them suitable for various industries and applications.
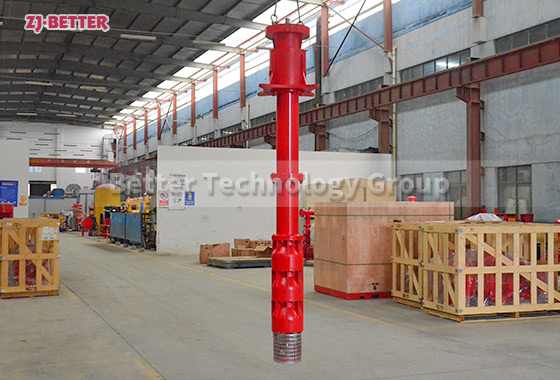
Flow:50-7500 GPM Head:3-20 Bar The long shaft pump is a high-performance engineering pump known for its unique long shaft design and exceptional capabilities. It offers advantages such as suitability for deep-buried pump stations, improved transmission efficiency, and reduced energy consumption. With excellent corrosion resistance and reliability, it can handle various fluids in diverse environments. It is a reliable solution for water supply, sewage treatment, and chemical processes.