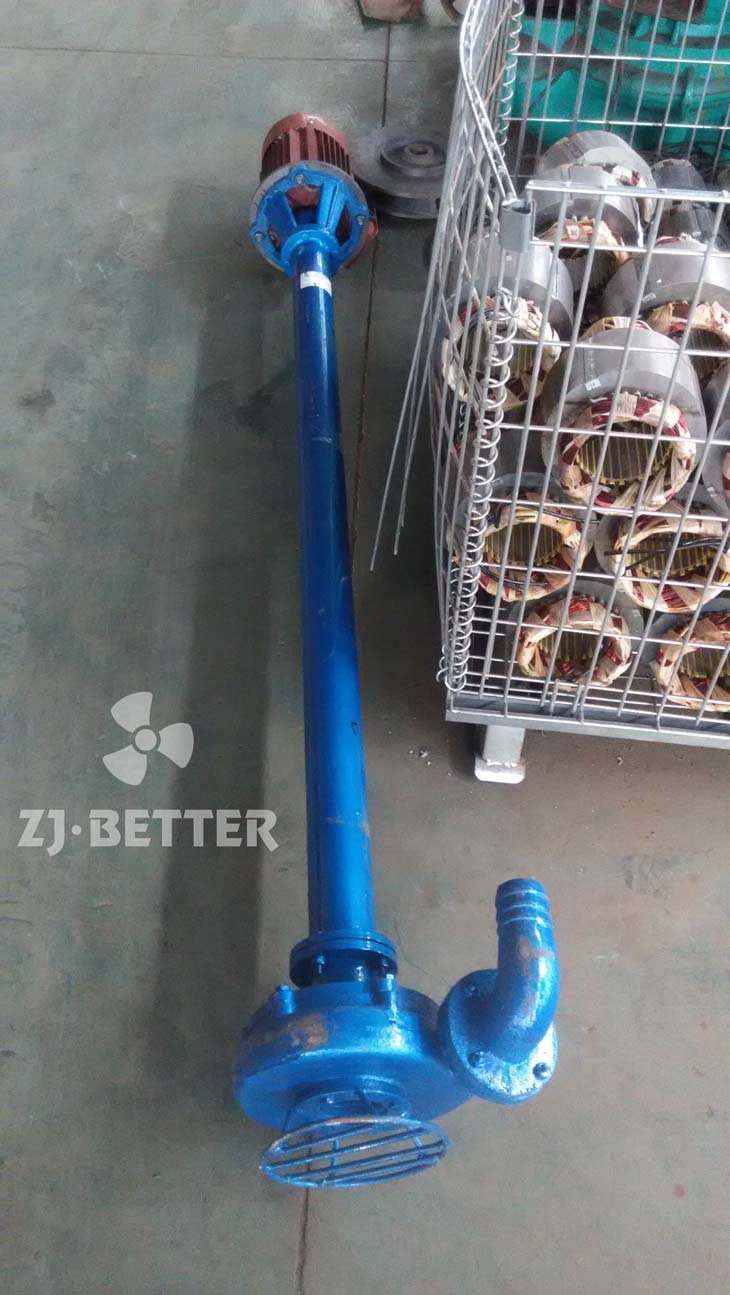
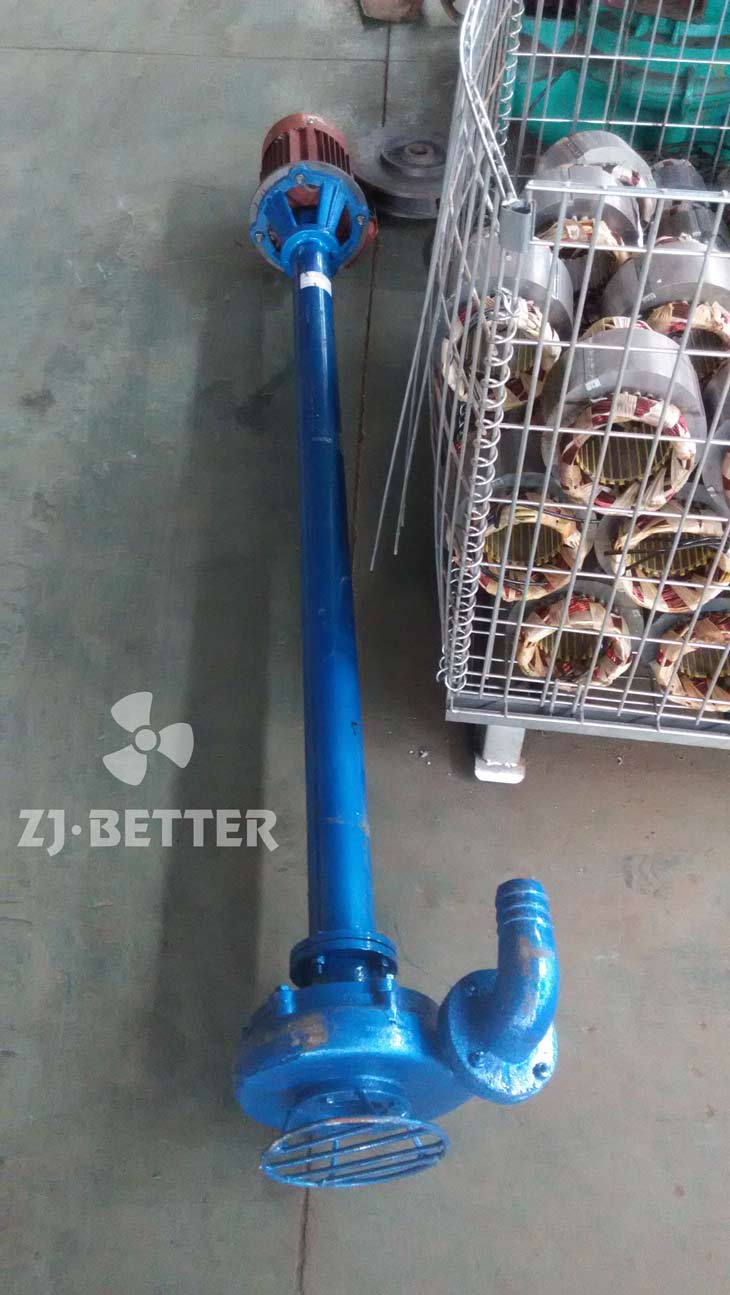
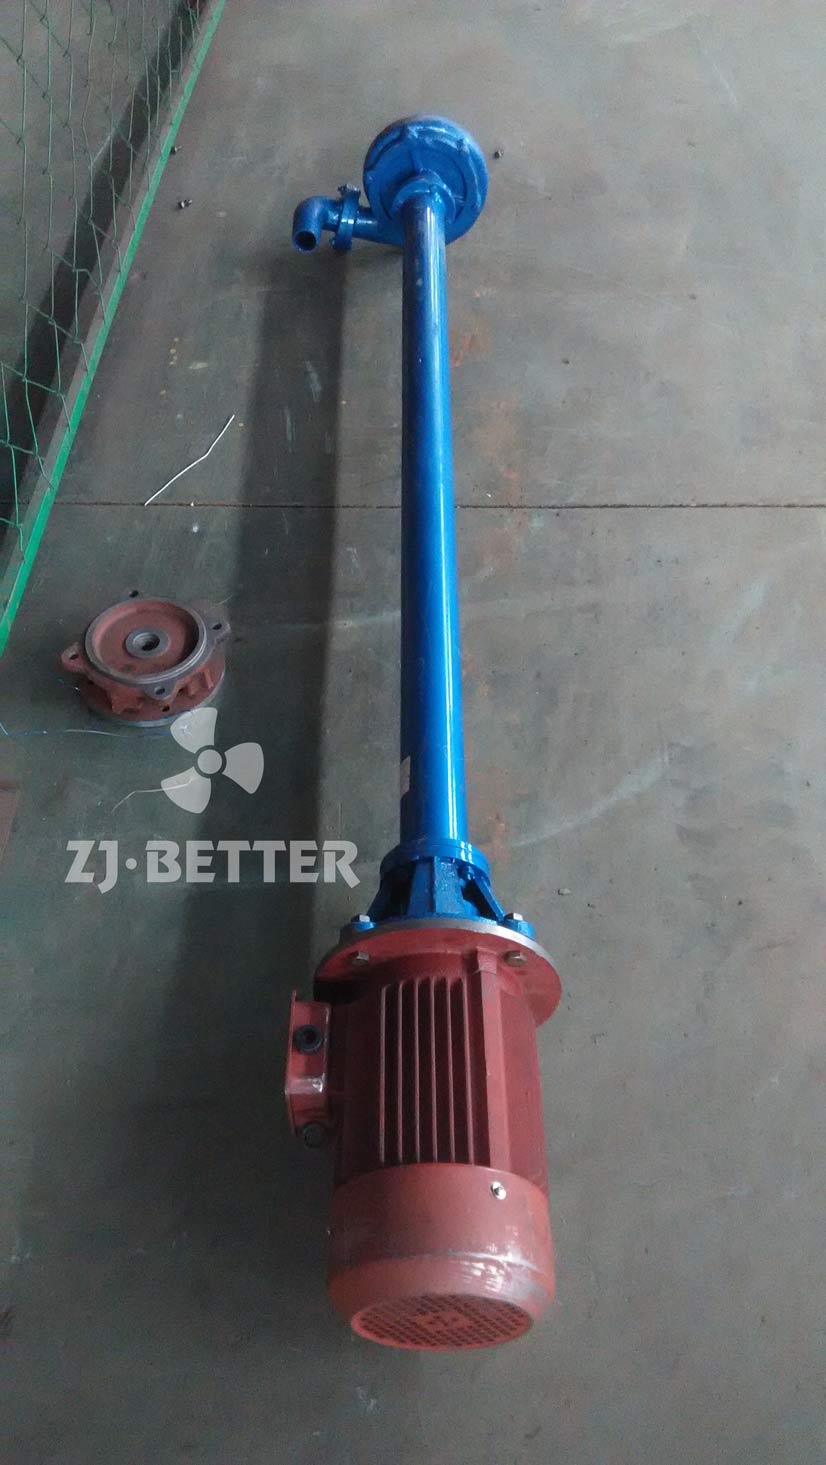
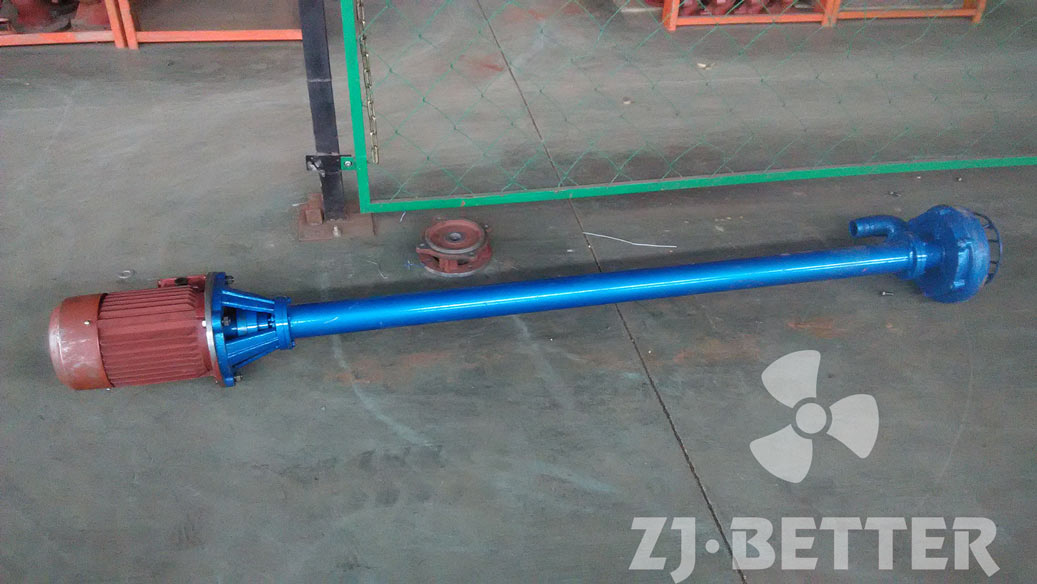
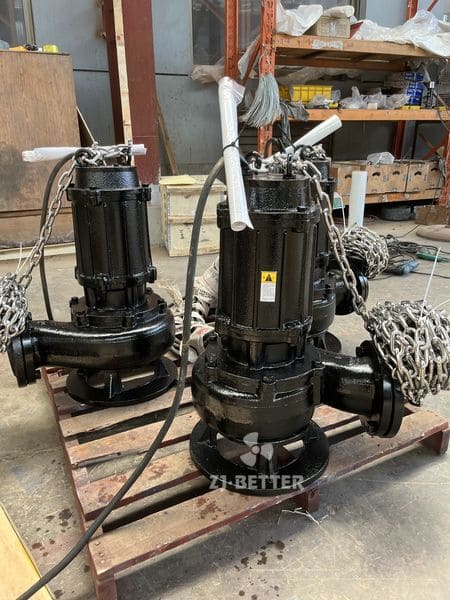
NL sewage mud pump Max flow :180m³/h Max head:16m
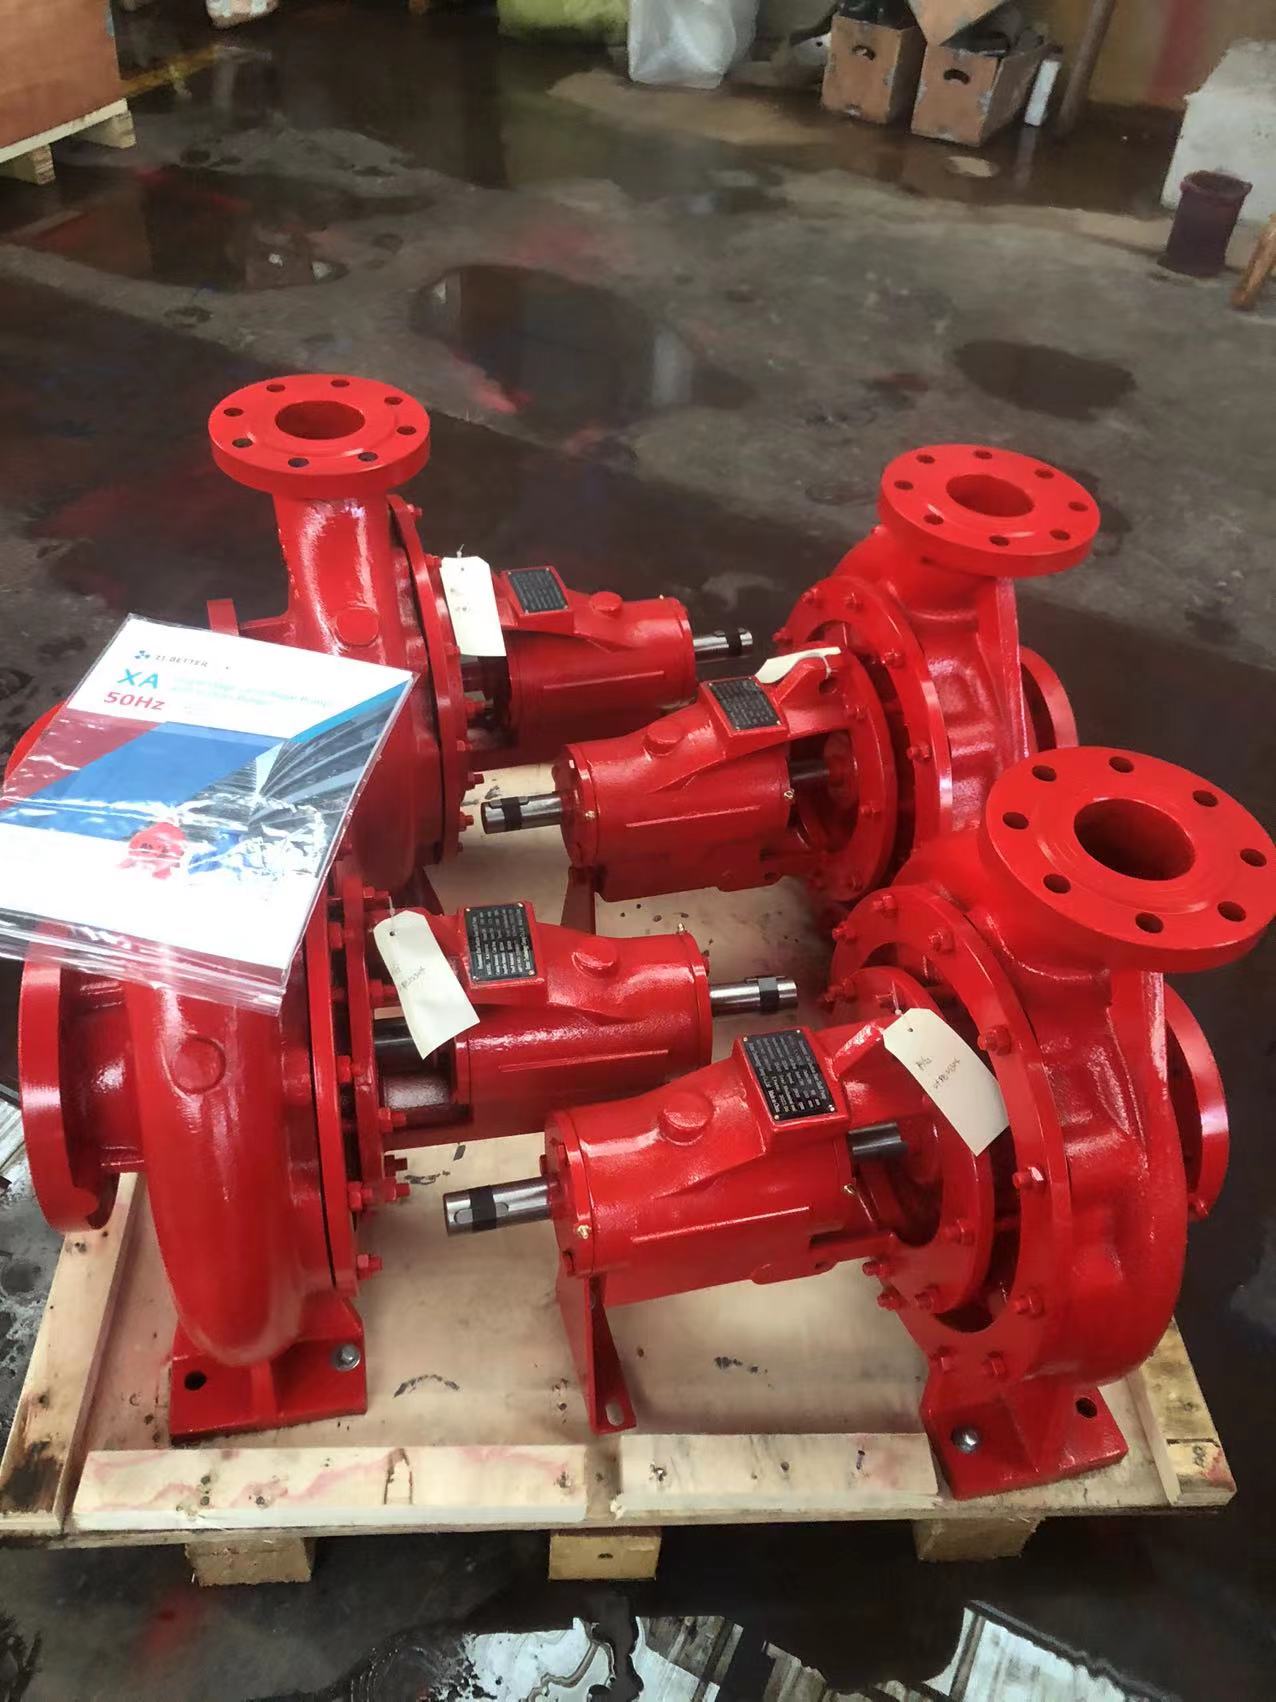
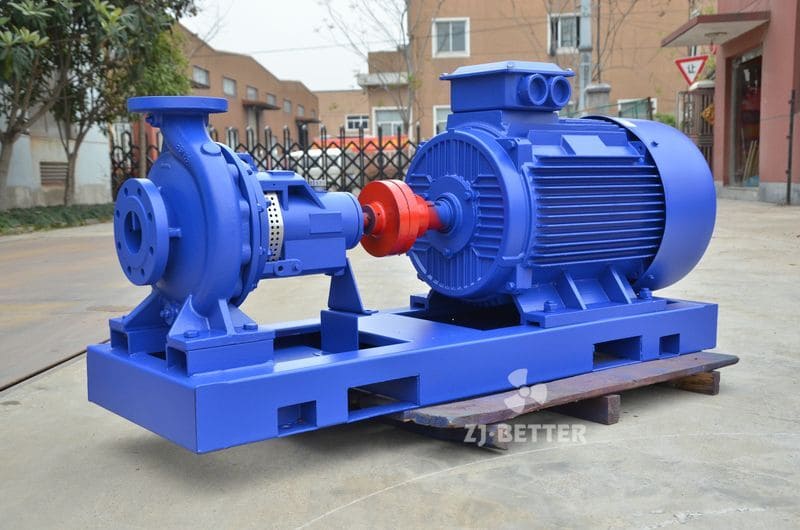
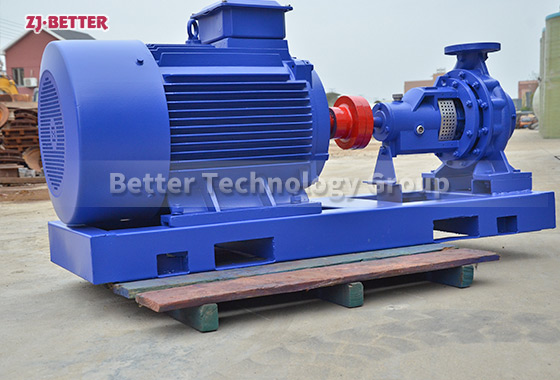
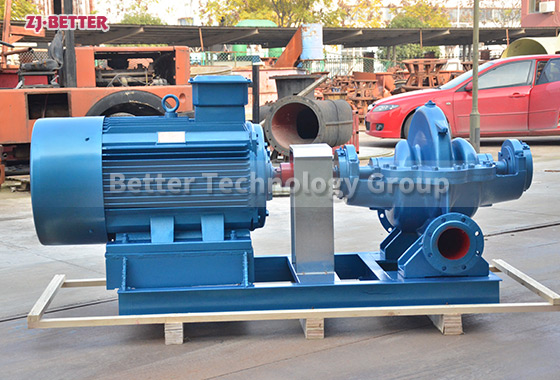
XA80/32 and XA100/32 bare shaft pump for shipment
Self-priming pump is a kind of self-priming centrifugal pump, which has the advantages of convenient operation, stable operation, easy maintenance, compact structure, long service life, high efficiency and strong self-priming ability. It does not need to install a bottom valve in the pipeline, as long as there is a quantitative suction liquid stored in the pump body before working, and different liquids can use self-priming pumps of different materials.
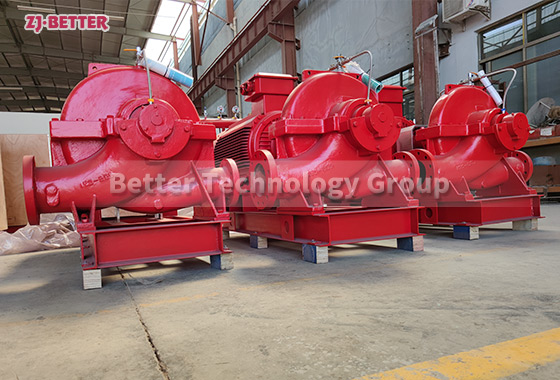
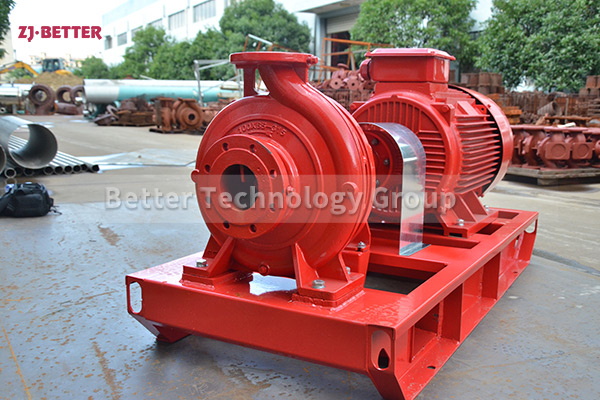
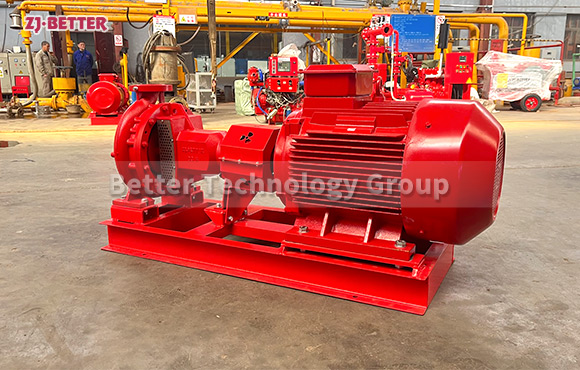
Horizontal fire pumps have significant advantages such as high efficiency, low operating noise, good anti-cavitation performance, reasonable structure, and long service life. , Long-distance water delivery, heating, bathroom, boiler cold and warm water cycle pressurization, air conditioning and refrigeration system water delivery and equipment matching and other occasions.
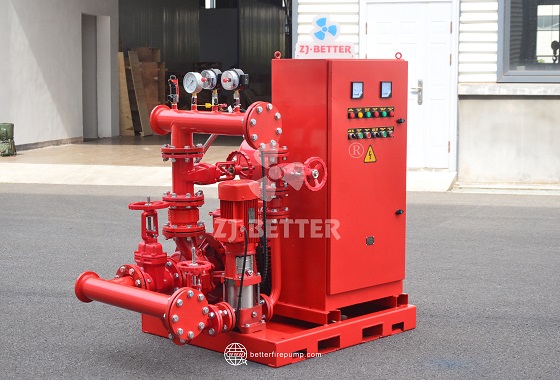
The fire pump is mainly a kind of pump equipment used for fire emergency, and its function is to transport the water source to the fire scene for fire extinguishing. In life, fire pumps are widely used in various buildings, such as factories, docks, warehouses, ports and other places, and are important equipment for fire emergency.
Flow:250-10000 GPM Head:3-16 Bar In various fields, our products find applications in large hotels, hospitals, schools, office buildings, supermarkets, commercial residences, subway stations, train stations, airports, various transportation tunnels, petrochemical plants, thermal power plants, oil storage tanks, large warehouses, industrial and mining enterprises, seawater injection, etc.
The Horizontal Multistage Pump is an exceptional engineering solution that offers high performance and reliability for fluid handling applications. With its unique multistage impeller design, it delivers efficient and incremental pressure boosting for high-pressure and high-flow scenarios. Whether used in water supply systems, industrial processes, irrigation, or building cooling, this pump ensures stable water pressure and flow. Its compact design allows for easy installation and maintenance, while its superior construction materials guarantee durability and long-term reliable operation. Choose the Horizontal Multistage Pump to achieve exceptional performance and success in your fluid handling projects.
If an electric fire pump fails during an emergency, the following steps should be taken:
Activate the backup pump: If available, switch to a secondary pump or manual firefighting methods. Investigate the cause of failure: After the emergency, perform a thorough inspection to determine the cause of the failure. Repair or replace the pump: Address the identified issues and restore the pump to full operational status. Review maintenance practices: Ensure regular testing and maintenance procedures are followed to prevent future failures.
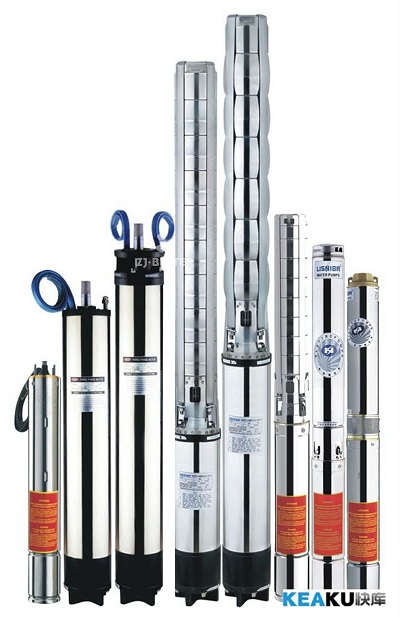
Submersible pump is an important equipment for deep well water extraction. During use, the whole unit works in the water to extract groundwater to the surface, which is used for domestic water, mine rescue, industrial cooling, farmland irrigation, sea water lifting, ship load regulation, and fountain landscape.
The XBD-L Vertical Single stage single suction fire pump is specifically designed for fixed fire protection systems in a wide range of settings, including businesses, construction projects, and high-rise buildings. It is a vital component in fire hydrant extinguishing systems, automatic sprinkler fire suppression systems, and more. This pump set is capable of delivering clear water and water-like media with physical and chemical properties similar to water, without solid particles, at temperatures below 100°C. It is also suitable for fire protection, domestic water supply, shared water supply systems, as well as building and municipal water supply and drainage applications.
·UL Standard Flow:100-2500 GPM Head:90-250 PSI ·NON-UL Standard Flow:250-10000 GPM Head:30-200 m / 3-20 Bar / 40-290 psi
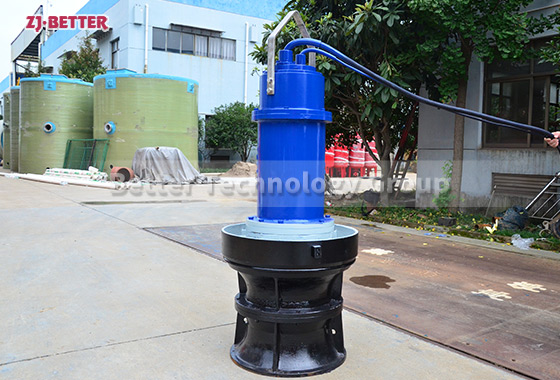
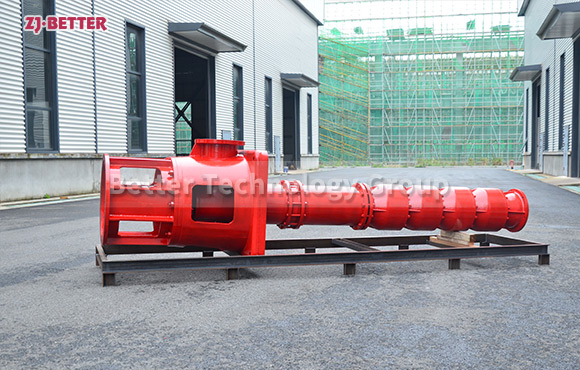
The submersible axial-flow pump is a special type of submersible pump designed for handling large flow rates with relatively low head conditions. It has a wide range of applications, including agricultural irrigation, urban water supply and drainage, municipal flood control and emergency rescue, as well as various water conservancy projects.The main feature of the submersible axial flow pump lies in its innovative design, enabling efficient operation under high flow rate conditions. Compared to conventional submersible pumps, it operates at relatively lower head conditions, making it more suitable for transporting water over long distances with moderate elevation changes.
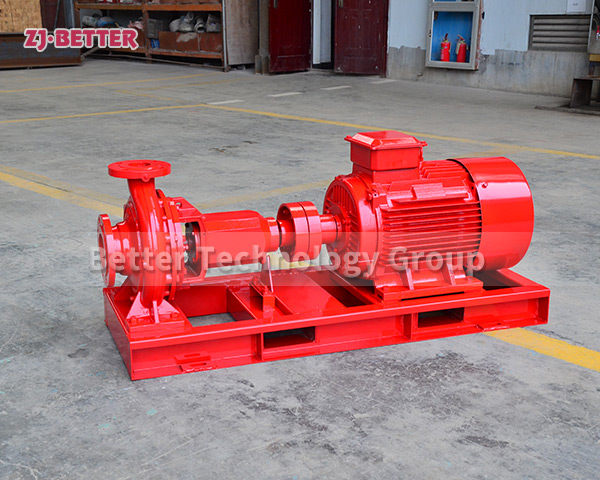
XA series single-stage centrifugal pump is the earliest single-stage single-suction centrifugal pump product launched by Better (China) Technology Co., Ltd. This product combines the advantages of similar products in China and abroad, and is designed with excellent hydraulic model. Therefore, its excellent hydraulic performance and structural characteristics ensure that users can effectively reduce the operation cost of pumps in various applications.
Electric fire pump systems include several safety features, such as:
Pressure relief valves: Prevent over-pressurization of the system. Jockey pumps: Maintain system pressure and reduce the frequency of the main pump’s operation. Emergency stop buttons: Allow manual shutdown of the pump in case of an emergency. Automatic transfer switches: Ensure seamless switching to backup power sources during a power outage.
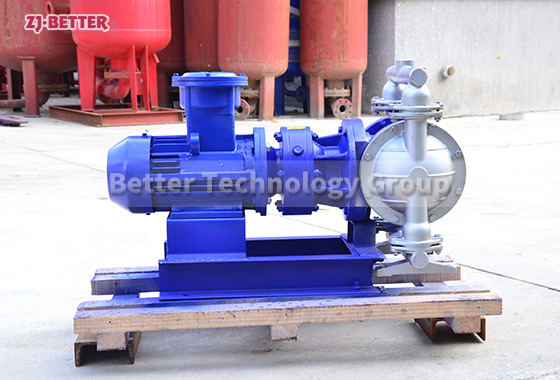
The electric diaphragm pump is a reliable and efficient industrial pump powered by an electric motor. It uses diaphragms to move liquids, making it suitable for handling various fluids, including clear water, chemicals, corrosive liquids, viscous substances, and particle suspensions. With its compact size and lightweight design, the pump is easy to install and maintain. It finds extensive use in industries such as chemical, petroleum, food and beverage, paper-making, and environmental protection. The pump’s leak-free and eco-friendly operation ensures safe and sustainable fluid handling processes. Its versatility, efficiency, and reliability make it an ideal choice for fluid transportation in various industrial applications.
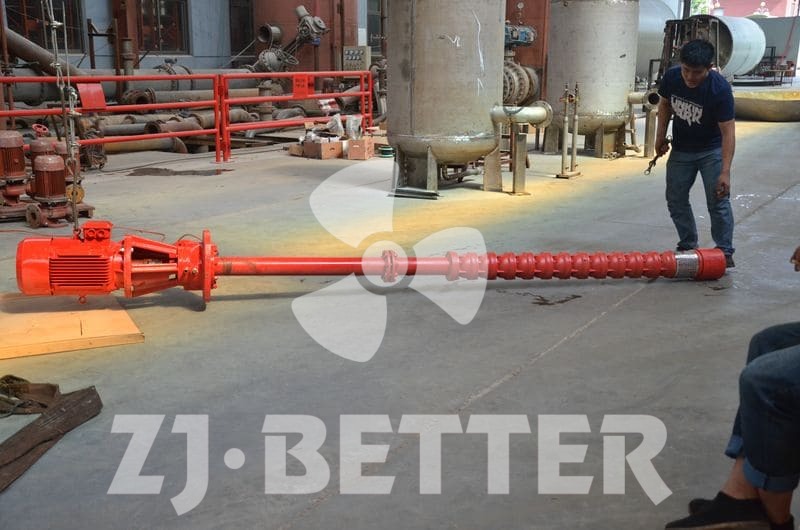
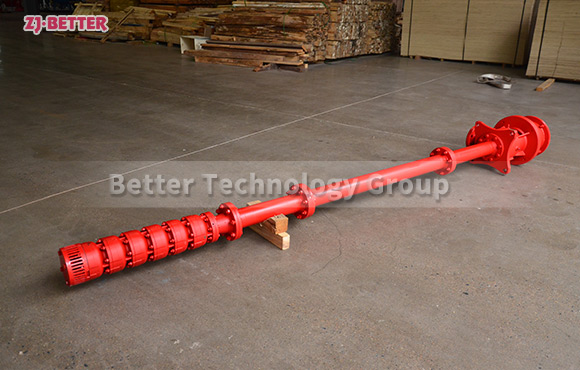
Long shaft pump is suitable for conveying belt particles, high viscosity, strong acid, alkali, salt, strong oxidant and other corrosive media. The motor part is placed on the liquid level, the pump part is placed under the liquid level, with strong corrosion resistance, no blockage, high temperature resistance and other characteristics. A new type of
Horizontal fire pumps are designed according to the principle of centrifugal force. The high-speed rotating impeller blades drive the water to rotate and throw it out, so as to achieve the purpose of transportation. There are many kinds of centrifugal pumps, which can be divided into civil pumps and industrial pumps in use; from the perspective of conveying media, they can be divided into clean water pumps, impurity pumps, corrosion-resistant pumps, etc.
The electric constant pressure fire pump system features rapid high-pressure startup, intelligent pressure control, energy-saving operation, and fault detection. Ideal for high-rise buildings, hospitals, subways, and data centers, it ensures smart firefighting and efficient water supply.
ISO end-suction pumps offer high efficiency, high flow capacities, and the ability to withstand high pressures. The suction inlet is designed to efficiently intake fluids, while the pump itself is constructed to be compact, making it suitable for installation and maintenance in limited spaces.They also provide multiple material options to accommodate different fluid mediums, including corrosive and high-temperature substances. ISO end-suction pumps find wide application in industries such as chemical, petroleum, pharmaceutical, food and beverage, and water treatment, where they are used for fluid transportation, circulation systems, heating, and cooling systems, among others.
Flow:50-7500 GPM Head:3-20 Bar 40-300 psi Power:11-1000 kw Caliber:50-200 mm Frequency:50 or 60 Hz
Selection criteria include:
Required flow rate and pressure. Depth and characteristics of the water source. Type of installation (indoor or outdoor). Compliance with relevant standards and regulations. Environmental conditions and potential hazards.
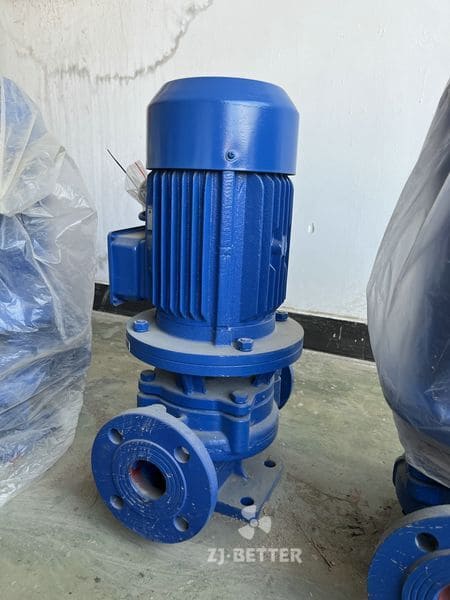
The vertical pipeline centrifugal pump is a pipeline centrifugal pump with a vertical structure. There are many models of the pump. The most common one is the ISG pipeline centrifugal pump. Urban water supply and drainage, high-rise buildings pressurized water supply.
The Vertical Single stage fire pump is specifically designed for fixed fire protection systems in a wide range of settings, including businesses, construction projects, and high-rise buildings. It is a vital component in fire hydrant extinguishing systems, automatic sprinkler fire suppression systems, and more.
The XA single-stage centrifugal pump is a widely used industrial pump designed for fluid transportation and handling in various industries. It features a simple and compact design with a rotating impeller and a stationary pump casing. The pump offers high efficiency, reliability, and flexibility in installation. It finds applications in water treatment, agriculture, construction, petrochemicals, energy, pharmaceuticals, and food processing. The XA pump is capable of handling different fluid mediums and provides efficient flow control. Its operating principle utilizes centrifugal force to draw in and propel fluids through the pump. Overall, the XA single-stage centrifugal pump is a reliable and efficient solution for fluid pumping needs in industrial settings.
Pump type is vertical multistage centrifugal pump, with the use of health clean, high efficiency, low noise, resistance to mildly corrosive and compact structure, beautiful appearance, small size, light weight. The use of easy maintenance, and reliable sealing performance. Use for high-rise building pipeline booster, fire booster regulator system.
Electric vertical turbine pump with high efficiency, energy saving and high efficiency, pump impeller immersed in water, no bottom valve, no irrigation and shaft vacuum, can be directly started, very convenient and reliable.
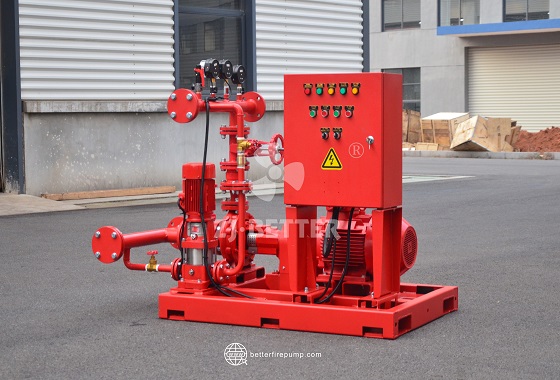
The electric fire pump is engineered for commercial buildings, offering high efficiency, low energy consumption, intelligent control, and modular installation—an ideal fire protection solution for modern architecture.
Sewage pump is a kind of non-clogging pump, with various forms: such as submersible and dry type, dry type sewage pump with cam rotor, mainly used to transport urban sewage, feces or liquid containing fibers, paper scraps For mediums such as solid particles, the temperature of the medium to be conveyed is usually not greater than 80 ¡ãC. Because the conveyed medium contains fibers that are easily entangled or bunched. Therefore, the flow channel of this kind of pump is easy to be blocked. Once the pump is blocked, the pump will not work normally, and even the motor will be burned, resulting in poor sewage discharge. It has a serious impact on urban life and environmental protection. Therefore, blocking resistance and reliability are important factors for the quality of sewage sewage pump.
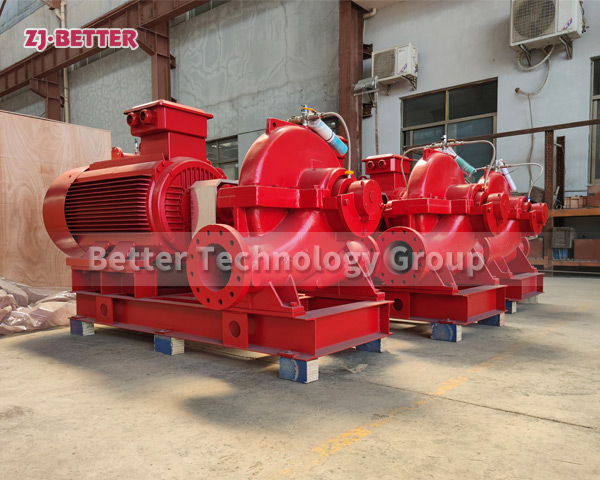
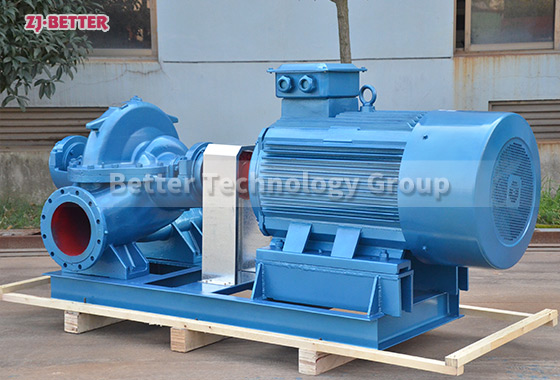
The OTS Double-suction End-suction Pump is a pump that combines the characteristics of a double-suction pump and an end-suction pump. It is designed for high flow and medium head liquid transfer and circulation systems in industrial applications. This pump features double-suction characteristics and an end-suction structure, making it suitable for balancing liquid flow and ensuring stability and efficiency. The end-suction design allows for easy installation and maintenance, particularly in spaces with limitations. The OTS Double-suction End-suction Pump offers high efficiency and is widely applicable in various applications, including water supply systems, cooling water circulation, petrochemicals, and industrial processes. When selecting and using this pump, specific operational requirements and flow rates should be considered, and consultation with professional engineers or pump suppliers is recommended to ensure the appropriate equipment is chosen for safe and reliable operation.
With proper maintenance and regular testing, an electric fire pump can have a lifespan of 20-30 years or more. Regular inspections and timely repairs are key to ensuring its longevity and reliability.