Home » Diesel engine fire pump » The XBC-ZWC Diesel Engine Self-priming Pump: your trusted companion.

The XBC-ZWC Diesel Engine Self-priming Pump: your trusted companion.

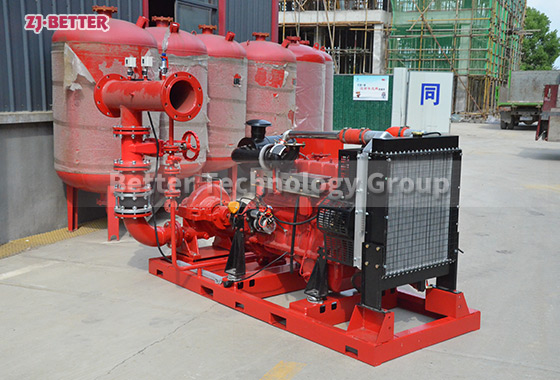
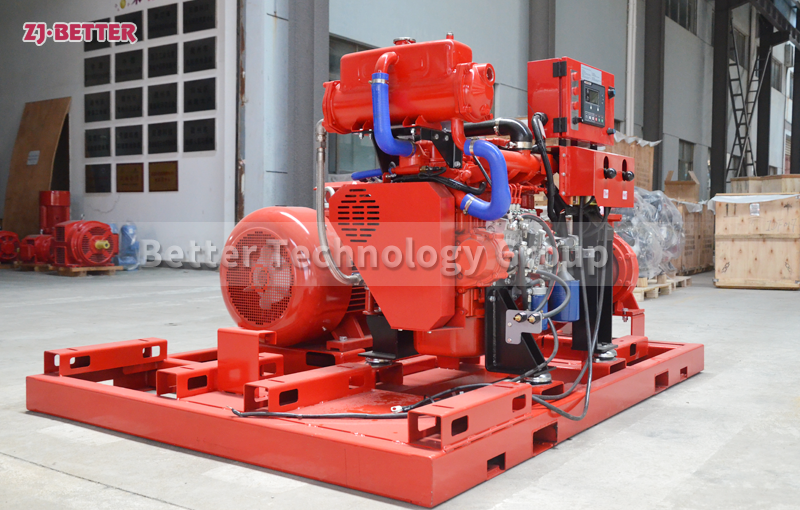
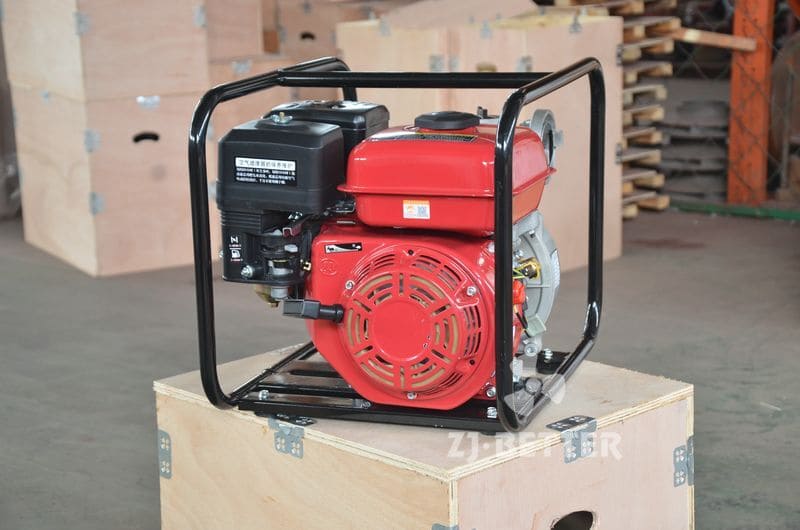
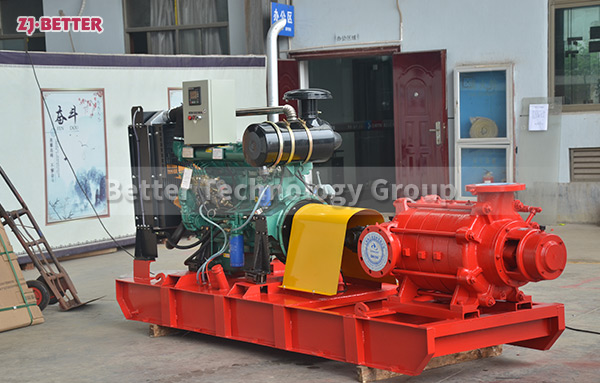
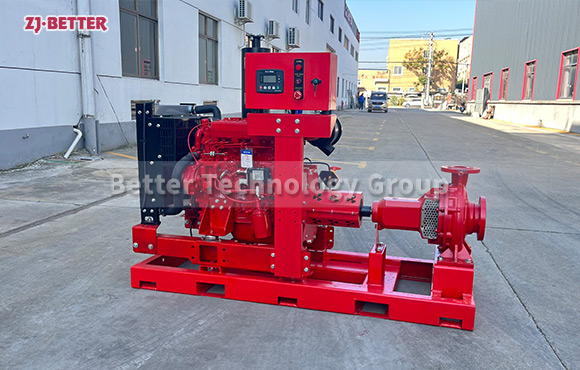
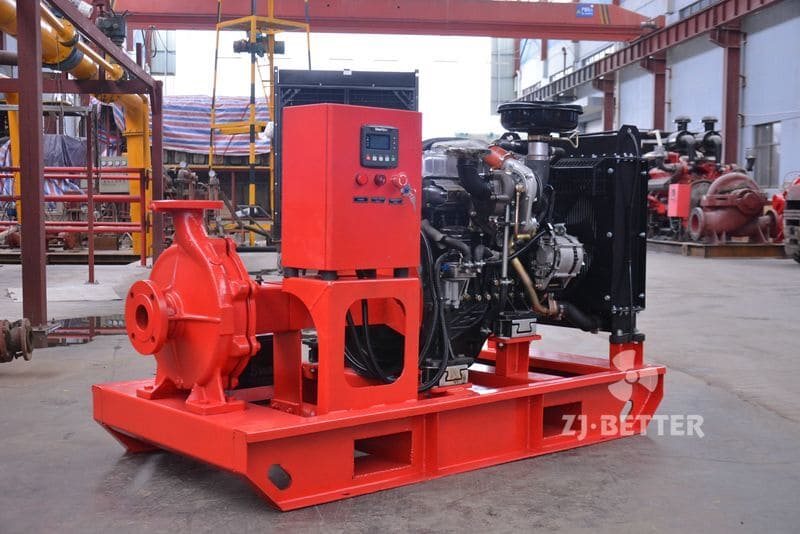
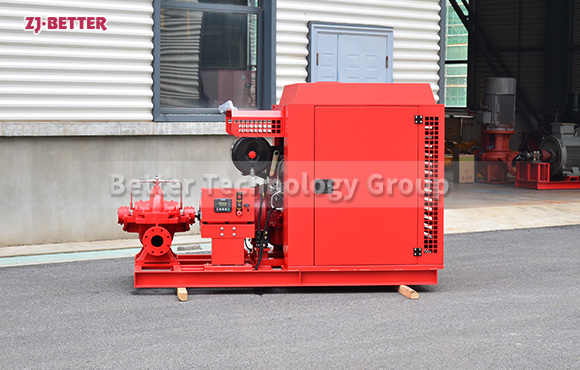
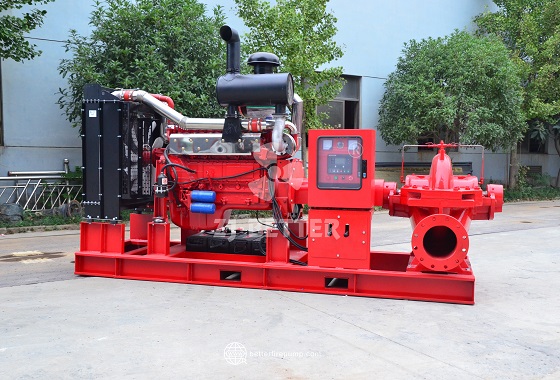
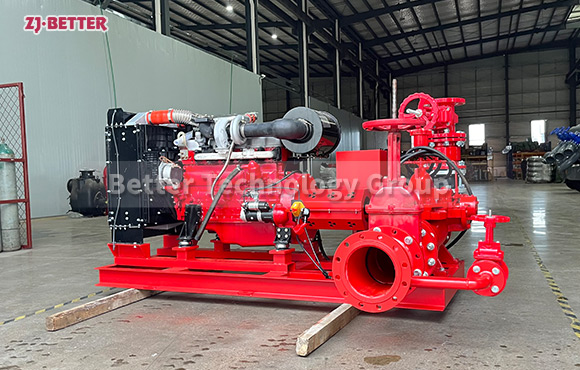
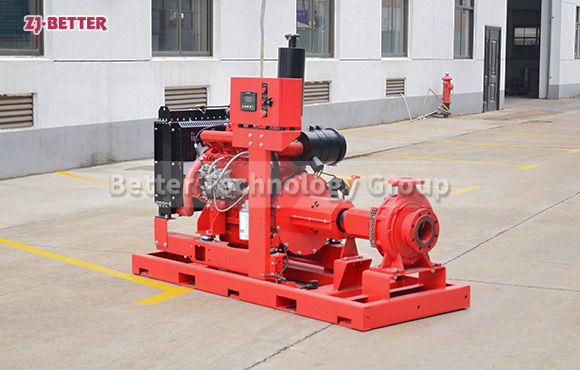
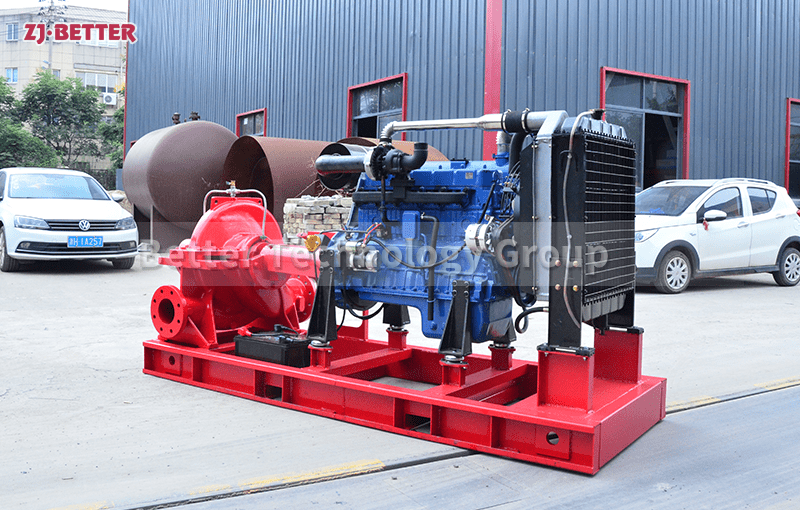
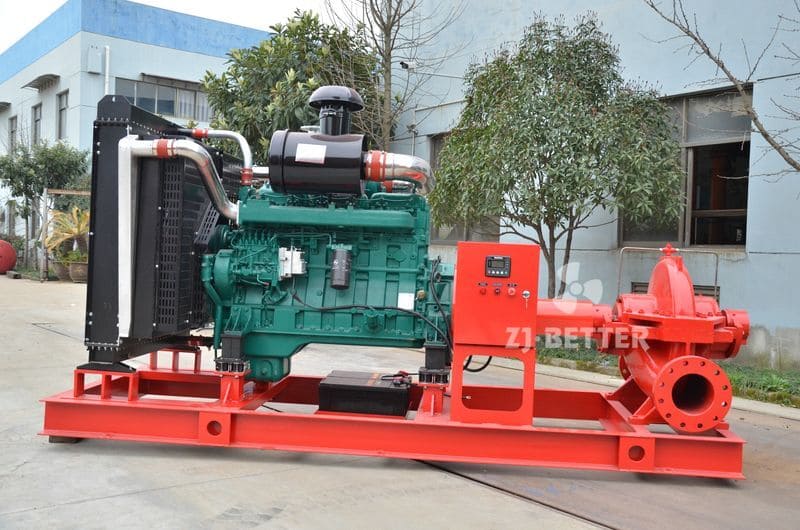
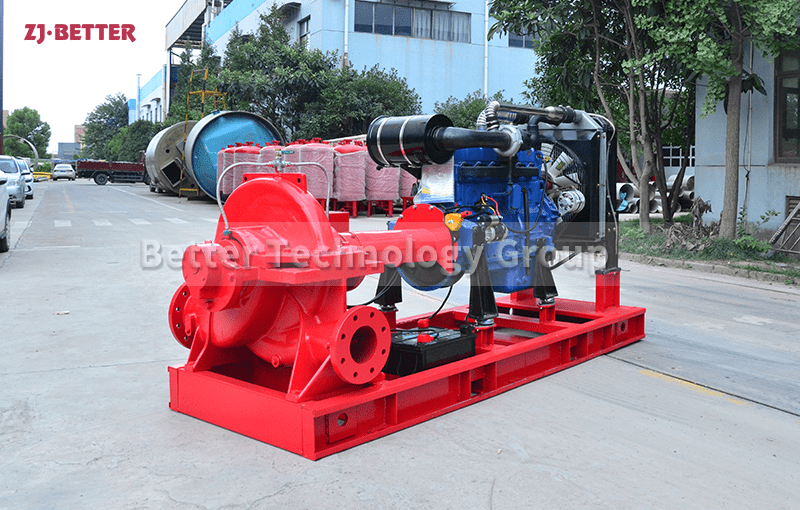
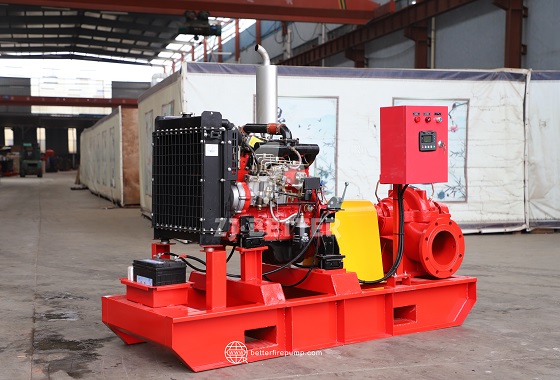
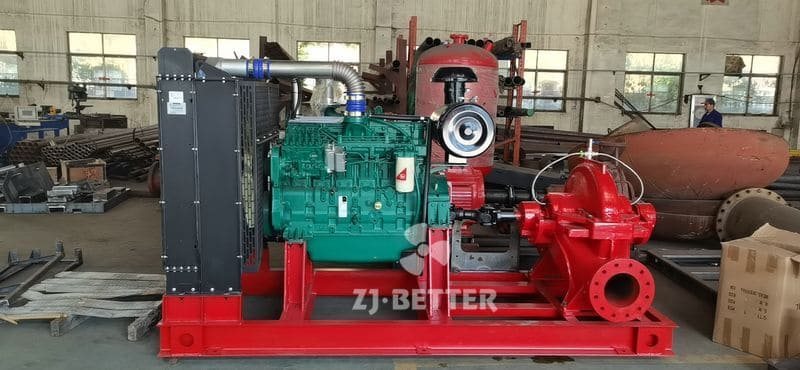
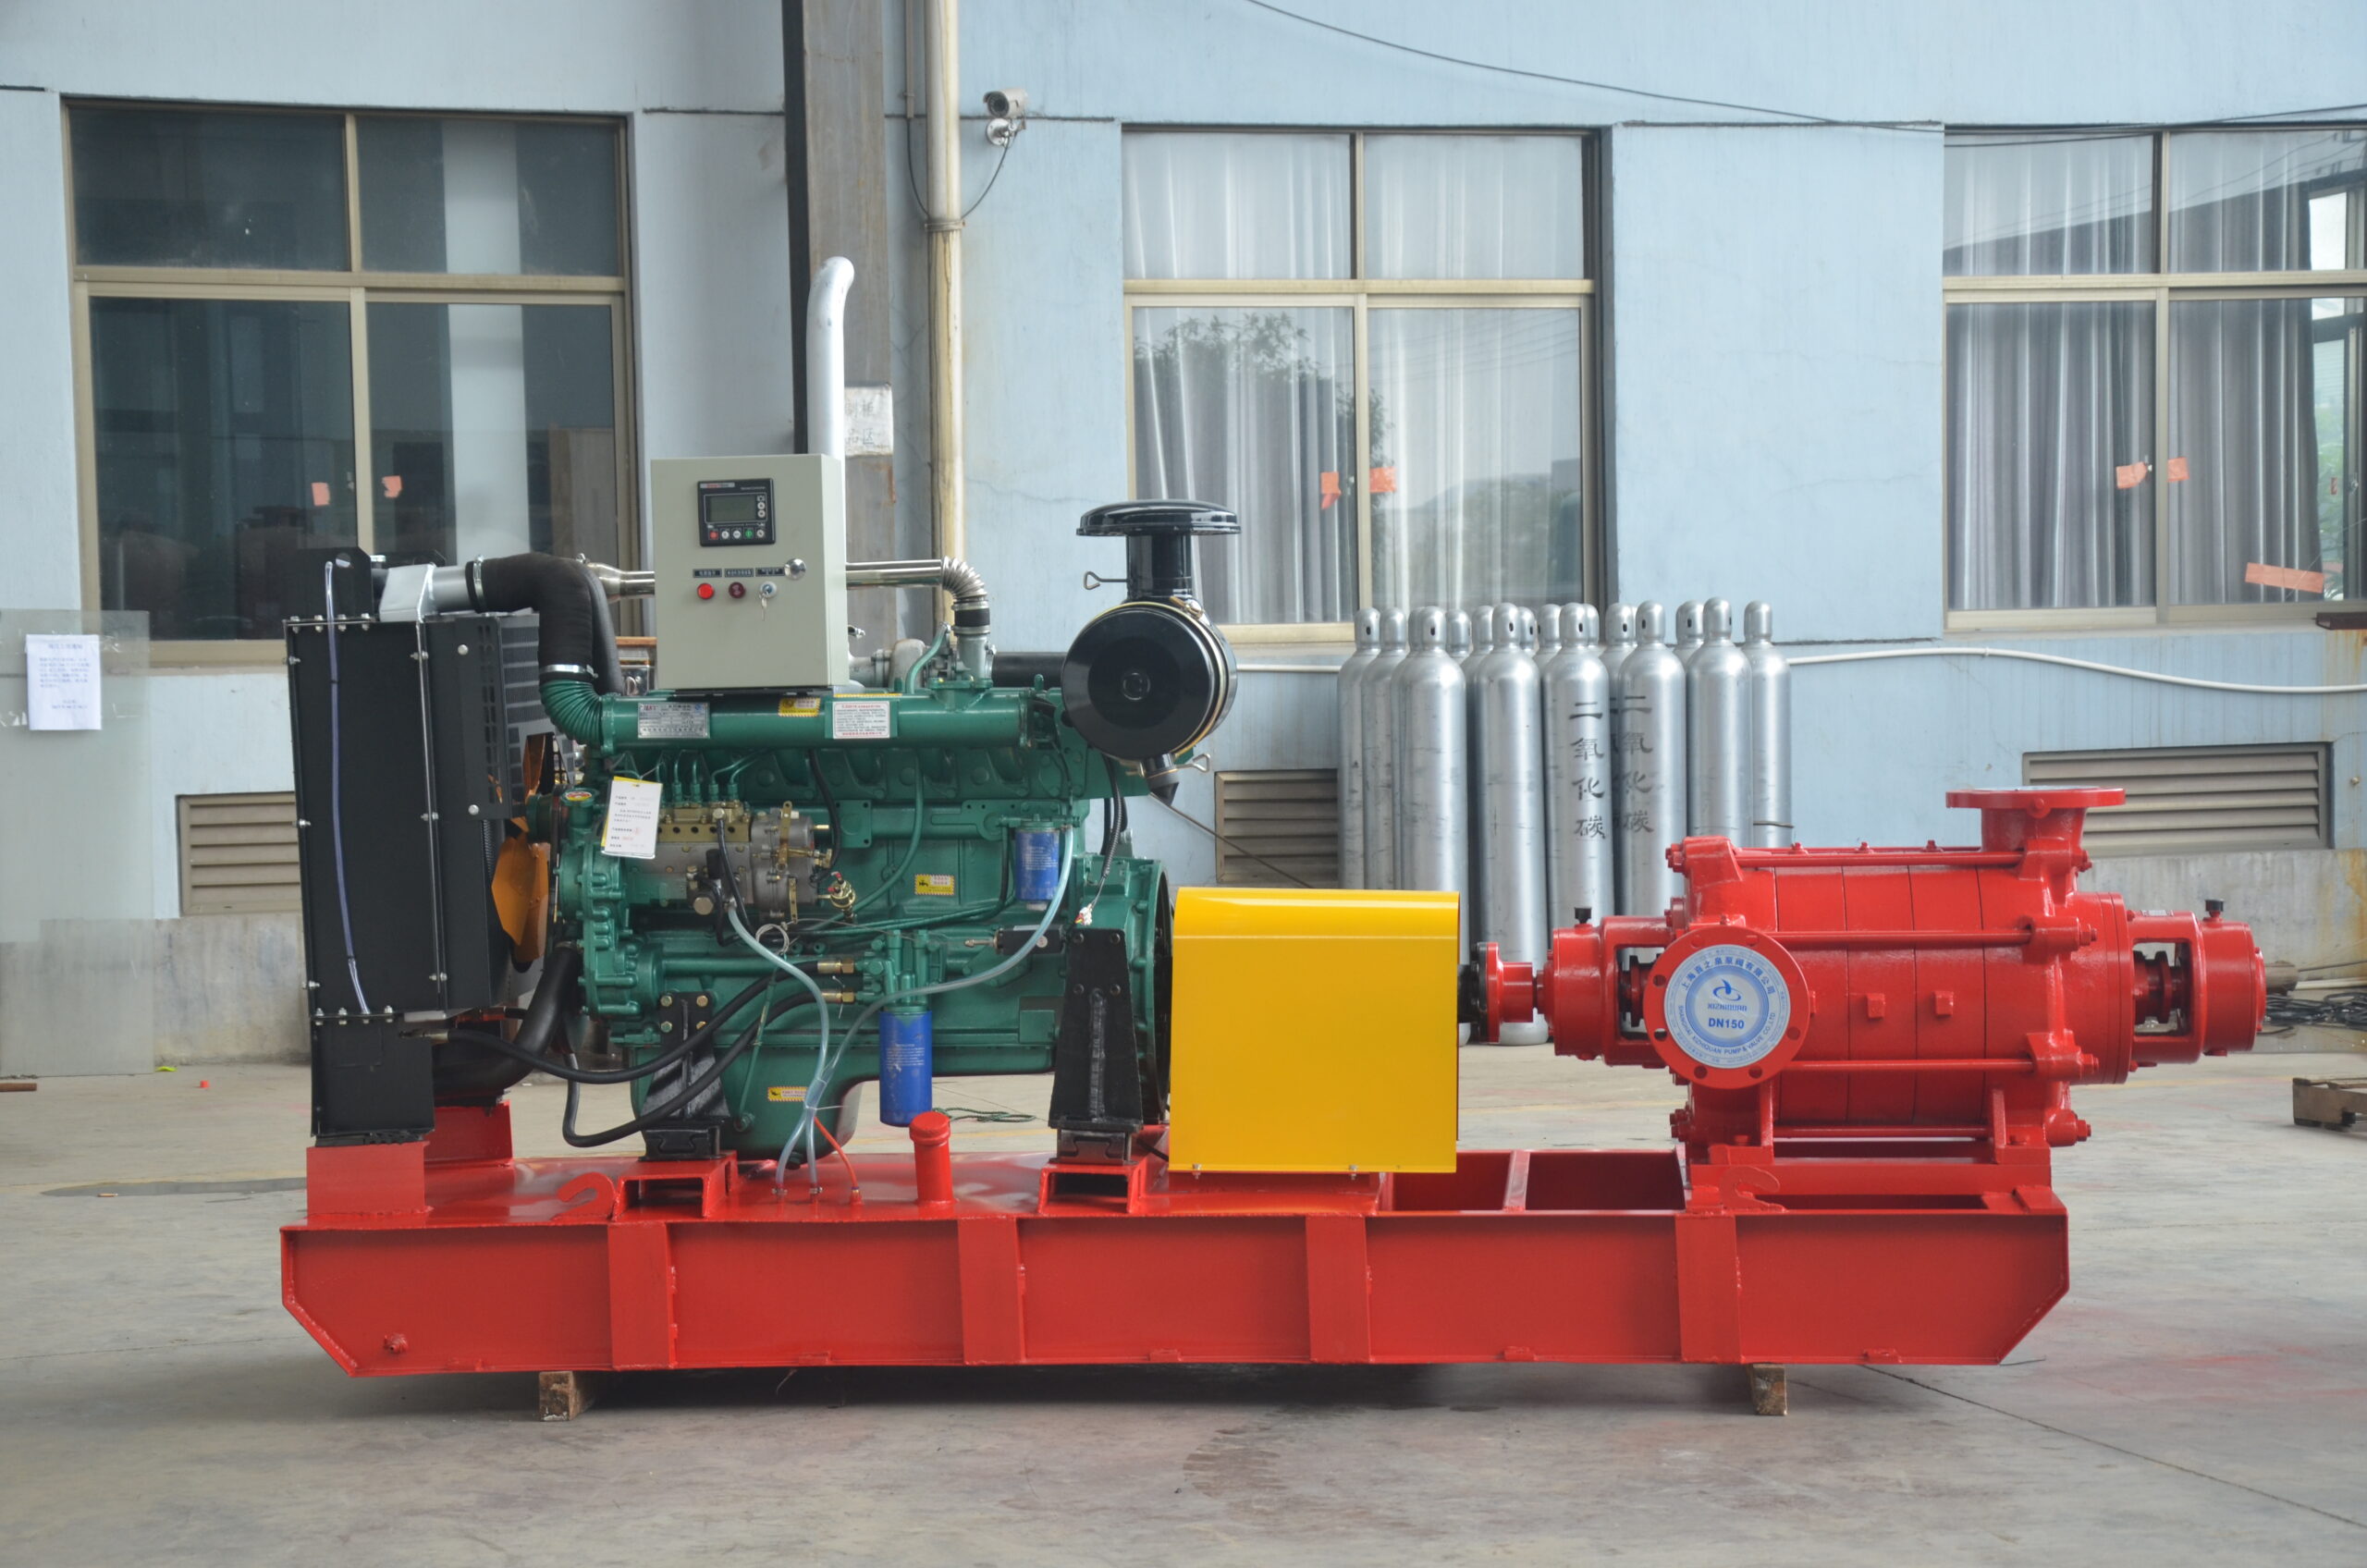
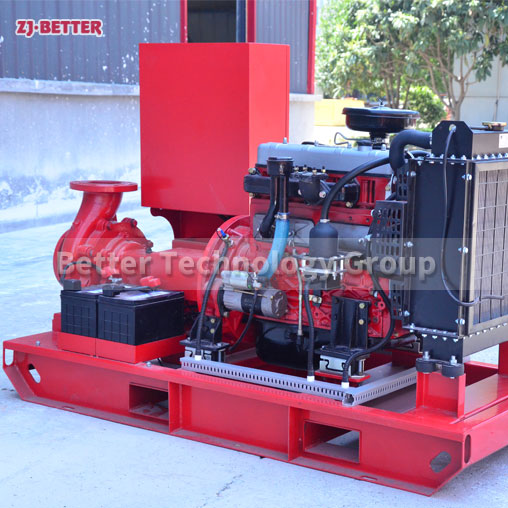
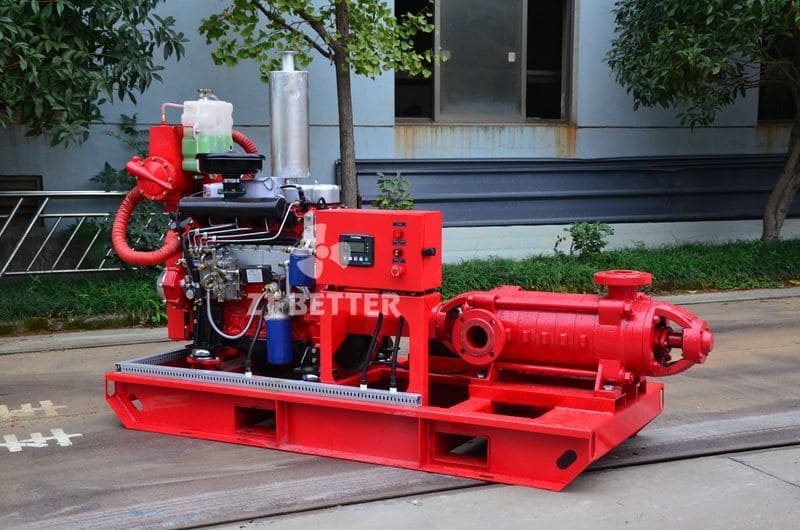
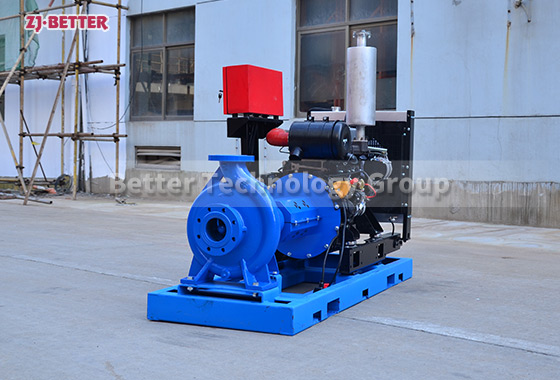
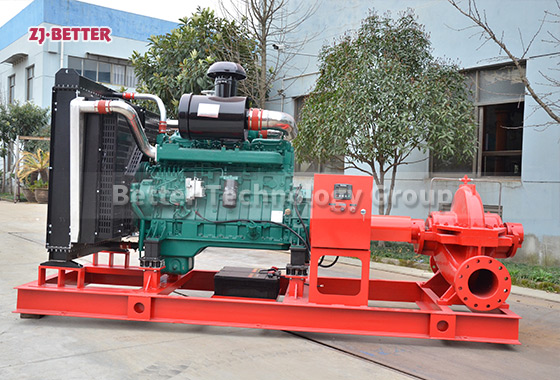
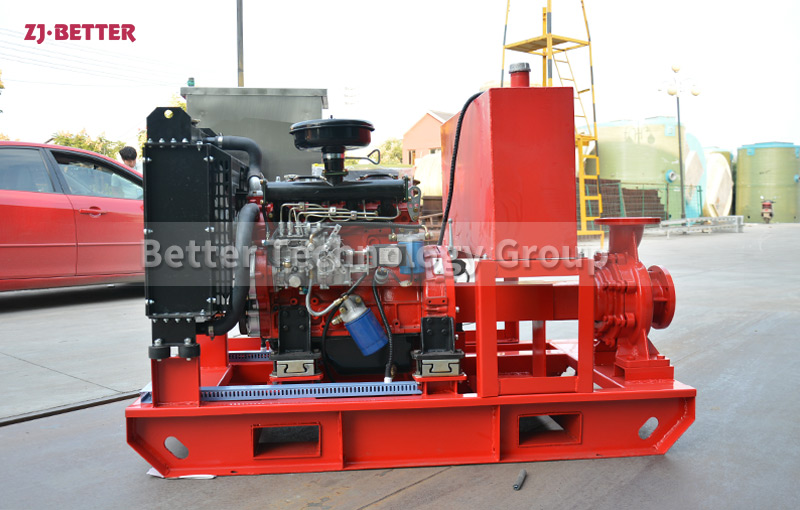
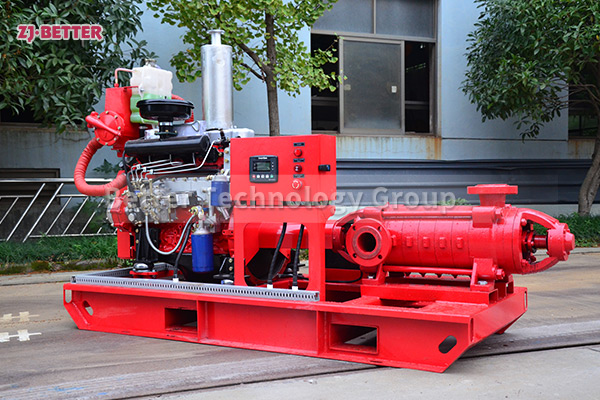
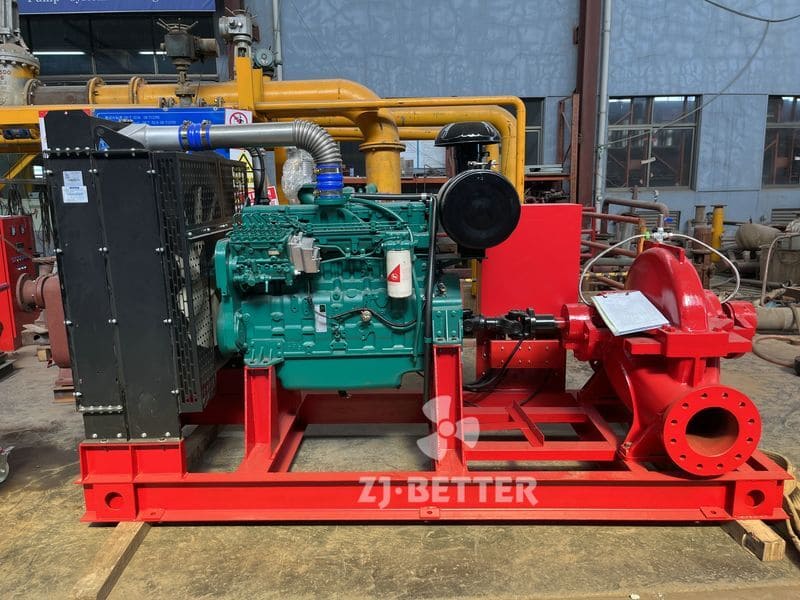
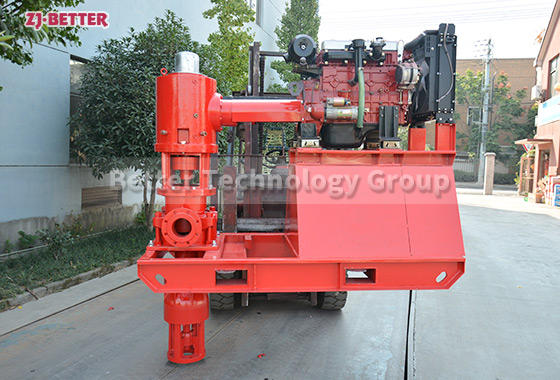
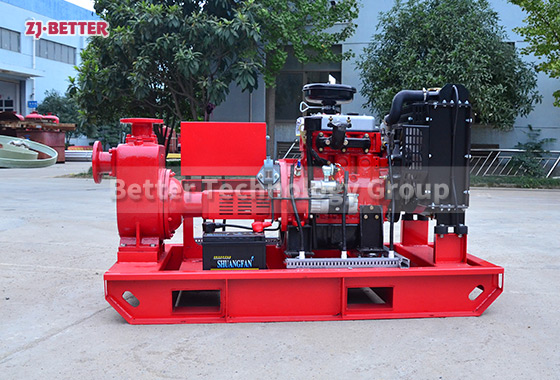
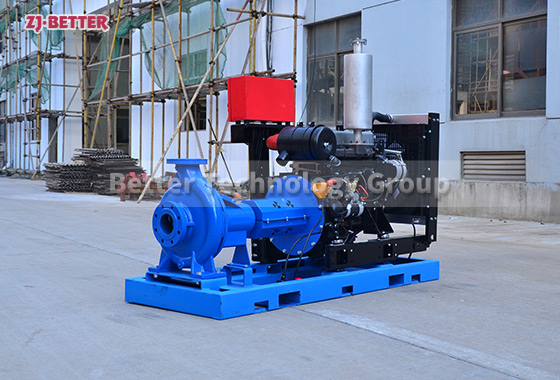
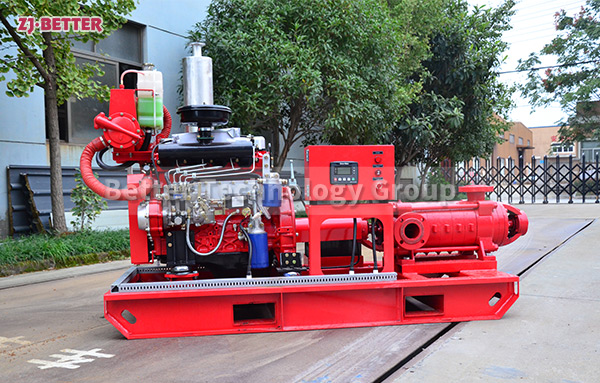
The XBC-ZWC Diesel Engine Self-priming Pump is a powerful and versatile solution for various water transfer applications. Designed with reliability and efficiency in mind, this self-priming pump is specifically engineered to handle water transfer tasks with ease. Whether you need to move water from one location to another, drain flooded areas, or supply water for irrigation, the XBC-ZWC Diesel Engine Self-priming Pump is your trusted companion.

Rated 4.6/5 based on 340 customer reviews
Share:
Content

Key Features:

1.Self-Priming Capability: With its advanced self-priming design, the XBC-ZWC Diesel Pump can quickly and effectively remove air from the suction pipe, allowing for effortless priming and ensuring a continuous flow of water.

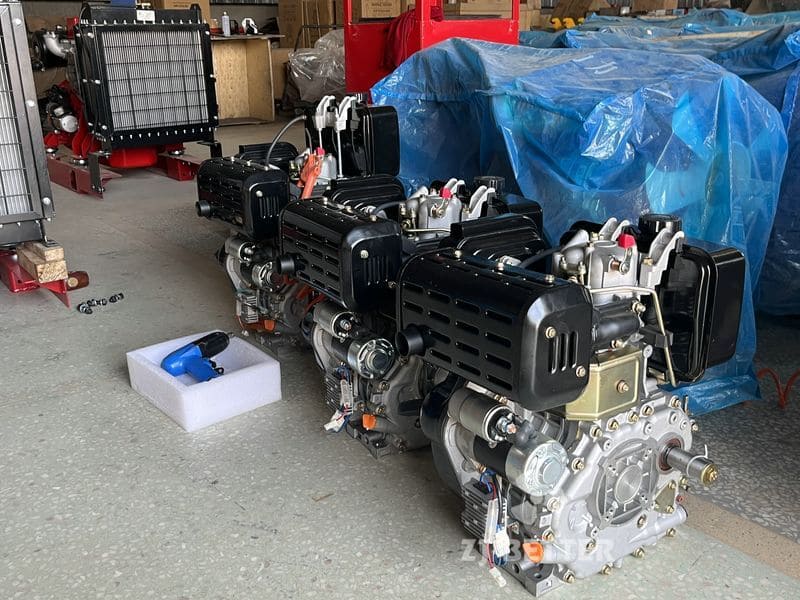
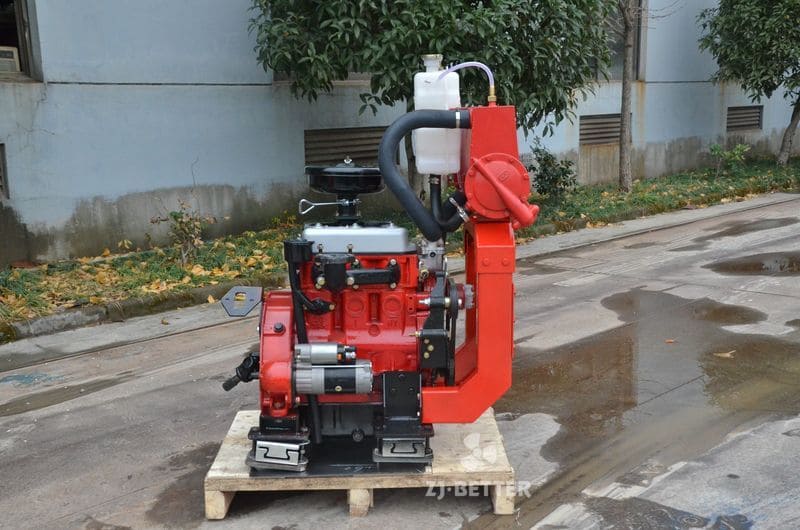
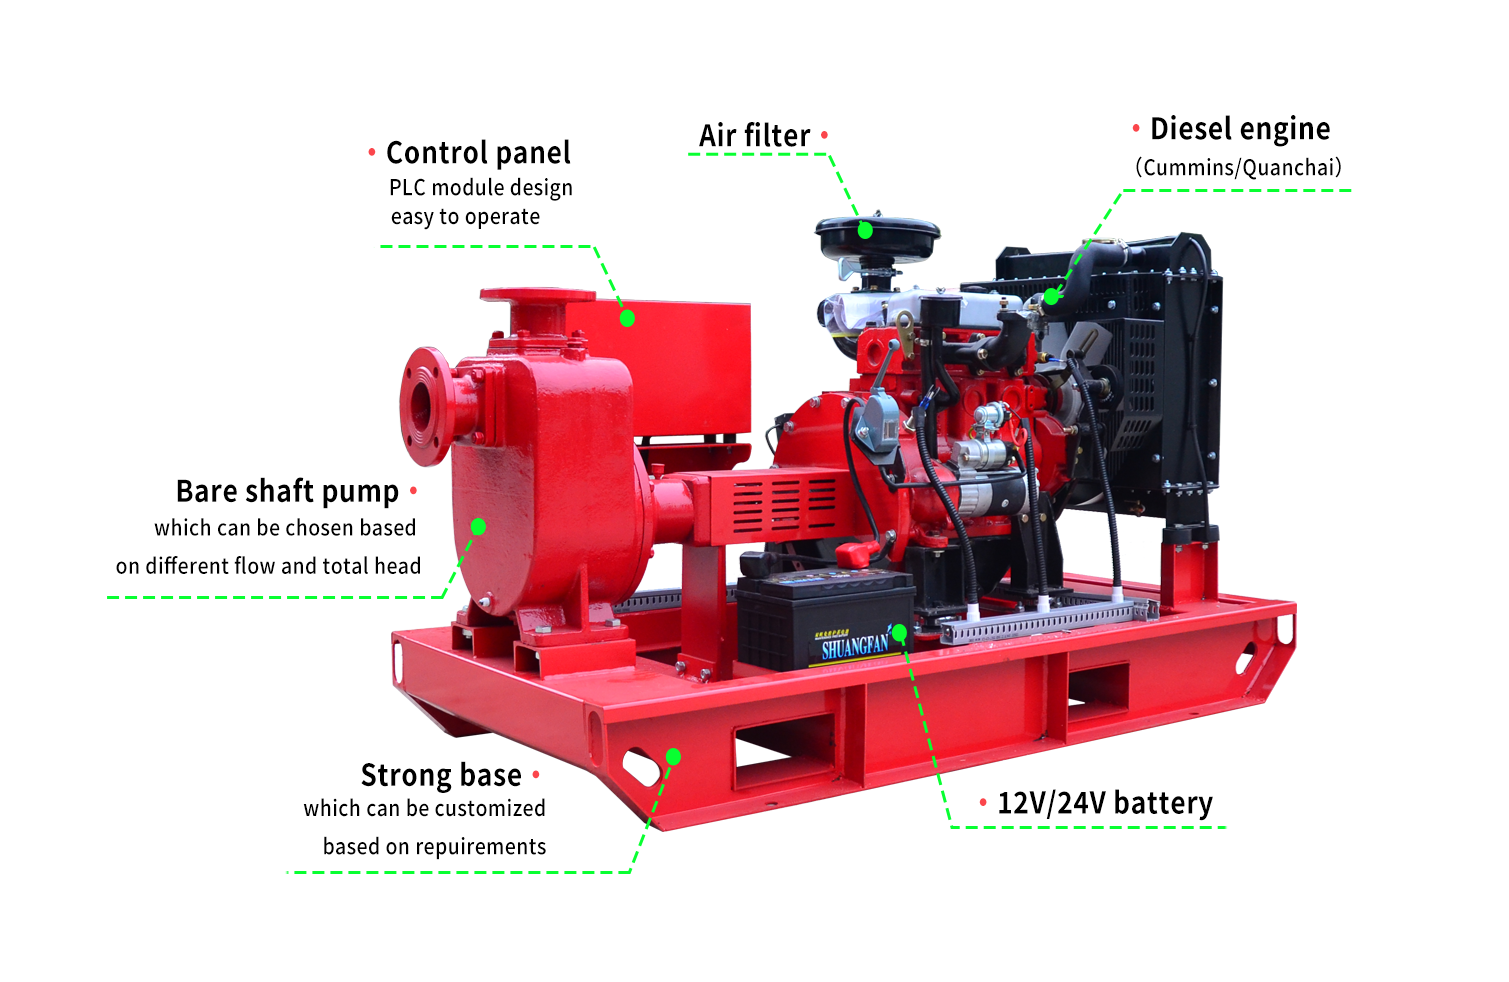
2.Efficient Diesel Engine: Powered by a high-performance diesel engine, this pump delivers reliable and efficient operation. The diesel engine provides a stable power source, allowing the pump to operate in various environments and challenging conditions.

4.Robust Construction: Built to withstand tough working conditions, the XBC-ZWC Diesel Self-priming Pump features a rugged construction that ensures durability and longevity. It can handle abrasive and corrosive materials, making it suitable for a wide range of applications.

4.Easy to Operate: Equipped with user-friendly controls and a simple interface, this pump is easy to operate even for those with minimal technical expertise. Its intuitive design allows for quick setup and hassle-free operation, saving you time and effort.5.

5.Versatile Applications: The XBC-ZWC Diesel Self-priming Pump is suitable for a variety of applications, including agricultural irrigation, construction sites, dewatering flooded areas, water transfer for firefighting operations, and more. It provides a reliable and efficient solution for your water transfer needs.
Inquiry


    More Diesel engine fire pump

    Generally speaking, we recommend that where natural ventilation is used to install diesel engine fire pumps, there must be vents and exhaust ports of sufficient size, and the position of the vents ensures that there is enough fresh air to supply the diesel engine for combustion within the temperature limit. Of course, the water supply radiator can also be used to take away the heat of the circulating cooling water and the heat emitted from the surface of the unit. If the space cannot meet the requirements of natural ventilation and cannot effectively dissipate heat, it is recommended that you adopt forced ventilation, install an intake fan and an exhaust fan at the vent, and choose a location that can provide enough cold air for the diesel engine and take away the machine room hot air inside. Generally speaking, the air intake of the unit should be 6-7 times that of the diesel engine. Only in this way can normal ventilation be ensured and the operating efficiency of the equipment can be improved.

    In addition, it must be fixed firmly so that the entire unit can be supported to ensure that the unit is in a horizontal state and absorb vibration. Generally speaking, the foundation of the unit adopts a concrete structure. The length and width are 150-250mm on one side of the length and width of the unit chassis, and the depth is 300-600mm. The height of the anchor bolts should be about twice the bolt diameter. And there should be a 750mm channel on both sides and front of the unit to facilitate the operator’s inspection and general maintenance.

    Our fire pump is renowned for its outstanding performance and reliability, specifically designed to respond to fire emergencies efficiently. It can start quickly in critical situations, ensuring a stable and efficient water supply. Whether in commercial buildings, industrial facilities, or public places, our fire pump delivers powerful performance and high head, swiftly transporting water to designated areas to ensure efficient firefighting operations.

    The product features advanced hydraulic design and an energy-efficient motor, which not only ensures smooth operation but also effectively reduces energy consumption and operating costs. Its low-noise characteristic makes it particularly suitable for environments with strict noise control requirements, maintaining quiet and reliable operation even during 24/7 use. High-quality materials and meticulous manufacturing processes provide excellent durability, enabling the pump to work stably for long periods in high-temperature, high-pressure, and corrosive environments.

    Equipped with an intelligent control system, the fire pump offers real-time monitoring, remote control, and fault alarm functions. Through a high-definition display, operators can easily monitor the operational status and quickly access parameters such as flow rate, pressure, and temperature. The built-in alarm system promptly issues warnings in case of abnormal operation, minimizing safety risks. The user-friendly maintenance design makes routine servicing simpler, prolonging the pump’s lifespan.

    We are committed to providing customers with reliable fire pump solutions, combining superior performance with user-friendly design to ensure comprehensive fire safety. Whether for new construction projects or equipment upgrades, our products are always your top choice.