High-Flow Diesel Fire Pump Set – Large Fire Pump and Diesel Engine Combination for Engineering Water Supply Systems
High-capacity diesel fire pump units consist of a diesel engine paired with a large-scale fire pump. They offer a variety of pump types and engineering specifications, making them suitable for fire-suppression water supply systems in industrial facilities, warehouses, docks, airports, and other large-scale infrastructure.
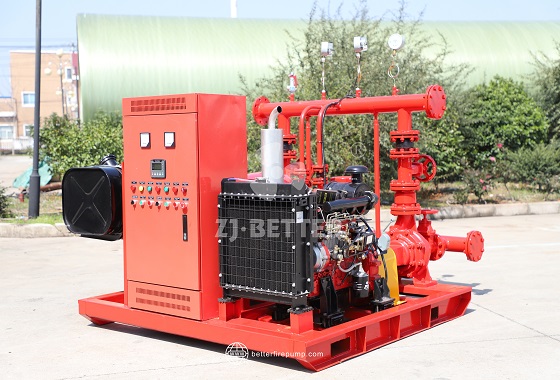
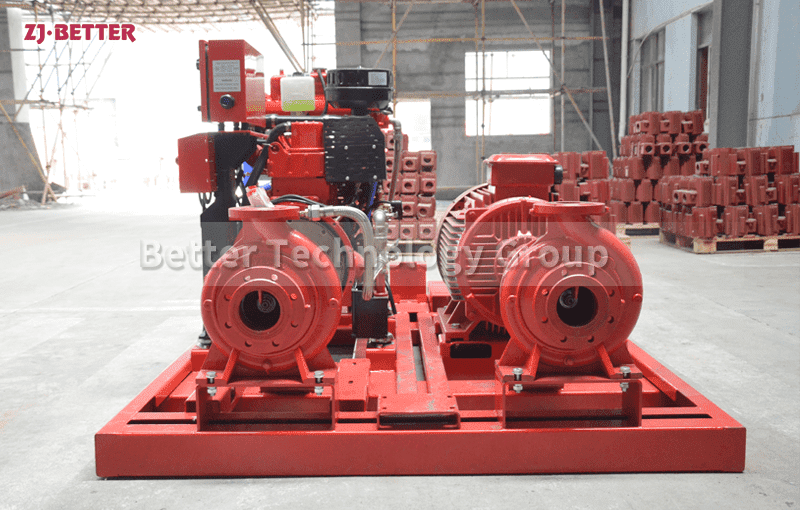
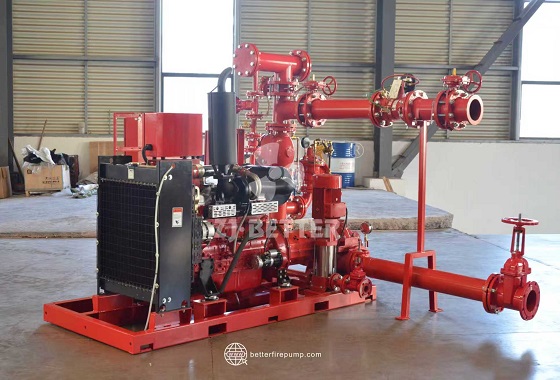
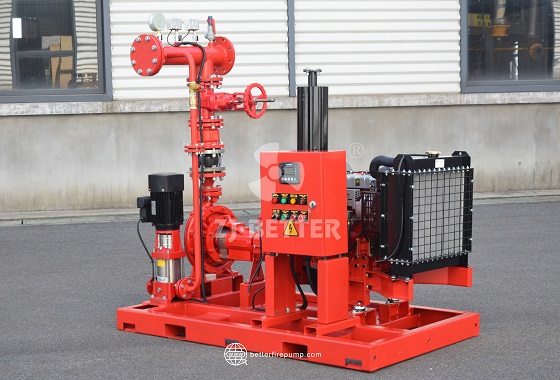
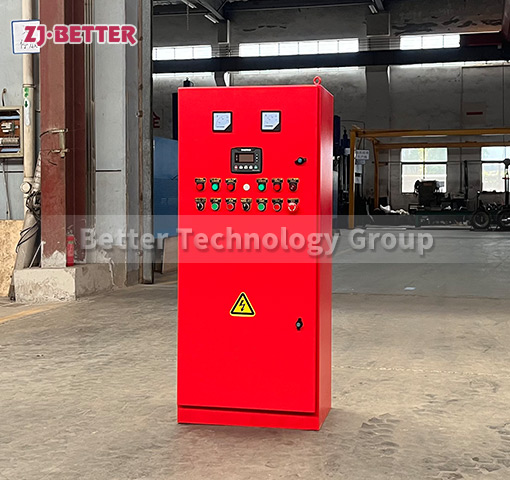
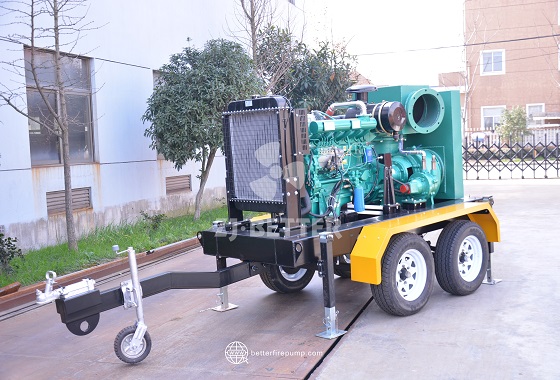
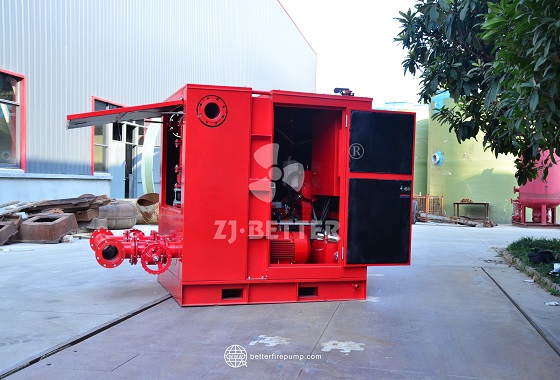
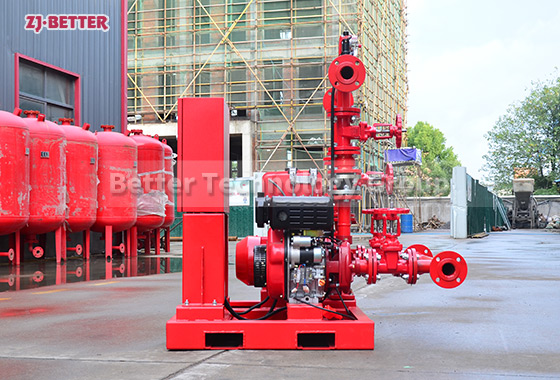
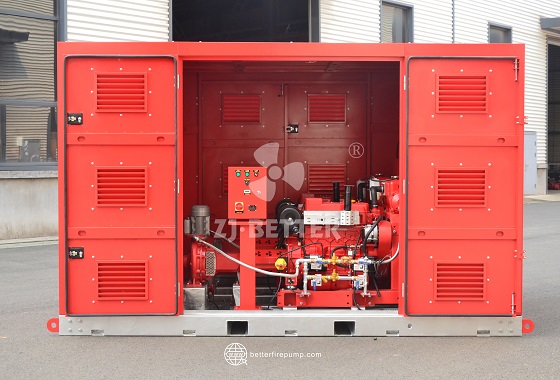
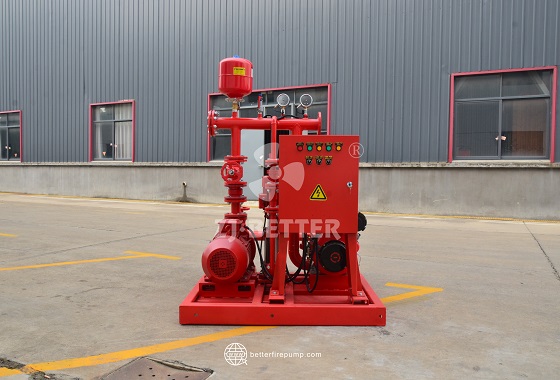
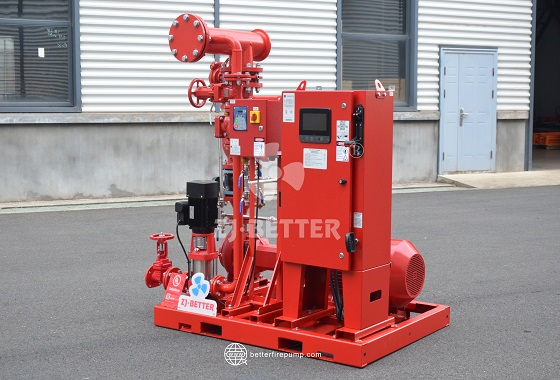
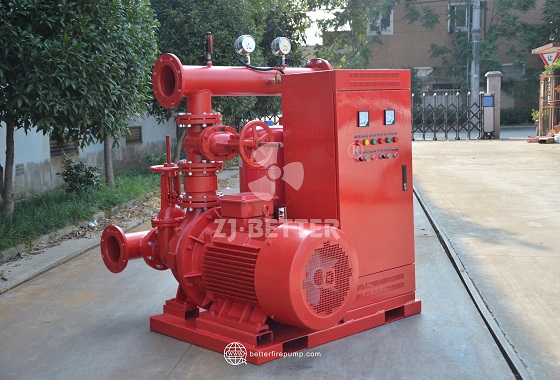
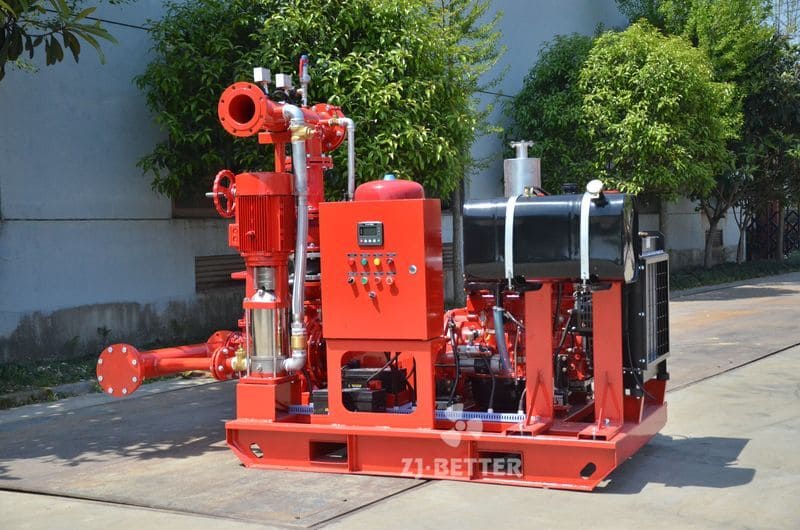
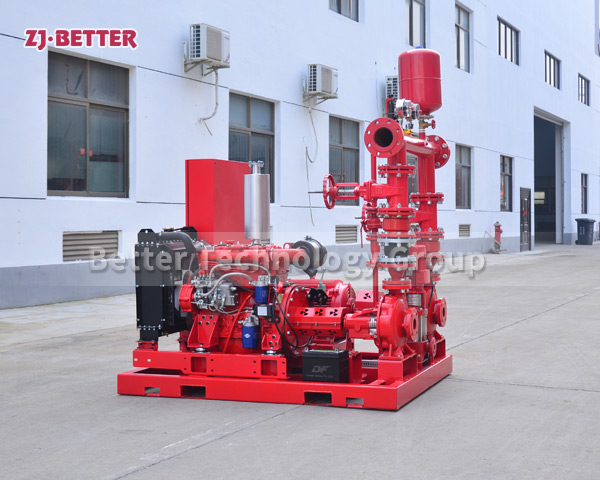
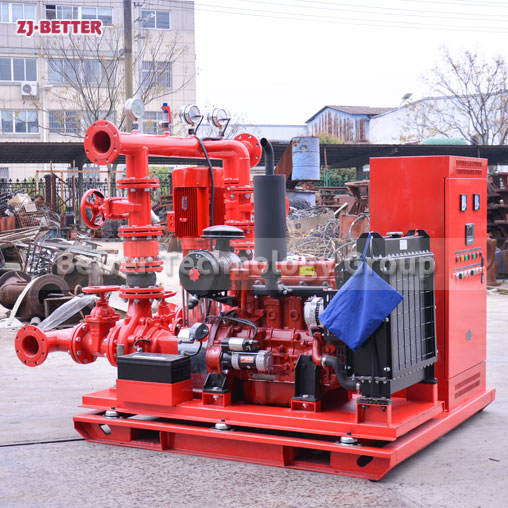
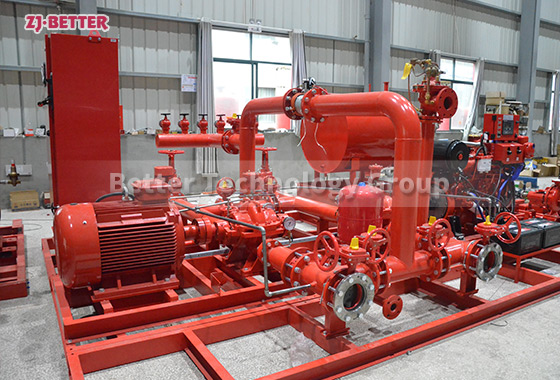
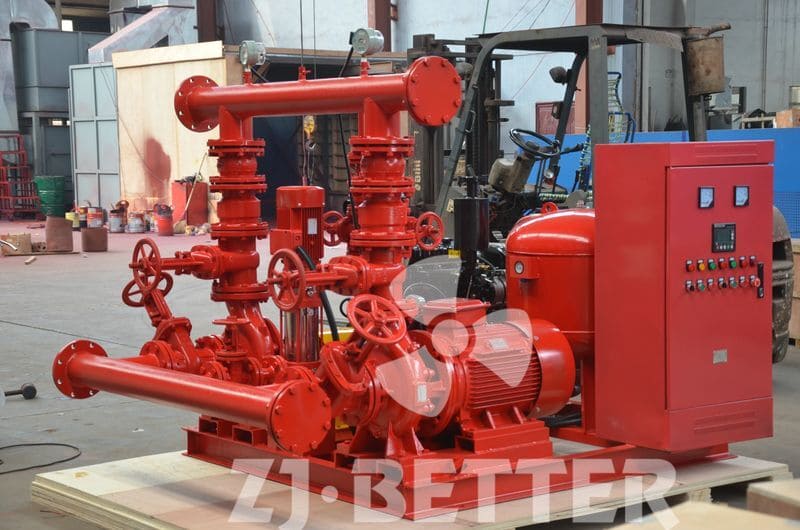
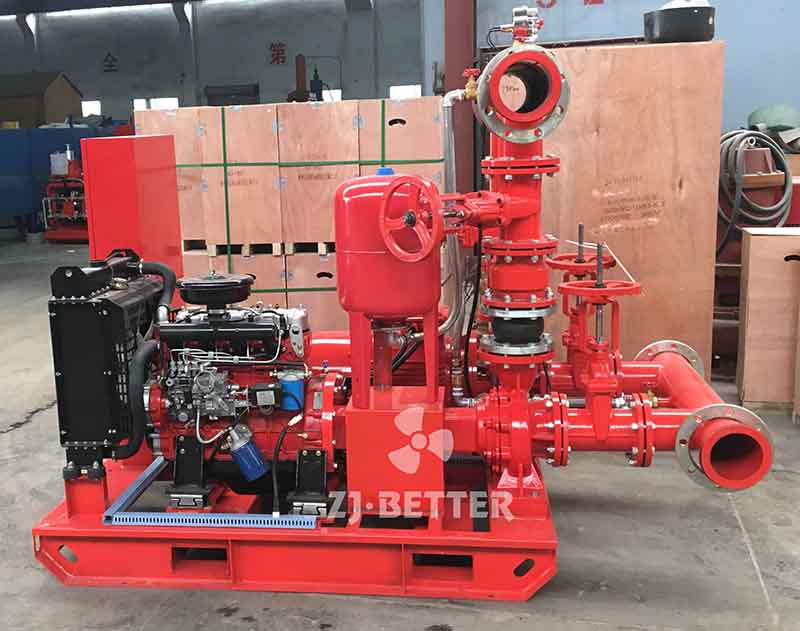
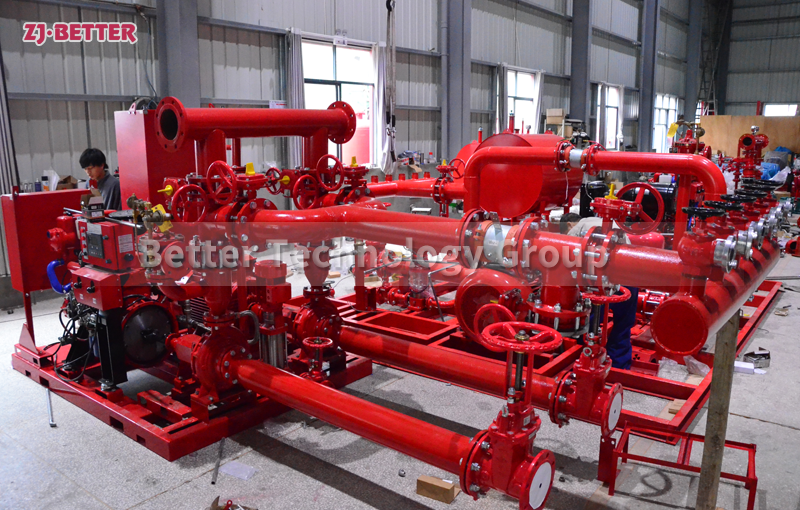
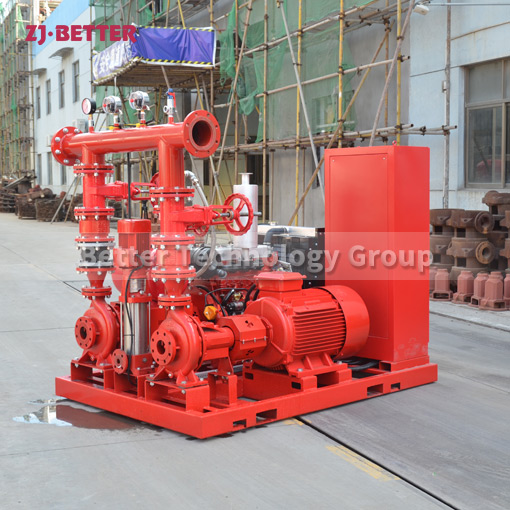
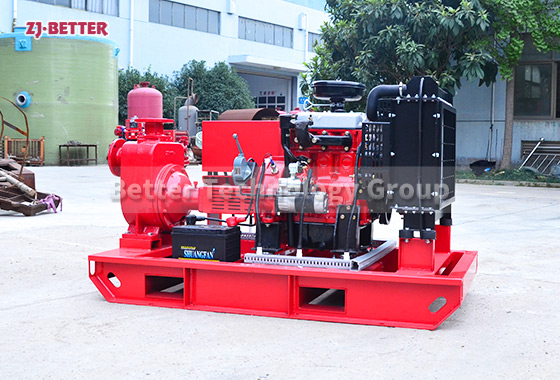
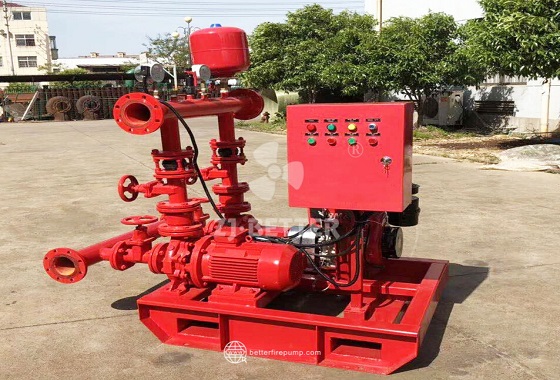
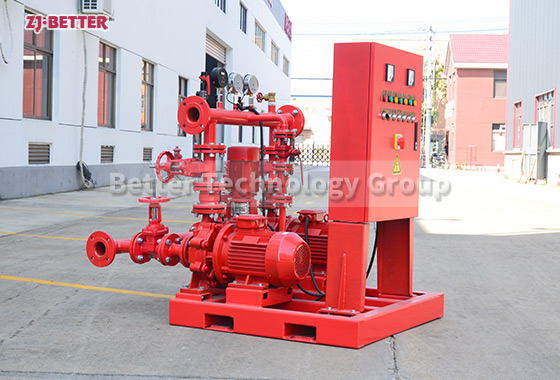
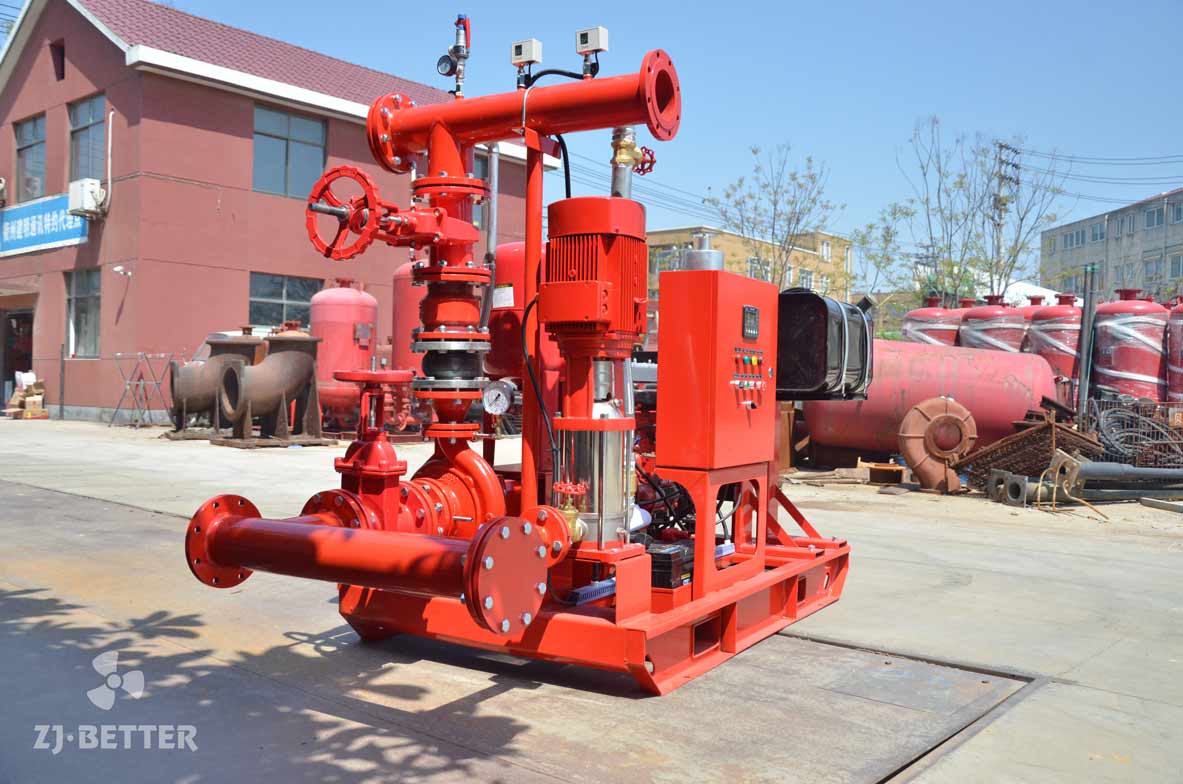
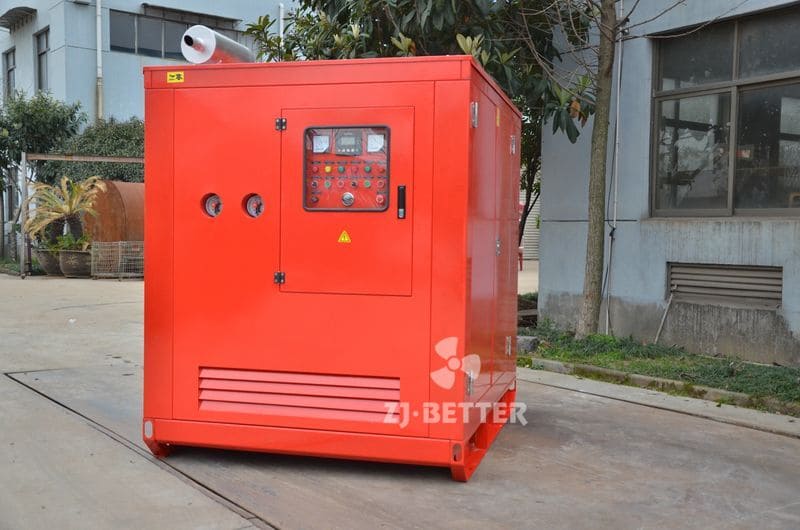
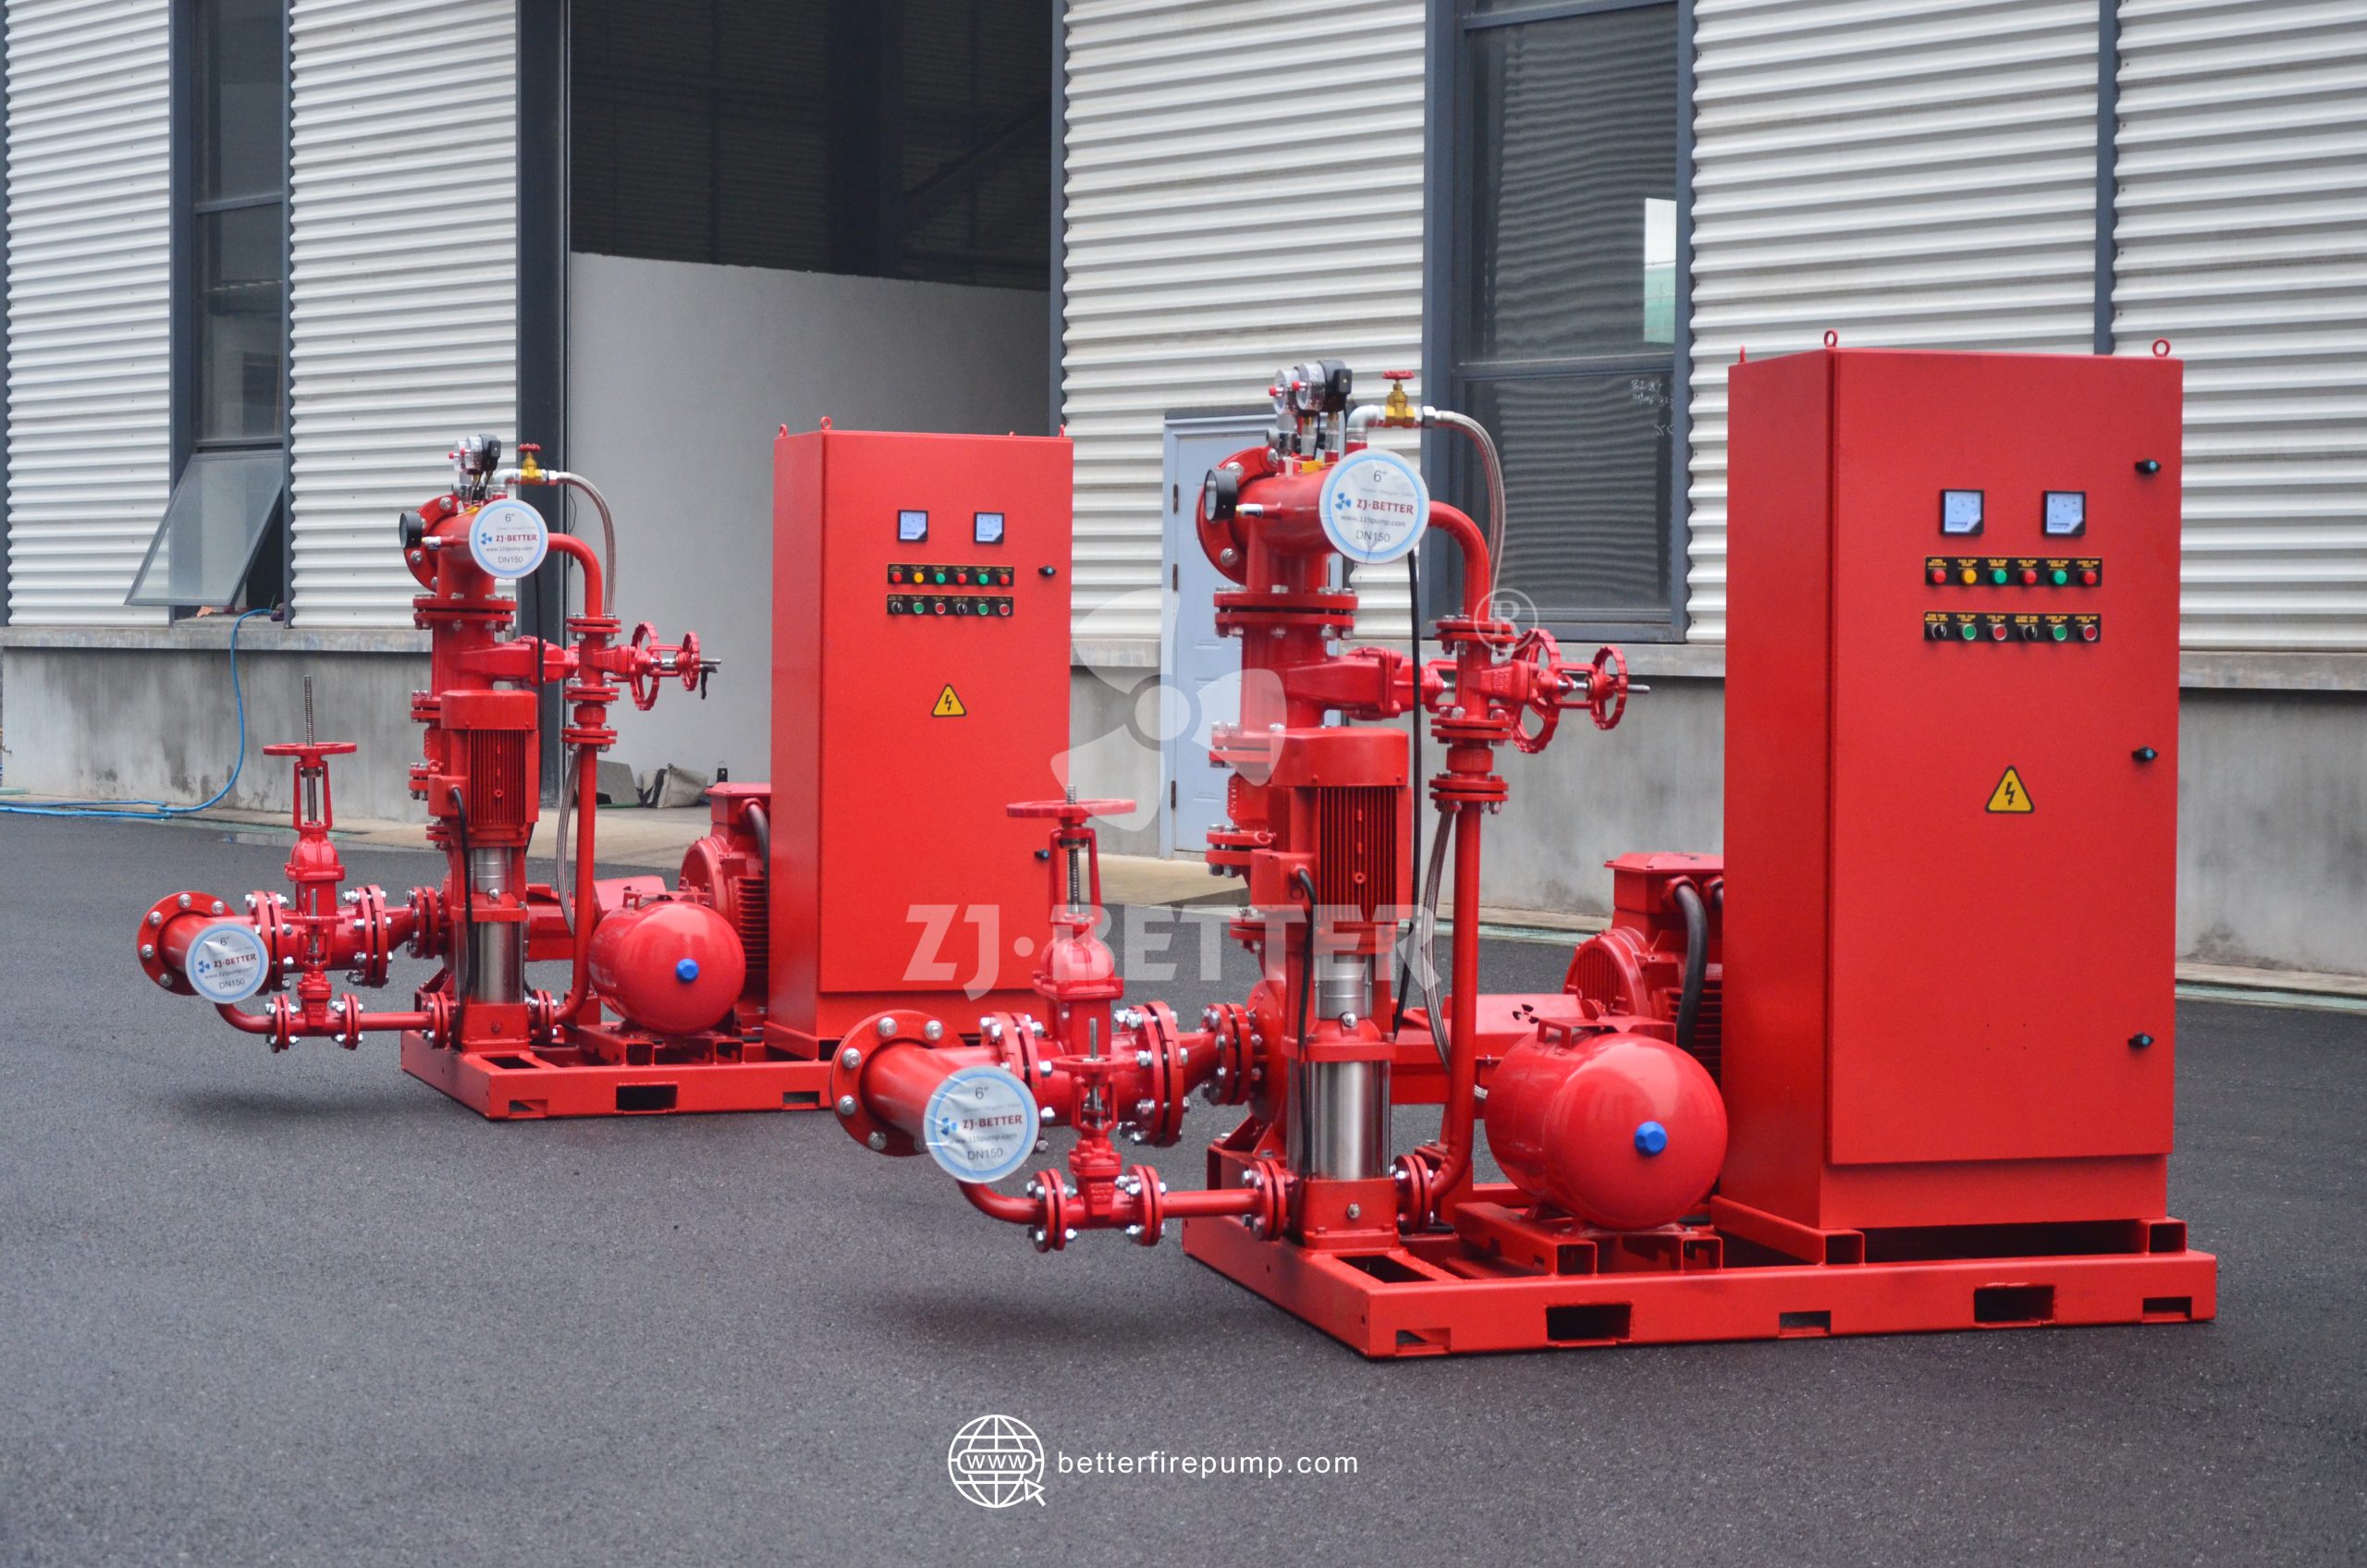
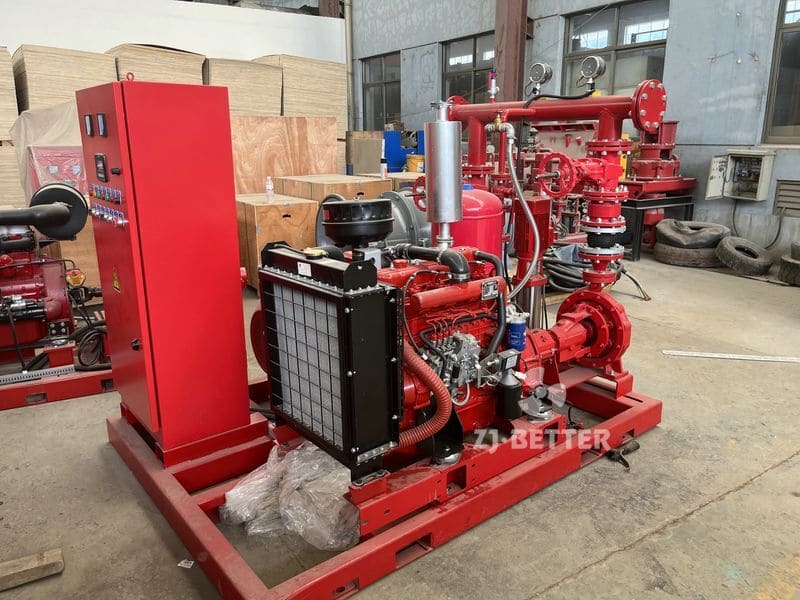
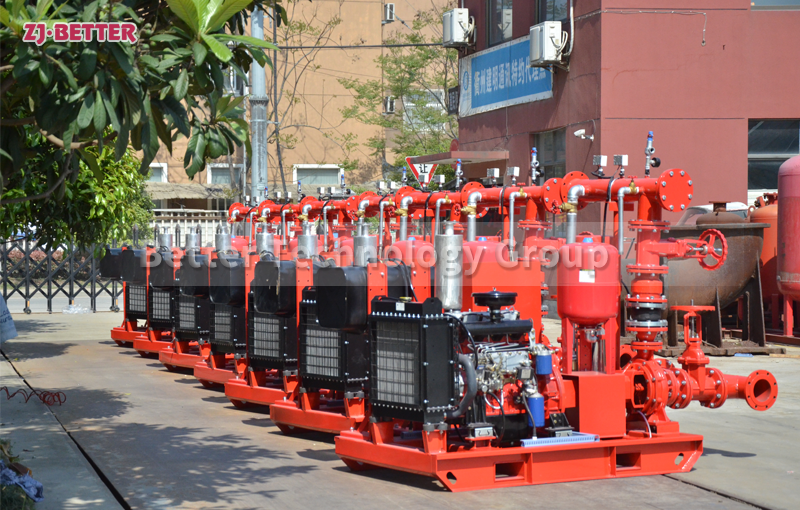
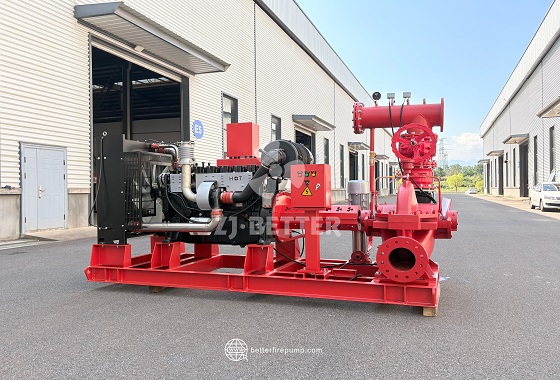
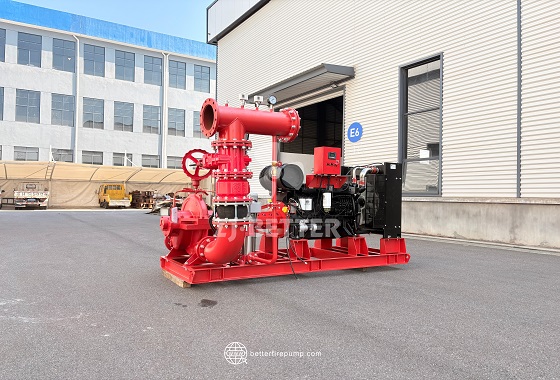
A high-capacity diesel fire pump unit is a complete power system designed for large-scale fire-fighting water supply projects. Powered by a diesel engine, it provides an independent drive source for the fire pump, making it highly suitable for industrial facilities, logistics warehouses, ports, airports, petrochemical plants, power facilities, and large-scale buildings that require substantial fire-fighting water supply capabilities. The unit shown in the image features a skid-mounted design, integrating the diesel engine, fire pump, control components, piping, valves, and related accessories into a single, cohesive pumping assembly. This configuration facilitates both transportation and on-site positioning and piping connections. For large-scale fire-fighting water supply systems, the core performance of the pump unit—encompassing flow rate, head, power, and operating conditions—must be comprehensively configured. These diesel fire pump units can be tailored with specific pump models to meet the unique water volume and pressure requirements of individual projects. Depending on the specific operating conditions, the system can utilize various pump configurations—such as end-suction pumps, horizontal split-case pumps, vertical split-case pumps, vertical in-line (pipeline) pumps, or vertical turbine pumps—offering significant flexibility in selection based on available installation space, water source conditions, flow requirements, and system layout. The diesel engine serves as the primary power source; its specifications are carefully matched to the power requirements of the fire pump to ensure reliable operation. Compared to procuring pumps and power units separately, this integrated design minimizes the complexities of component matching and simplifies overall equipment management for the project team. In large-scale fire-fighting water supply projects, the pump unit must deliver a consistent and stable water supply. Consequently, the equipment structure, engine power, pump performance, and piping configuration must be determined holistically based on project design parameters, rather than being judged solely by external appearance or isolated technical specifications. The unit is mounted on a common steel skid, which secures the primary components and ensures excellent structural stability. This skid-mounted approach reduces the labor associated with installing scattered components on-site and allows for efficient, integrated planning within the fire pump room. Depending on system requirements, the pump unit can be configured with components such as control cabinets, pressure gauges, pressure sensors, check valves, gate valves, flexible connectors, flanges, and shared inlet/outlet piping. This creates a comprehensive, integrated assembly comprising the fire pump, power system, and piping equipment. The control system can be tailored to specific project requirements to manage the operation of the diesel engine and associated pump equipment; it may also include protective functions—such as overcurrent and overload protection—to facilitate operational management. For projects requiring high-flow fire water supply, the selection of an appropriate pump type and careful piping design are critical. Factors such as inlet/outlet pipe diameters, pipeline resistance, installation height, and the characteristics of the fire water source all influence actual operational performance. Consequently, hydraulic calculations based on the system’s design flow rate and head are essential during the equipment selection process. Parameters can be configured to meet the needs of individual projects; according to official documentation, these diesel fire pump units cover a flow range of 30–9000 GPM and a head range of 3–20 bar, with actual performance contingent upon the specific model, engine configuration, and operational conditions. For industrial facilities, warehouses, ports, airports, petrochemical plants, power stations, and other large-scale fire protection applications, suitable diesel fire pump units can be selected based on building scale, fire protection system design requirements, and site-specific installation conditions. In summary, high-flow diesel fire pump units offer several advantages: independent diesel power, flexible pump selection, a high degree of integration, skid-mounted designs for easy installation, and suitability for large-scale fire water supply projects. By effectively matching the fire pump, diesel engine, piping, and control components, these units can be configured to suit various engineering environments, providing the necessary hydraulic capacity for large-scale fire protection systems. During the selection process, one should conduct a comprehensive assessment—based on fire protection design parameters—of flow rate, head, power output, pump type, water source conditions, and available installation space to ensure the chosen diesel fire pump unit aligns with the project’s specific requirements.