Home » Diesel engine fire pump » Chemical diesel engine pump set

Chemical diesel engine pump set

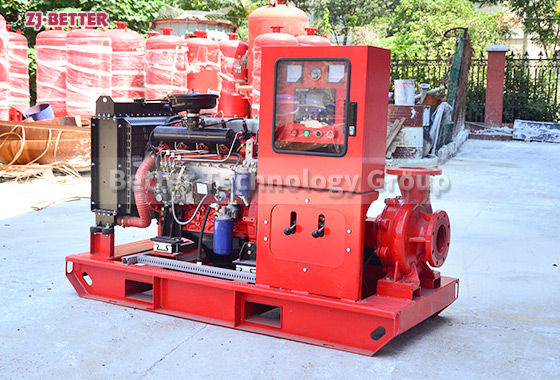
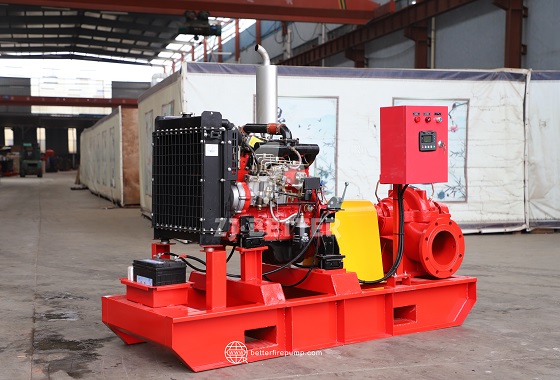
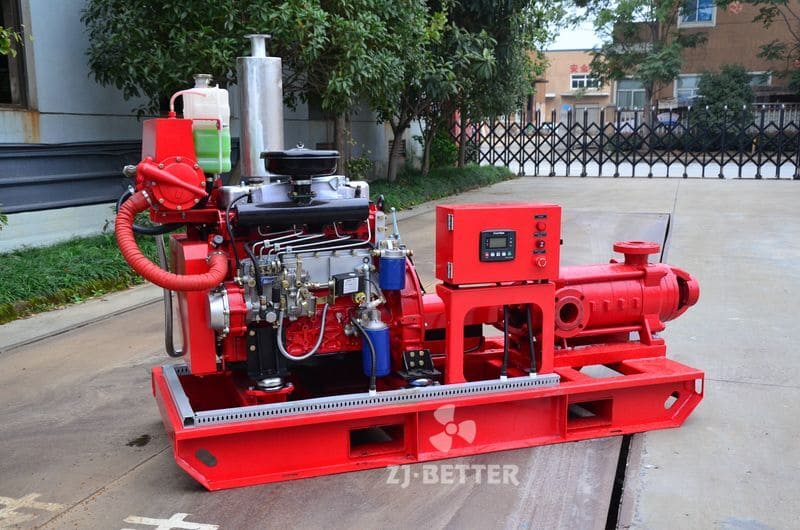
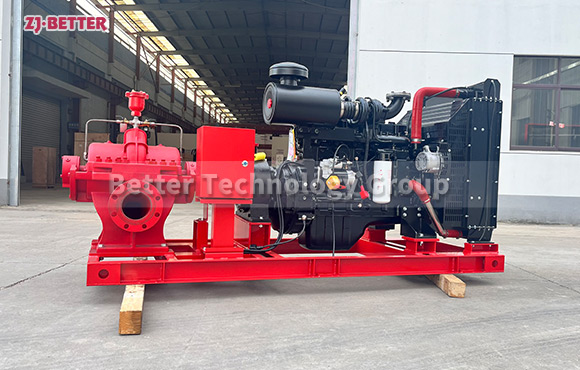
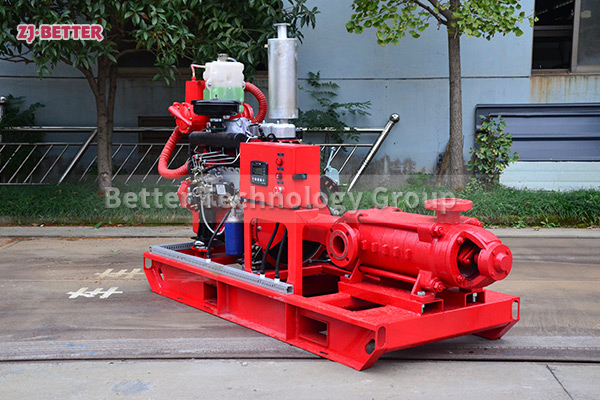
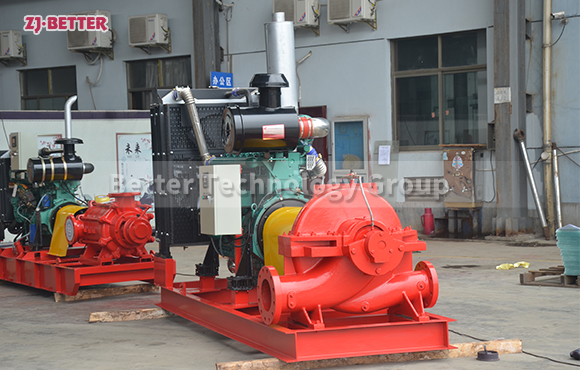
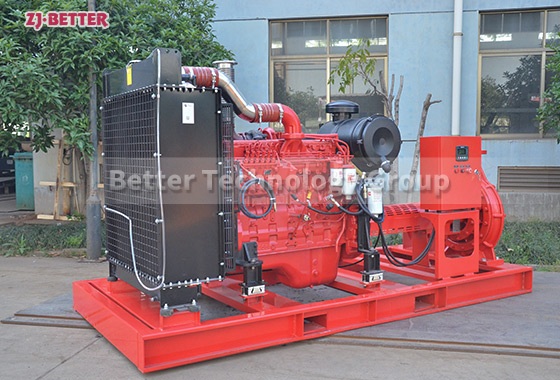
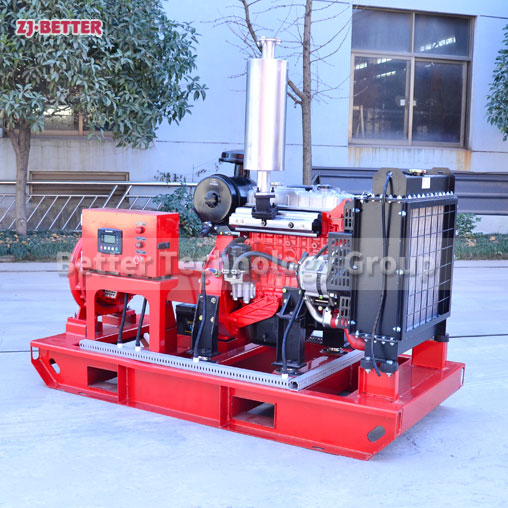
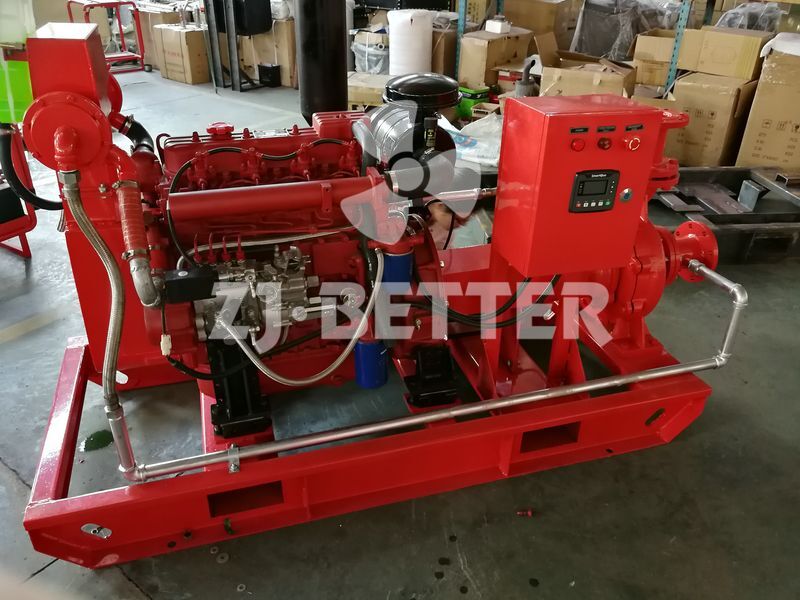
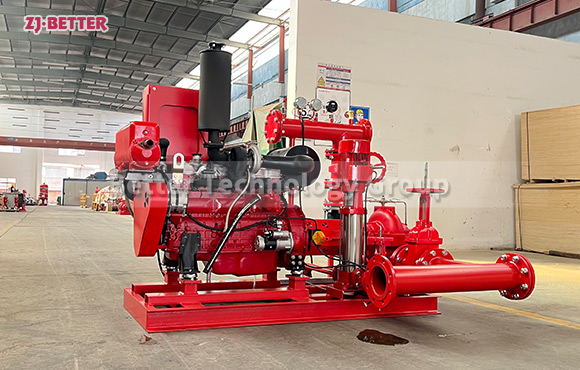
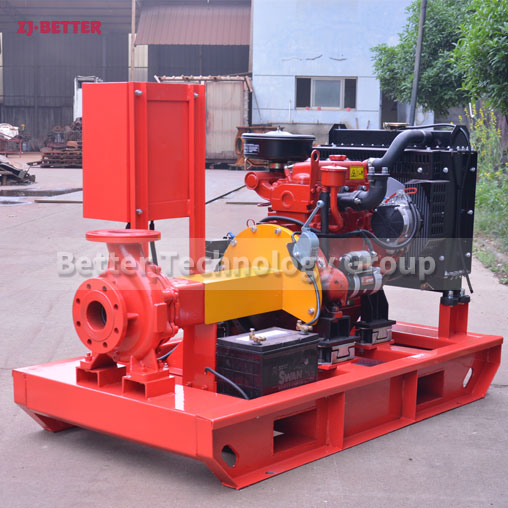
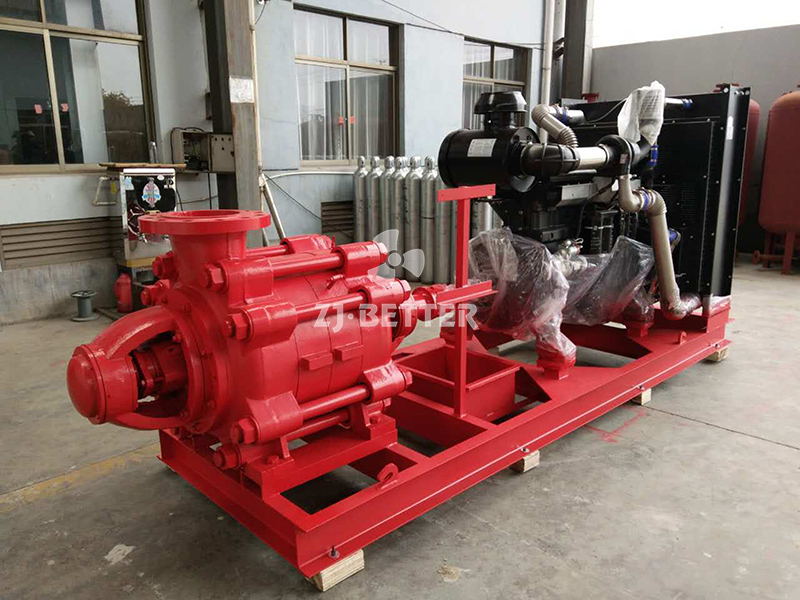
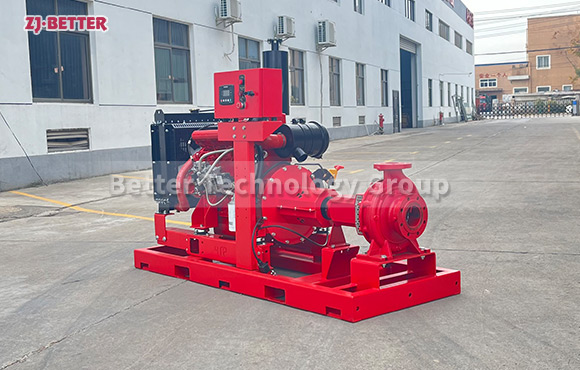
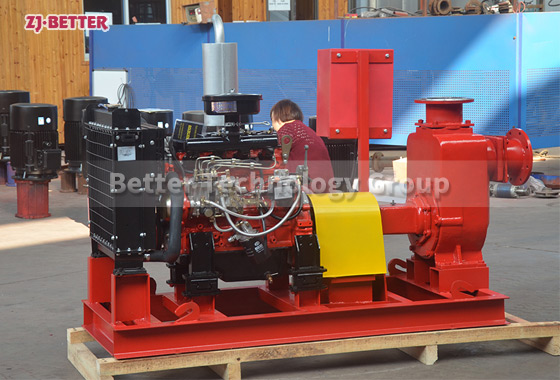
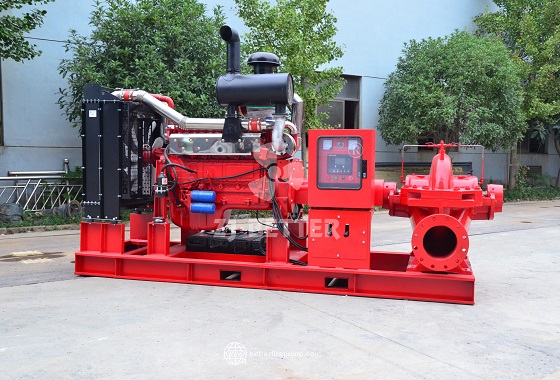
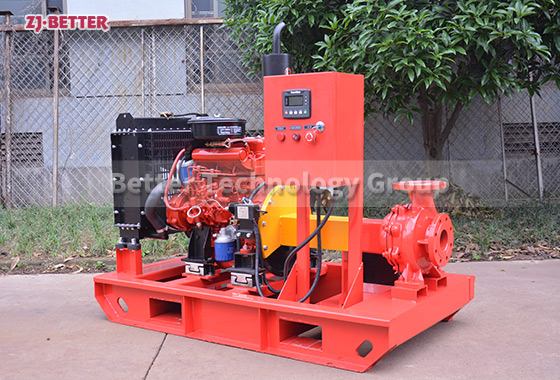
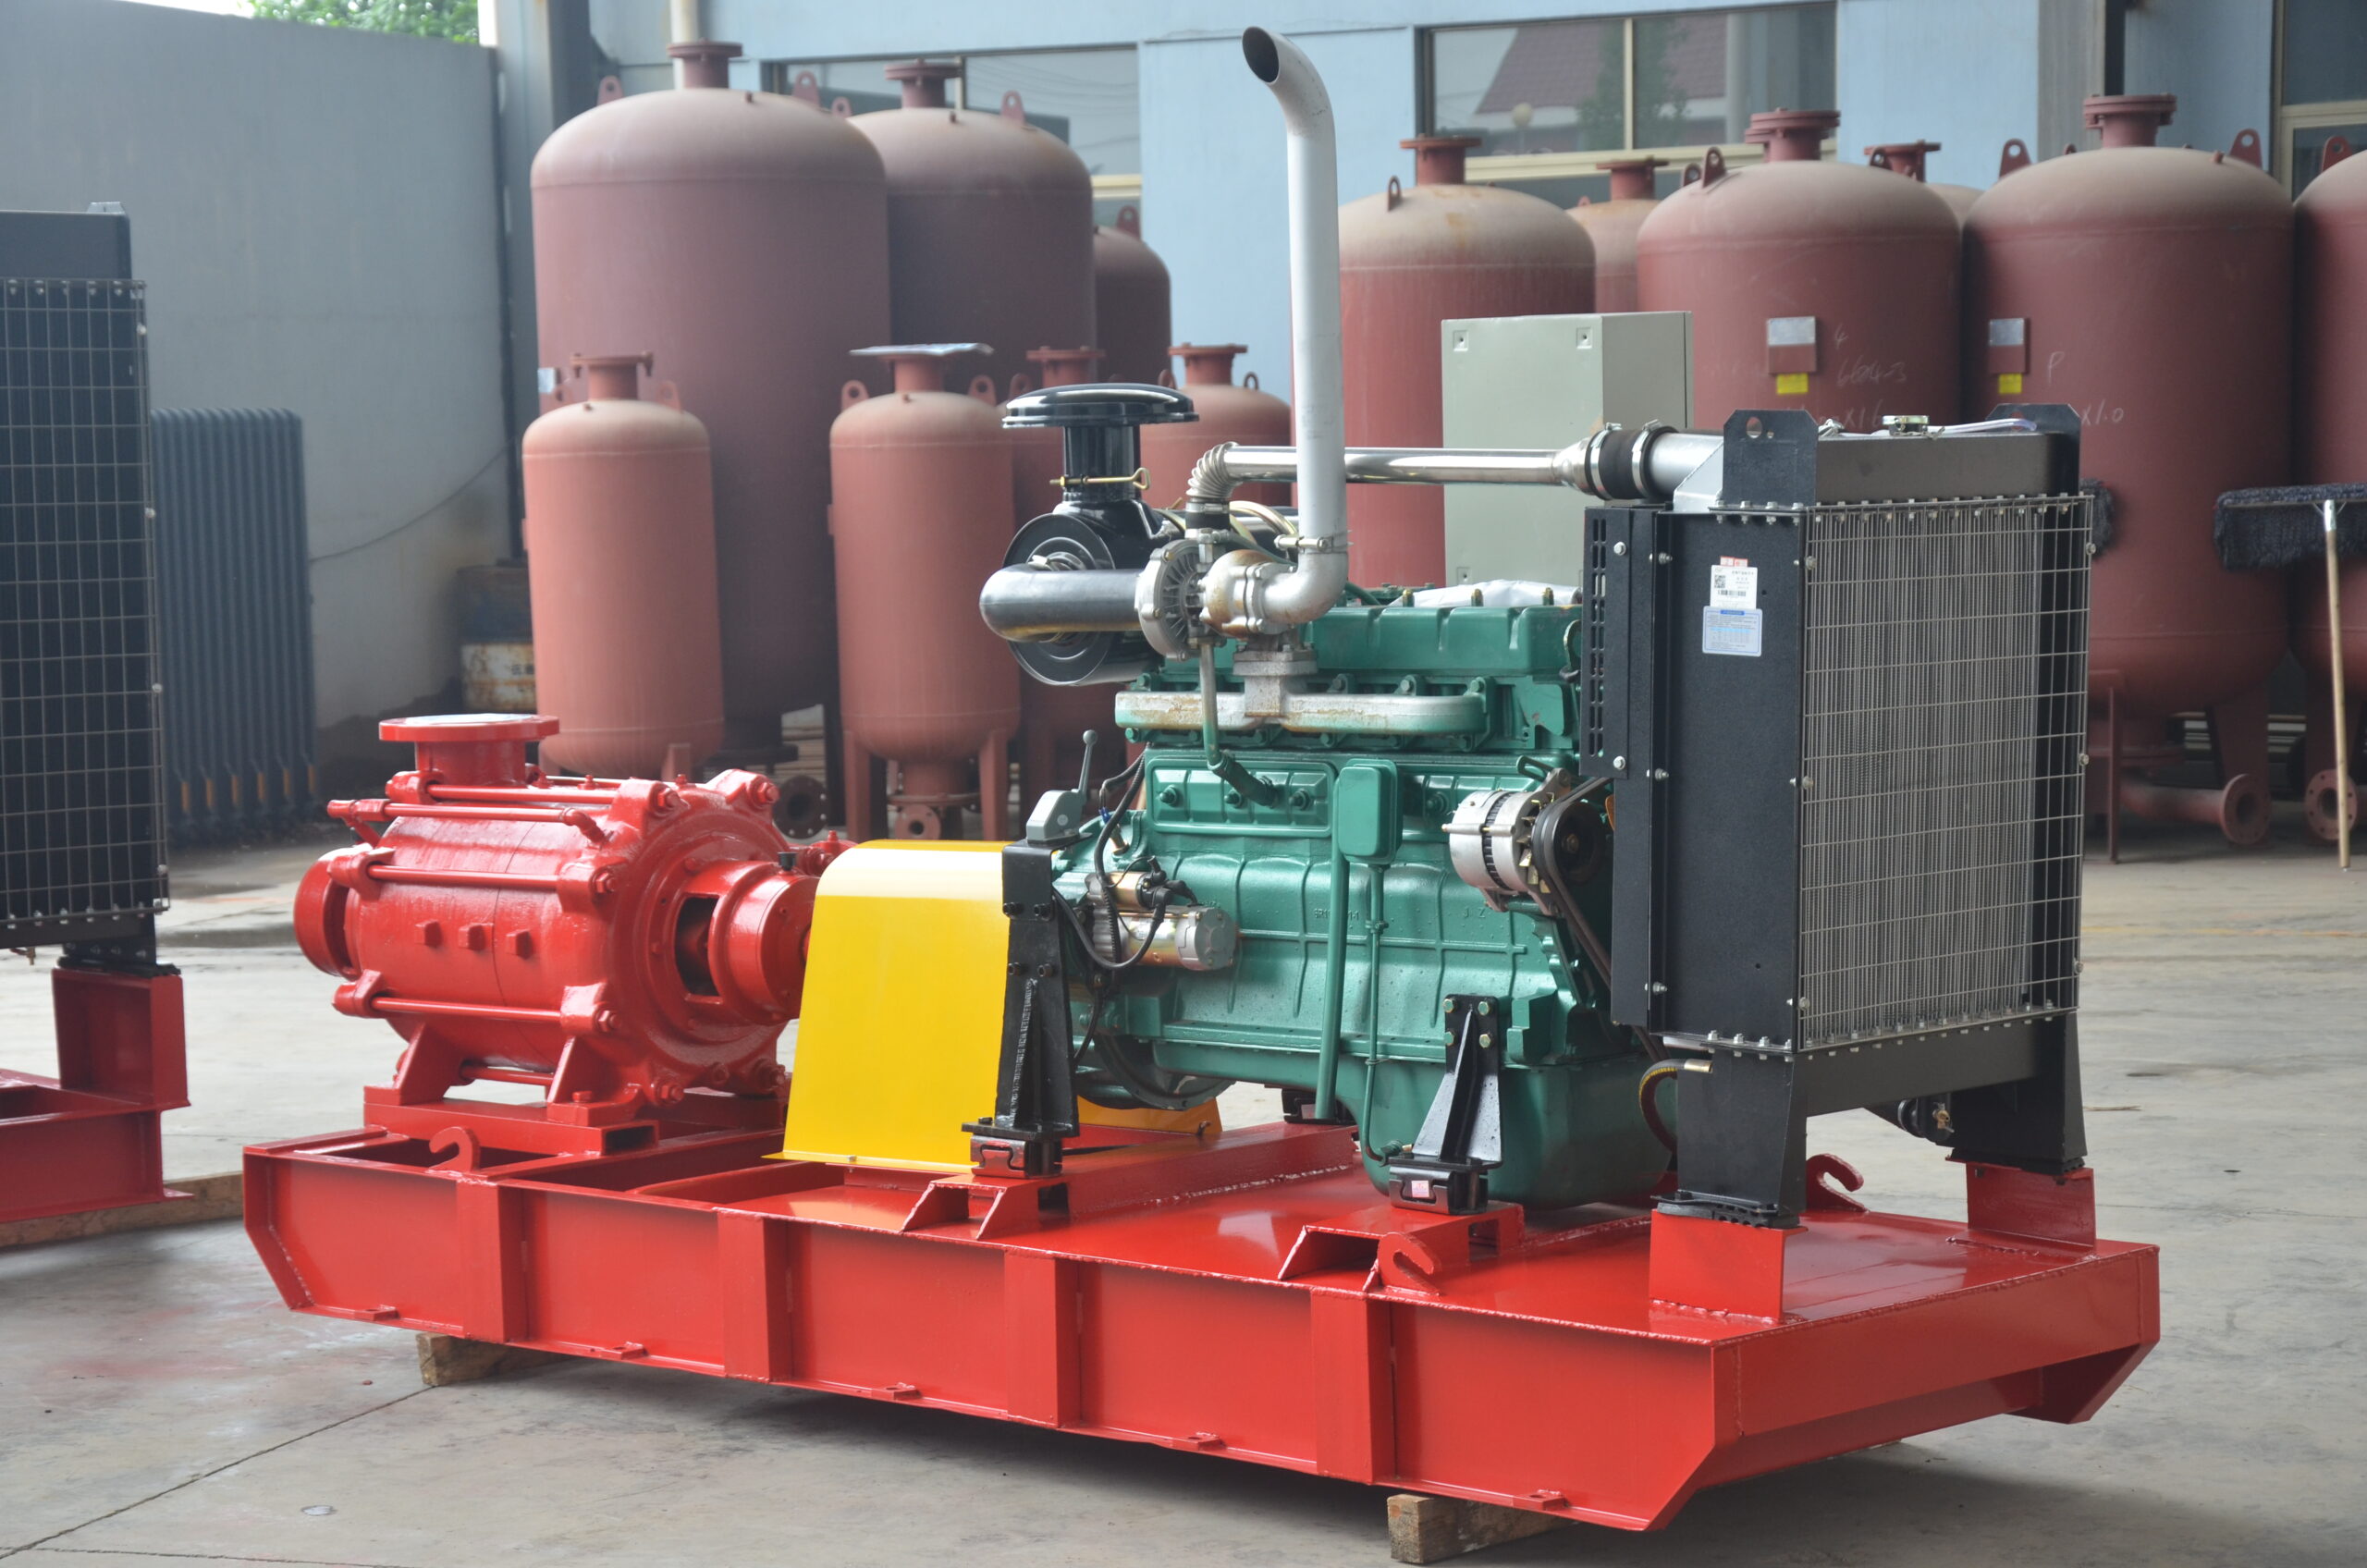
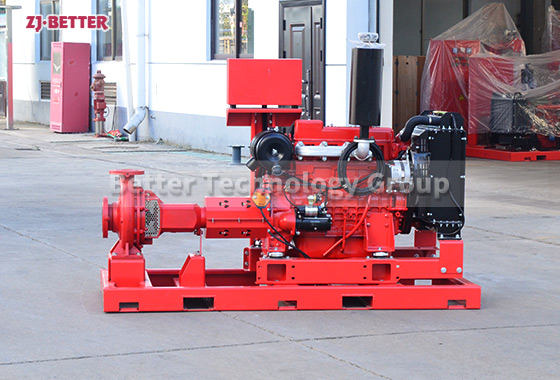
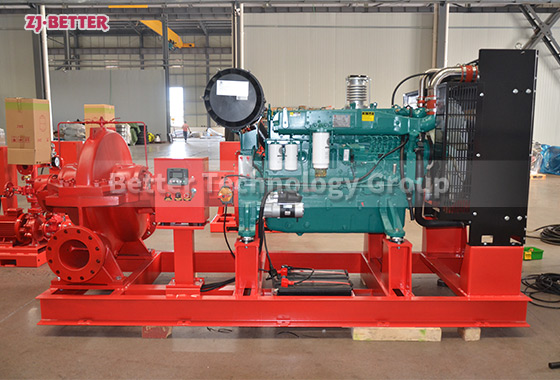
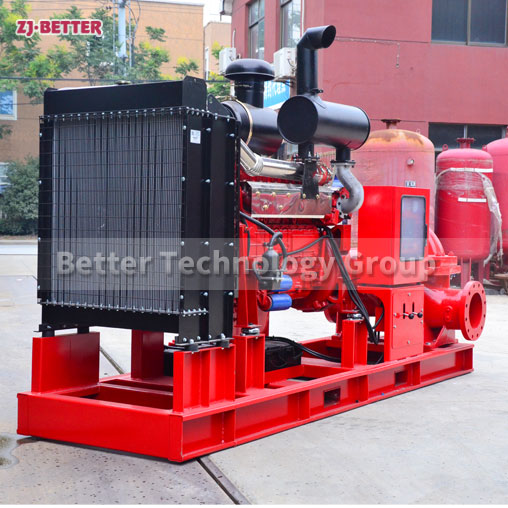
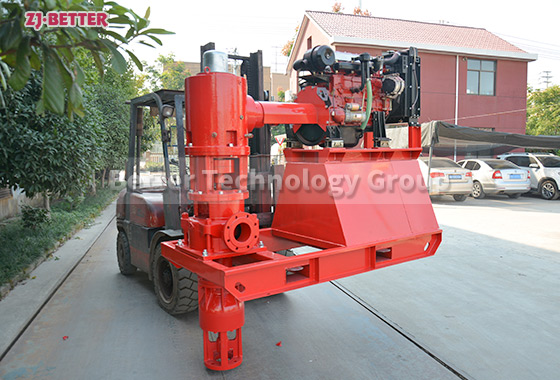
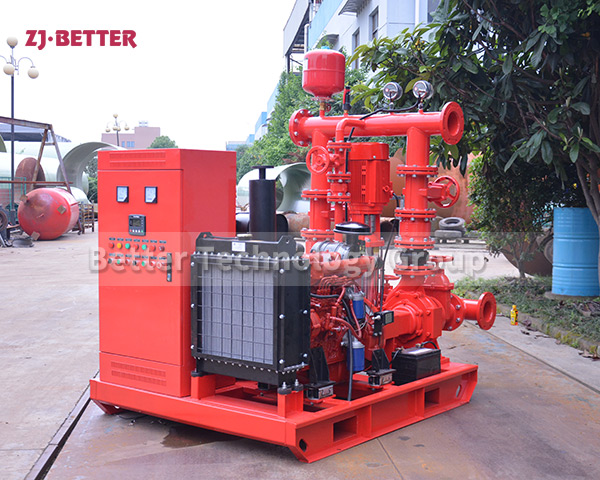
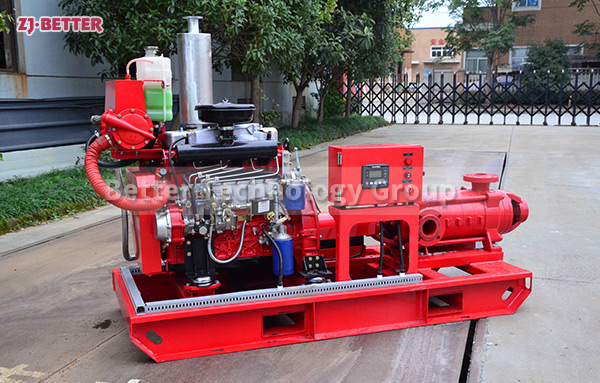
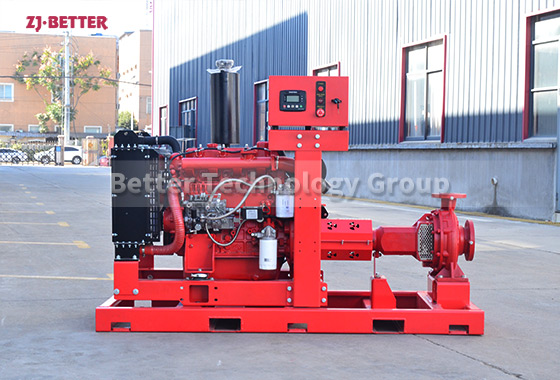
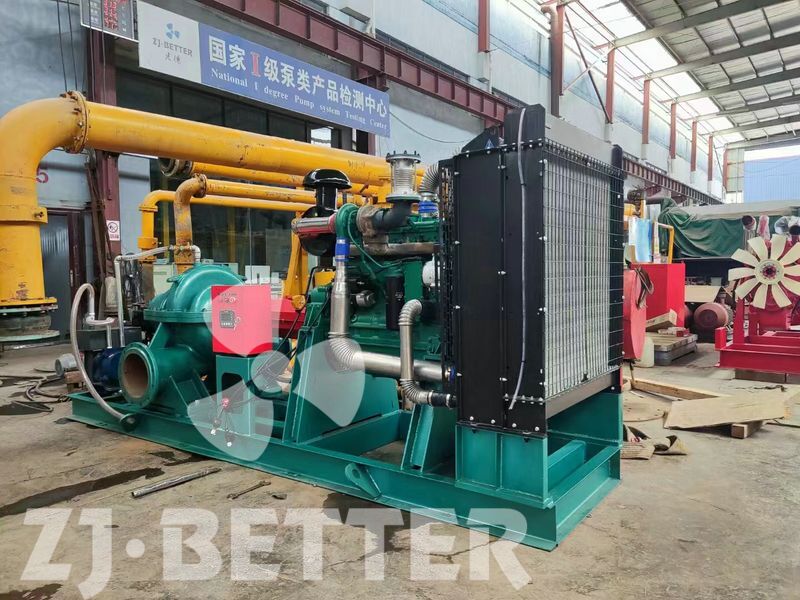
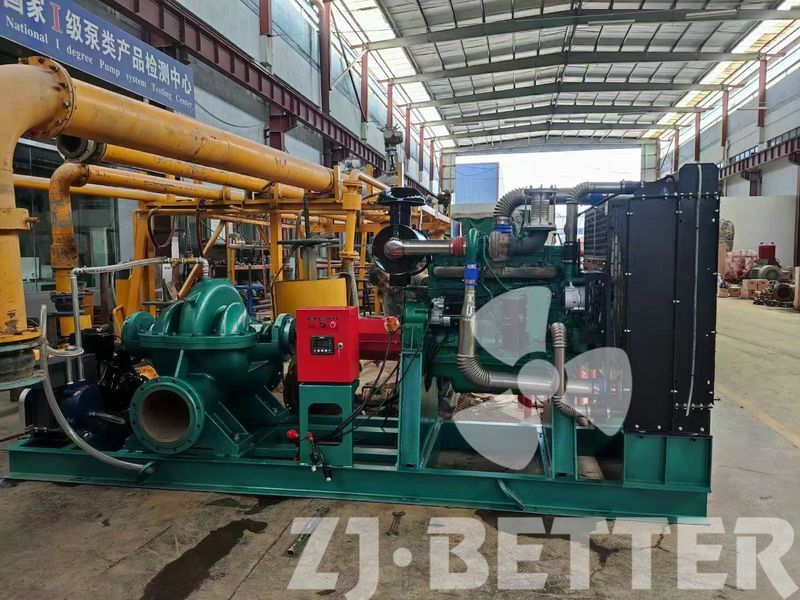
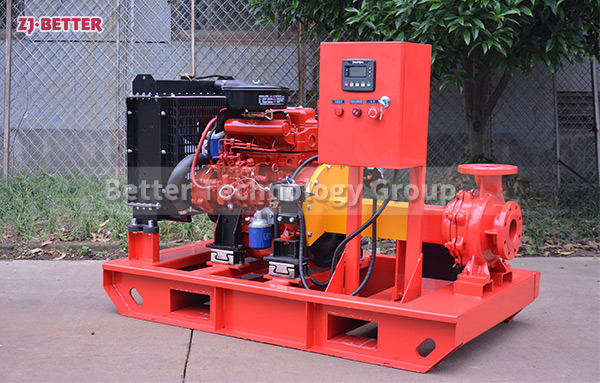
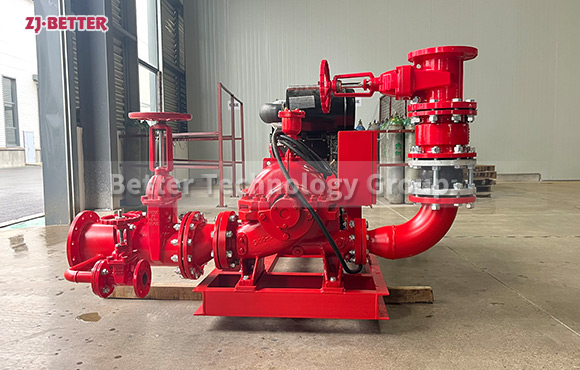
The national standard name of the diesel engine fire pump is “engineering diesel engine fire pump group”, and the national standard model is XBCL/Q where L is the lift value and Q is the flow value. XBC diesel engine fire pump set is the latest according to the national standard GB6245-2006 “fire pump performance requirements and test methods”. This series of products has a wide range of lift and flow, and can fully meet the fire water supply in various occasions such as warehouses, docks, airports, petrochemicals, power plants, liquefied gas stations, textiles and other industrial and mining enterprises.

Rated 4.7/5 based on 317 customer reviews
Share:
Content

After more than 10 years development, BETTER PUMP has won awards including all kinds of certificates awards by governments institutional and society. As we have professional R&D team, our products has got the Certificate of Utility Model Patent and Certificate of Design Patent. And our factory has got Production License, authentication from SGS, Export License from government. We are also have many honor, the enterprise of Vice Chairman of Quzhou Network Association, the cooperative enterprise with Quzhou colleges and universities. We are also a member of Wenzhou Commerce, Quzhou disabled people internship foundation. All of our products accord with machinery industries standard JB/T5118-2001.
Inquiry


    More Diesel engine fire pump

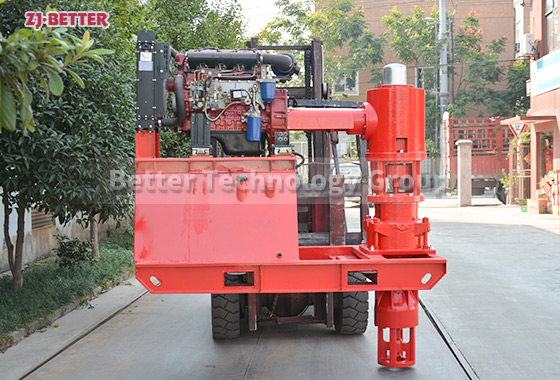
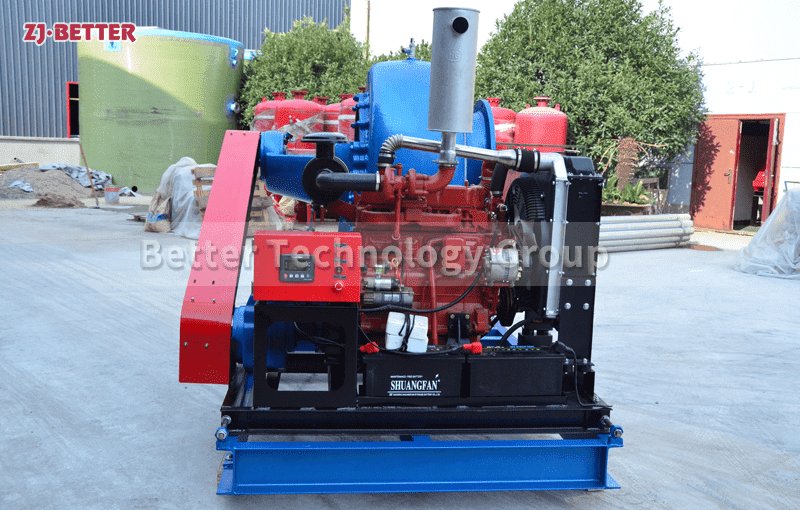
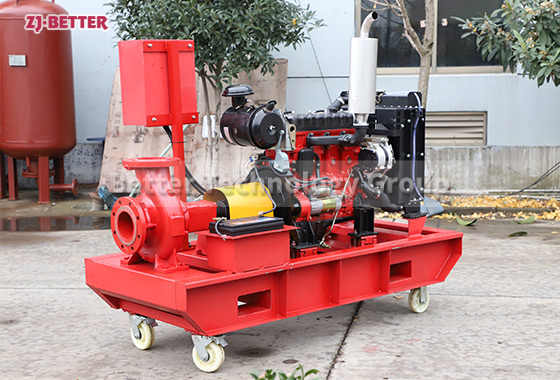
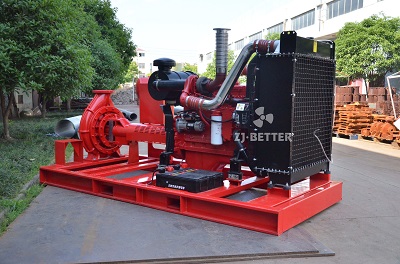
    Our fire pump is renowned for its outstanding performance and reliability, specifically designed to respond to fire emergencies efficiently. It can start quickly in critical situations, ensuring a stable and efficient water supply. Whether in commercial buildings, industrial facilities, or public places, our fire pump delivers powerful performance and high head, swiftly transporting water to designated areas to ensure efficient firefighting operations.

    The product features advanced hydraulic design and an energy-efficient motor, which not only ensures smooth operation but also effectively reduces energy consumption and operating costs. Its low-noise characteristic makes it particularly suitable for environments with strict noise control requirements, maintaining quiet and reliable operation even during 24/7 use. High-quality materials and meticulous manufacturing processes provide excellent durability, enabling the pump to work stably for long periods in high-temperature, high-pressure, and corrosive environments.

    Equipped with an intelligent control system, the fire pump offers real-time monitoring, remote control, and fault alarm functions. Through a high-definition display, operators can easily monitor the operational status and quickly access parameters such as flow rate, pressure, and temperature. The built-in alarm system promptly issues warnings in case of abnormal operation, minimizing safety risks. The user-friendly maintenance design makes routine servicing simpler, prolonging the pump’s lifespan.

    We are committed to providing customers with reliable fire pump solutions, combining superior performance with user-friendly design to ensure comprehensive fire safety. Whether for new construction projects or equipment upgrades, our products are always your top choice.