Diesel Engine Fire Pump Set with Large Radiator for Continuous-Duty Applications
Equipped with a large, high-efficiency radiator and a diesel power system, this diesel fire pump unit maintains a stable engine operating temperature and supports prolonged, continuous operation. It can be flexibly configured based on flow rate, head, and specific project requirements, making it suitable for fire water supply systems in large-scale industrial facilities and buildings.
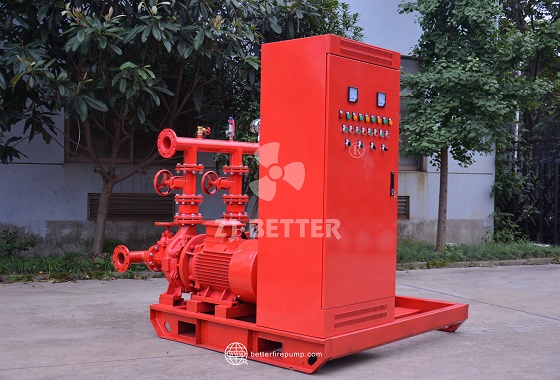
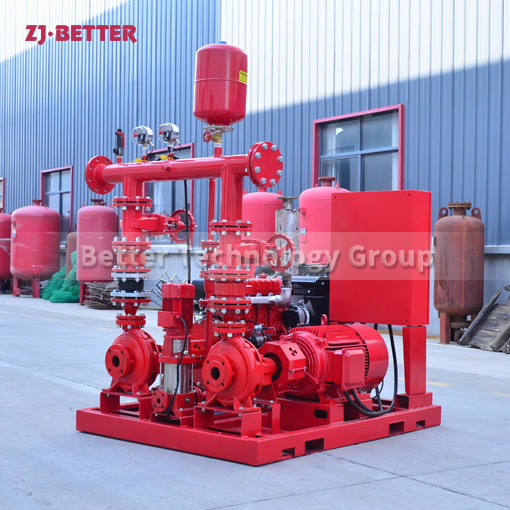
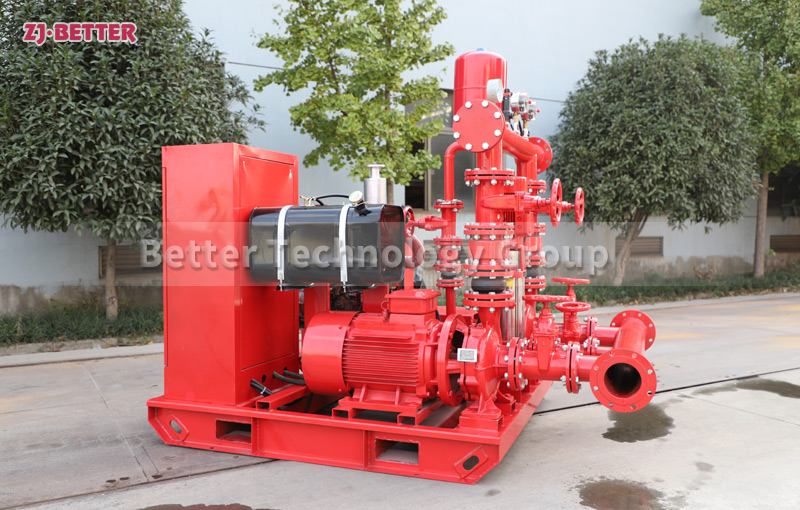
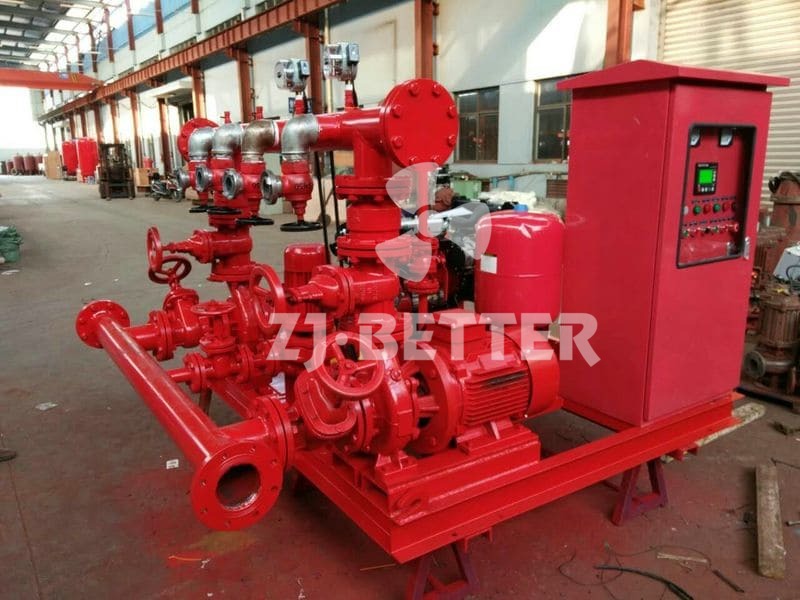
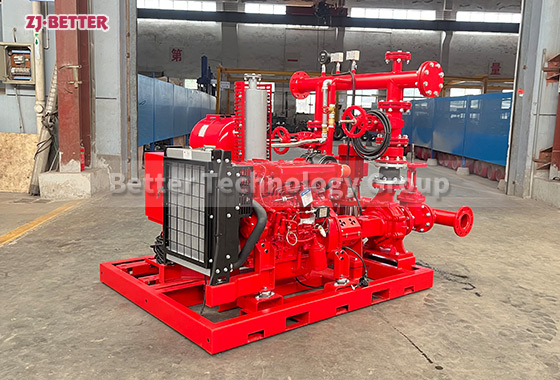
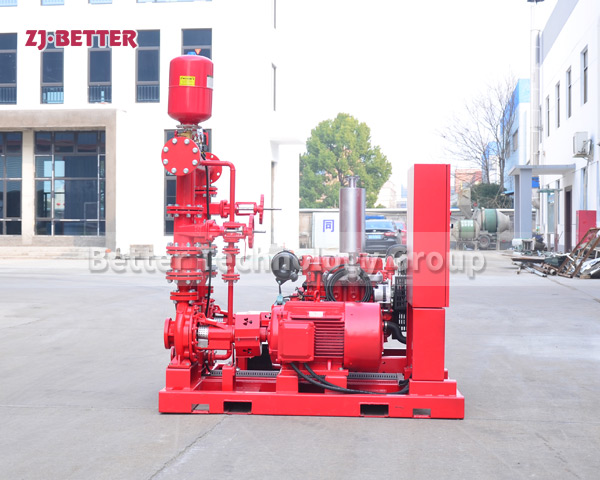
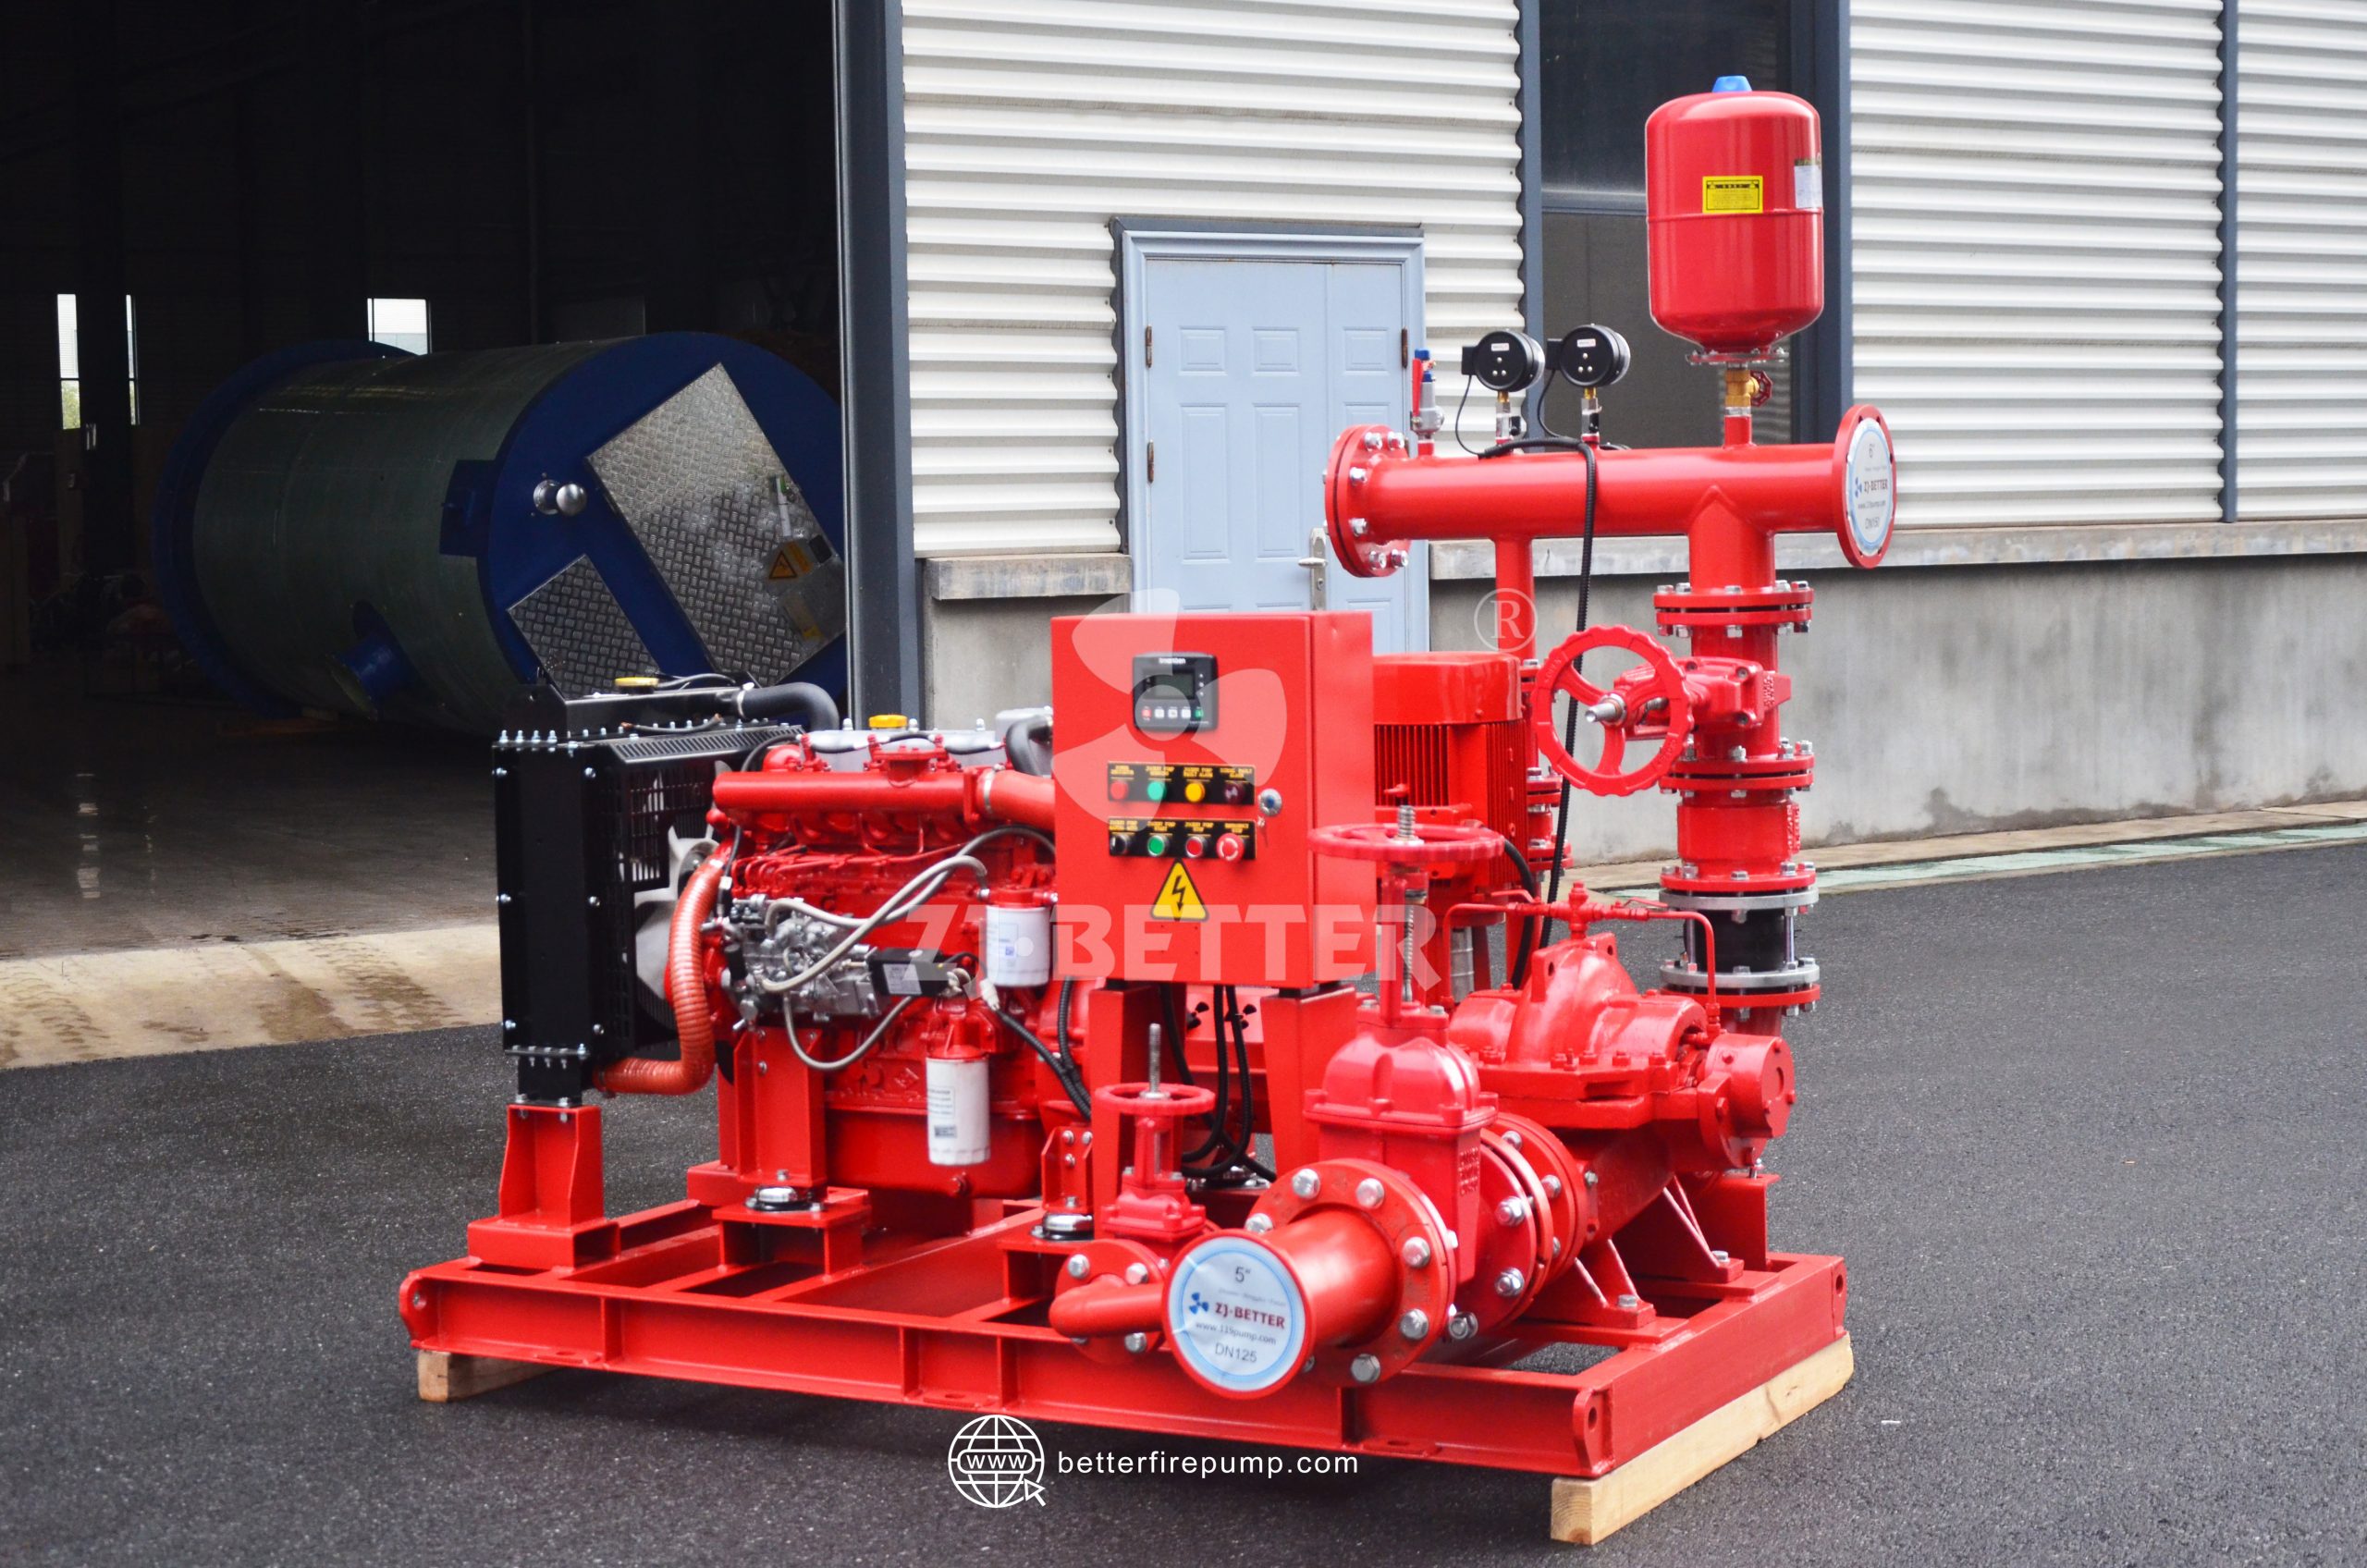
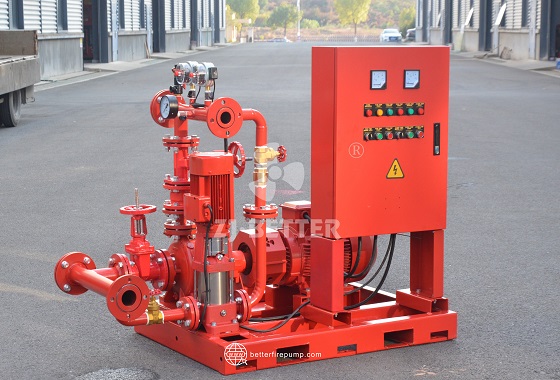
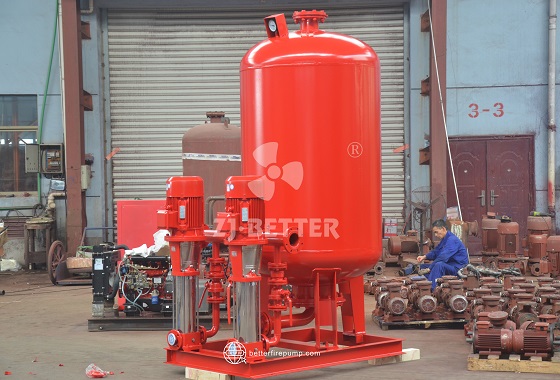
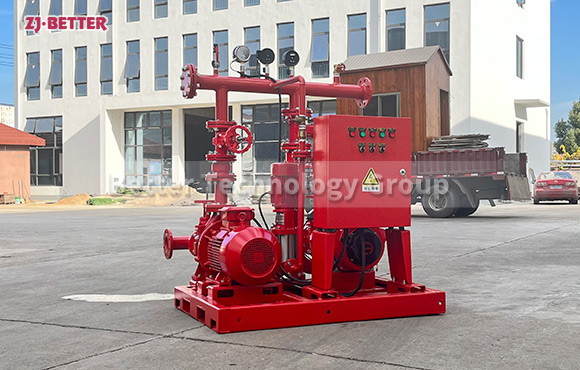
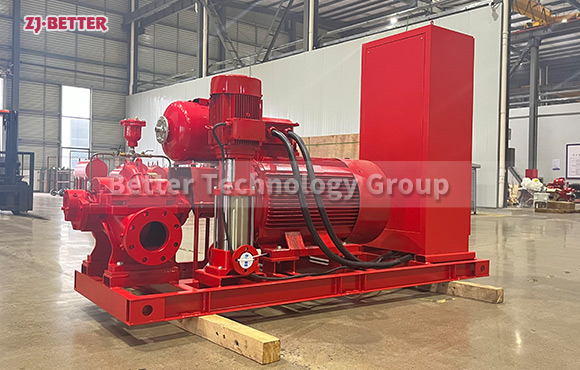
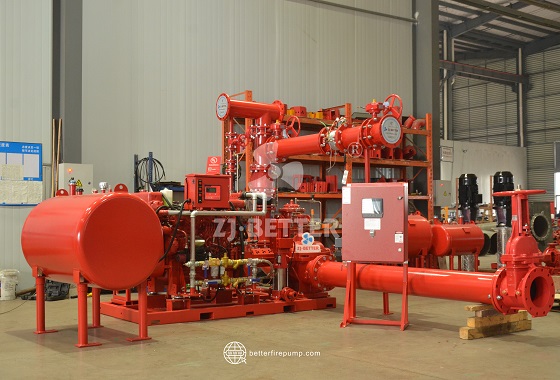
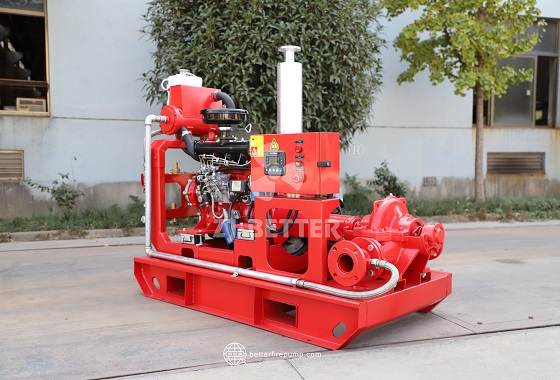
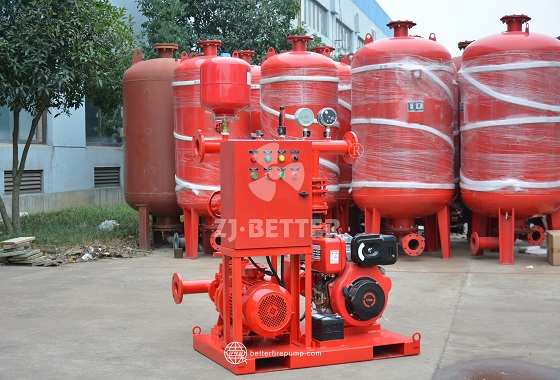
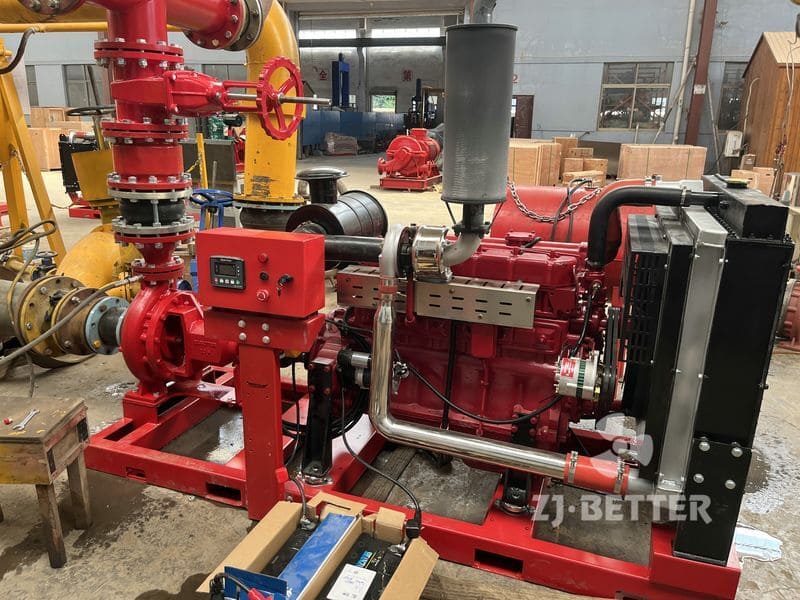
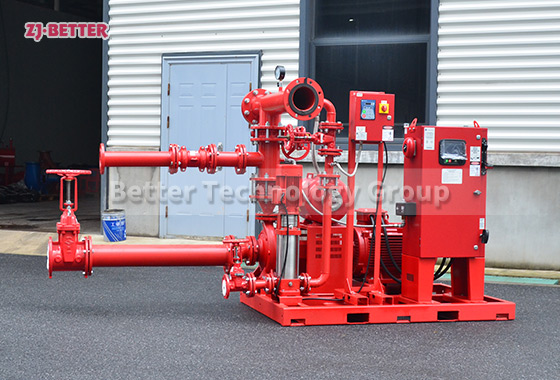
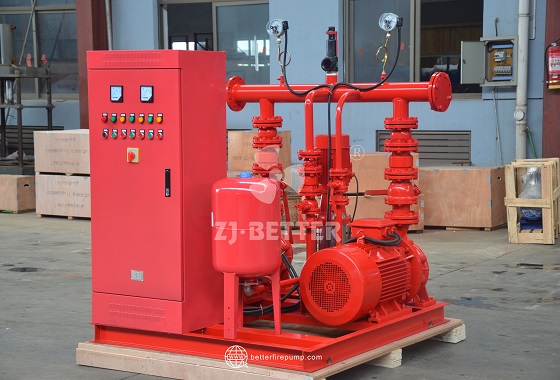
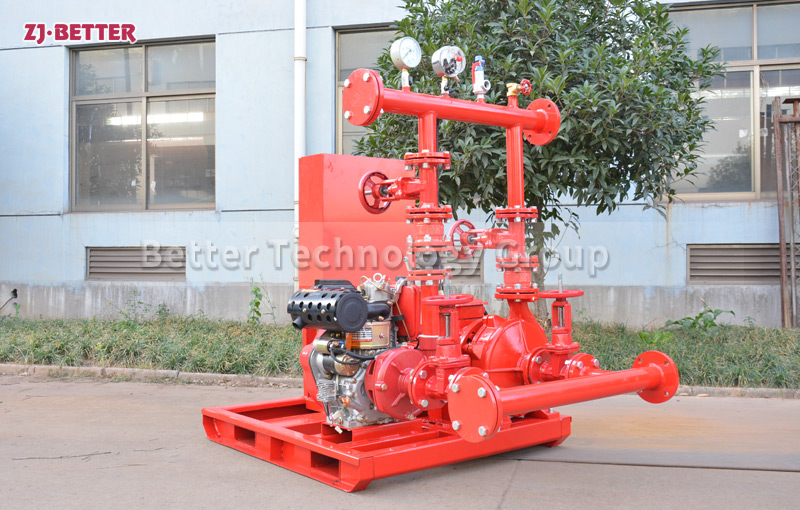
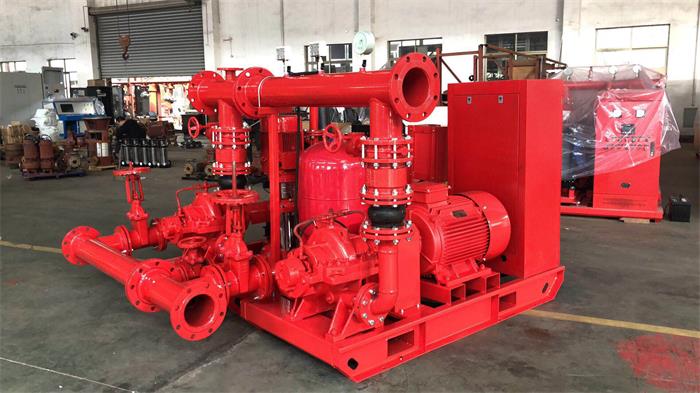
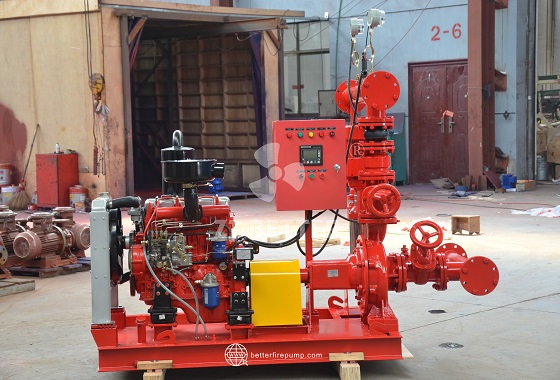
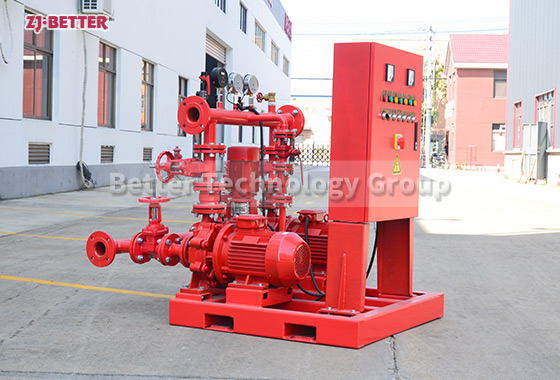
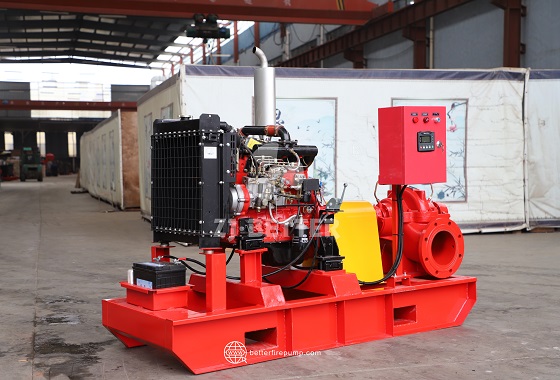
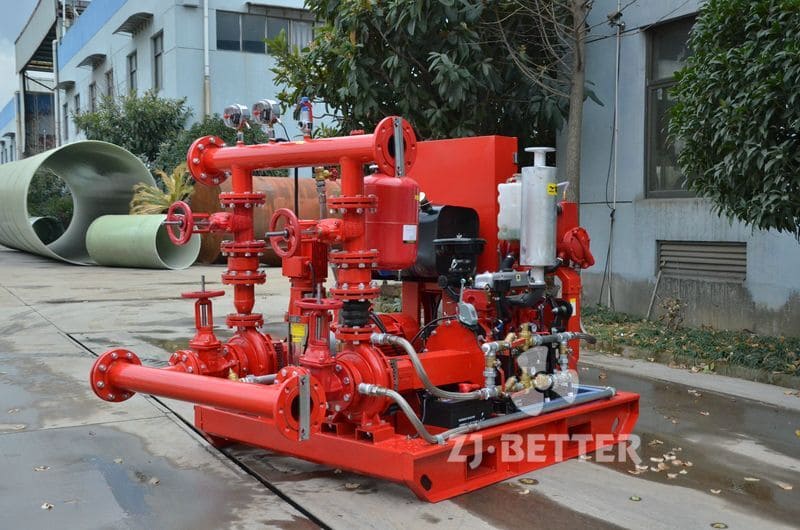
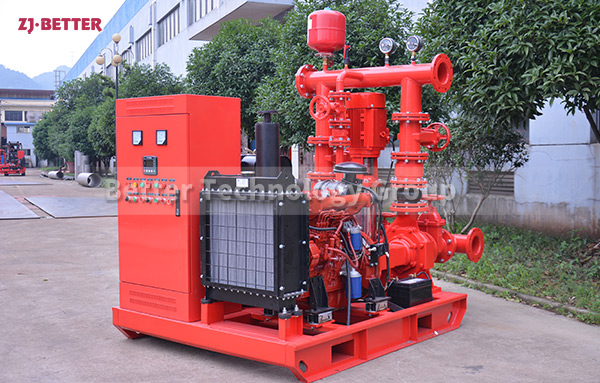
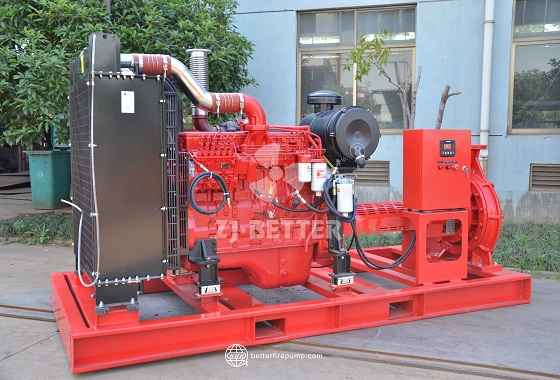
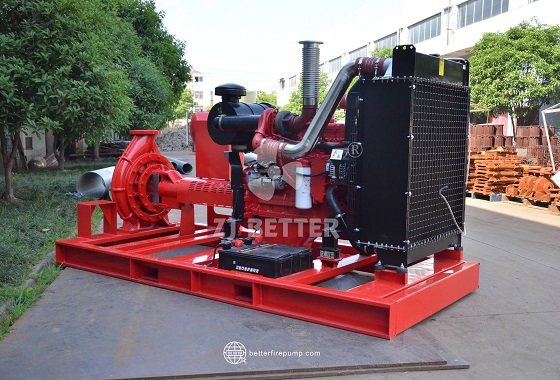
A diesel fire pump set is a stationary fire water supply system powered by a diesel engine; it is suitable for applications requiring high continuity of water supply, such as industrial plants, logistics warehouses, petrochemical facilities, power plants, docks, and large-scale buildings. The equipment shown features a diesel engine coupled with a fire pump, along with a large radiator, fuel system, and control components, all mounted on a common base to form a complete diesel fire pump unit. The diesel engine provides independent mechanical power to the fire pump, enabling operation during external power failures or when backup power is required, making it ideal for projects demanding high reliability in fire water supply. According to official specifications, these units can be configured with various pump types—such as single-stage, horizontal split-case, end-suction, or multi-stage pumps—tailored to specific flow rate, head, and pressure requirements; flow rates range from 30 to 9,000 GPM and discharge pressures from approximately 3 to 20 bar, with exact parameters determined by project design needs. The large radiator is crucial for sustained operation, as diesel engines generate significant heat; an efficient radiator combined with a circulating cooling system dissipates this heat to maintain optimal engine temperatures, thereby minimizing the risk of performance degradation due to overheating. Technical documentation indicates that a well-designed cooling system ensures stable power output even in high-temperature environments or during prolonged continuous operation, providing the necessary foundation for reliable, uninterrupted fire water supply. In addition to the cooling system, the unit relies on integrated fuel, lubrication, and exhaust systems to ensure stable engine performance. Proper matching of the engine and pump meets operational requirements for both startup and design-load conditions, while the diesel engine’s high torque output effectively handles the power demands during the pump’s startup phase. Regarding hydraulic performance, the fire pump converts the mechanical energy supplied by the engine into fluid pressure energy via impeller rotation, facilitating the transfer of water from the source to the piping network, with flow and head specifications selected to suit specific project requirements. For large-scale fire protection projects, equipment requires not only sufficient instantaneous water supply capacity but also stable operation during emergencies; consequently, the material quality and manufacturing precision of critical components—such as the pump casing, impeller, bearings, mechanical seals, and couplings—significantly influence long-term performance. Data indicates that the use of high-strength, wear-resistant materials combined with precision machining minimizes component wear during extended operation, thereby enhancing equipment durability. The equipment utilizes an integrated base mounting design that consolidates the diesel engine, fire pump, and related components; this facilitates transportation, positioning, and on-site installation while ensuring an optimal connection between the power system and the pump unit. Depending on specific project requirements, a control cabinet can be configured to manage the startup, operational status, and parameters of the diesel fire pump; features such as pressure monitoring, fault alarms, and protective functions further enhance the convenience of equipment operation and management. Overall, through the coordinated operation of the diesel engine, large-scale radiator, fuel system, lubrication system, and hydraulic pump system, the diesel fire pump unit meets flow rate and head requirements for fire suppression while ensuring the power stability and temperature control necessary for prolonged operation. For large-scale industrial and architectural projects requiring continuous fire water supply, the diesel engine power, pump flow rate, head, pipe diameter, and control method can be precisely matched to actual design parameters; this ensures the equipment is well-suited to the specific project environment and provides reliable power support for emergency fire water supply.