Packaged Horizontal Fire Water Pump Equipment – Electric Drive Solution for Fixed Fire Protection Networks
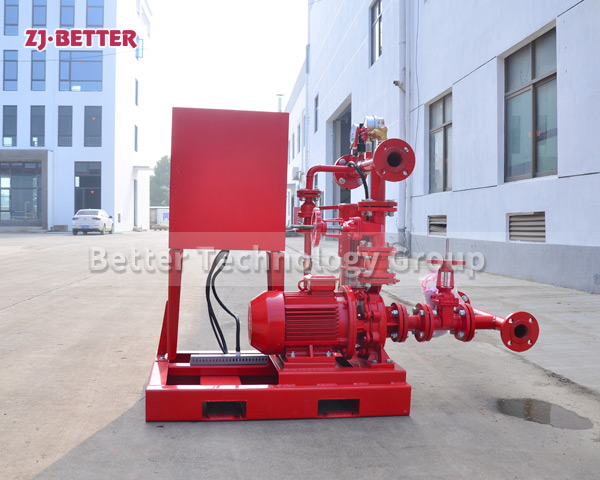
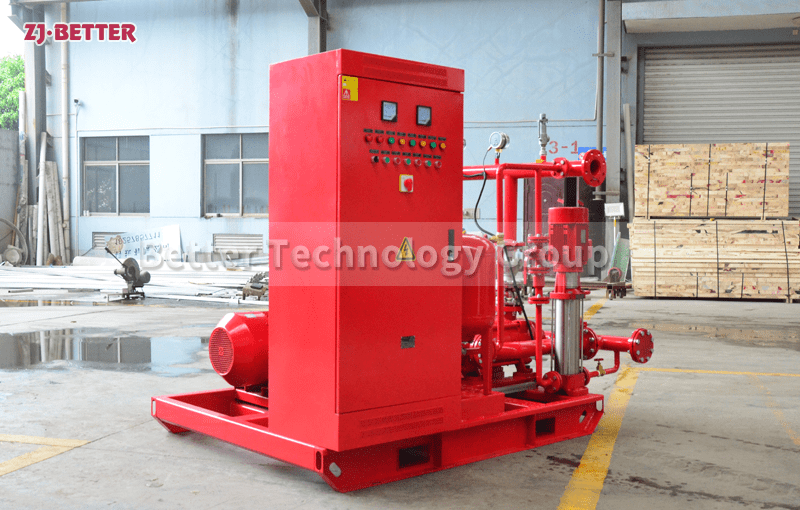
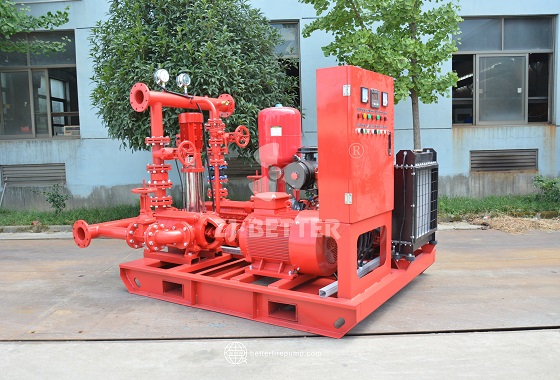
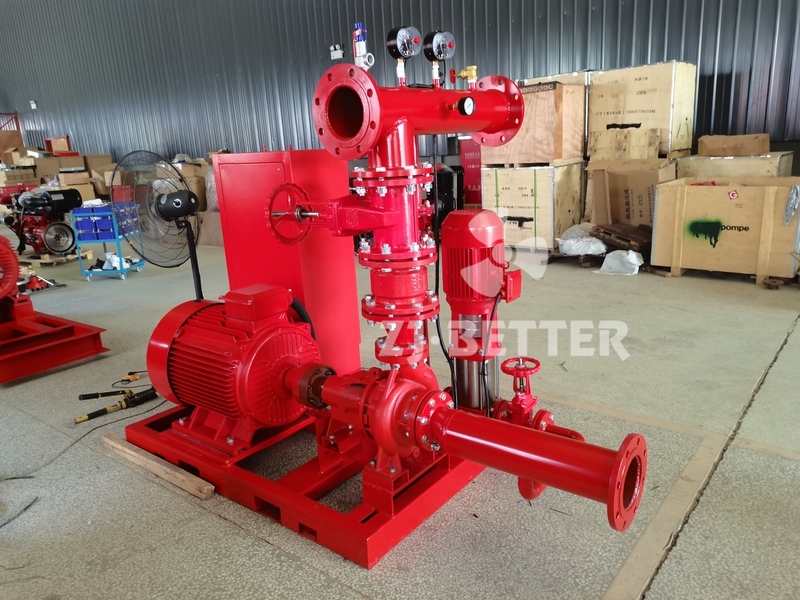
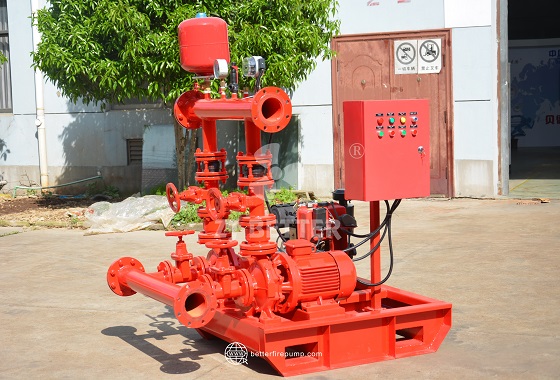
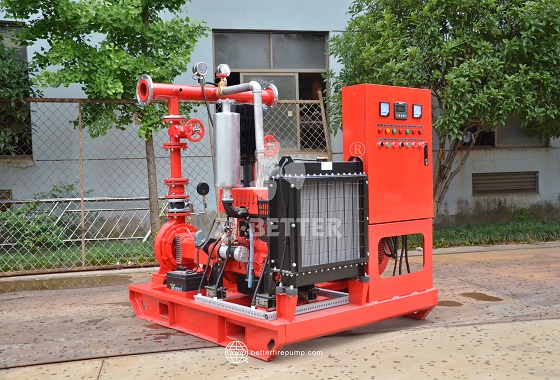
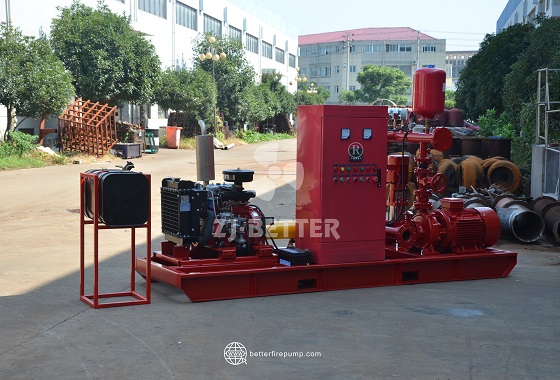
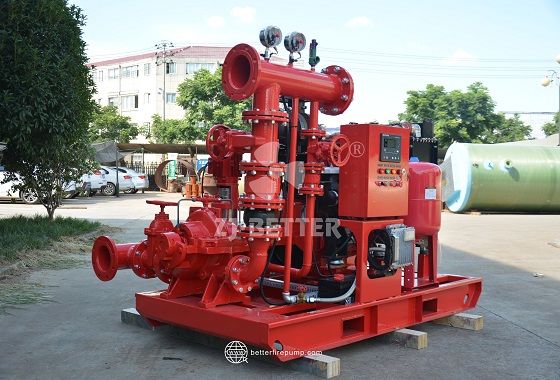
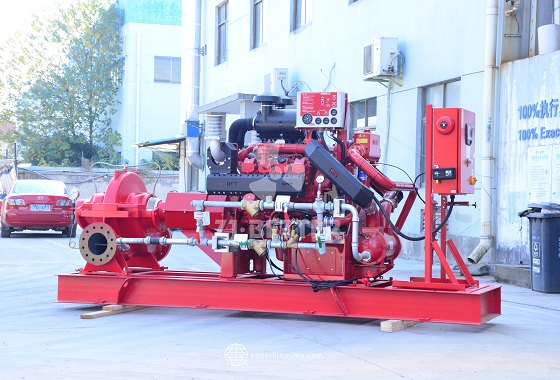
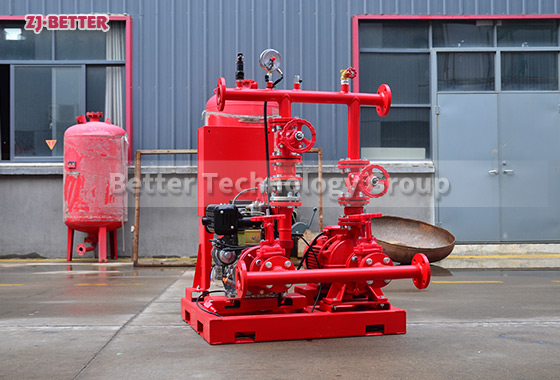
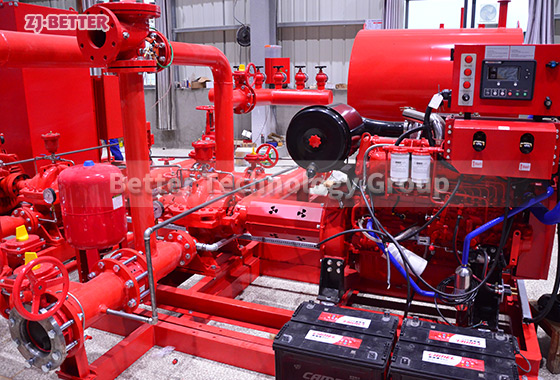
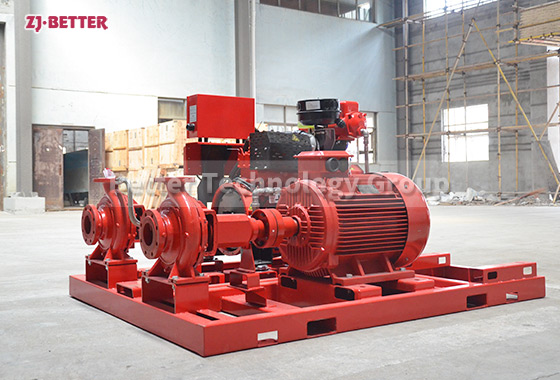
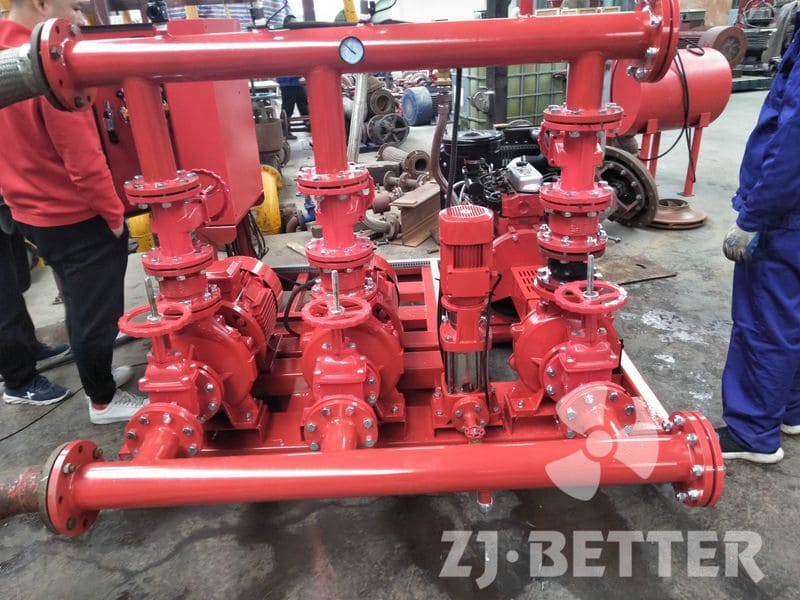
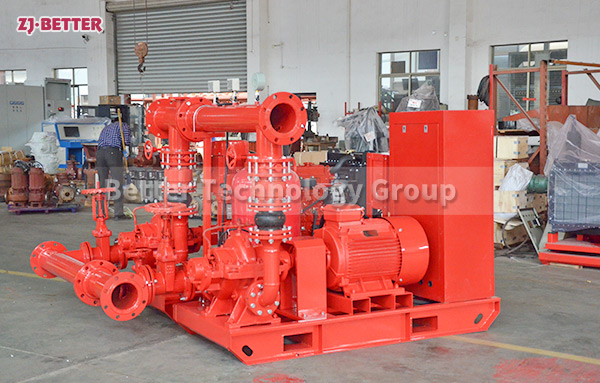
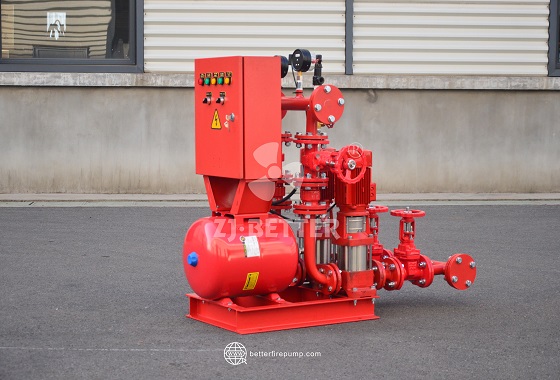
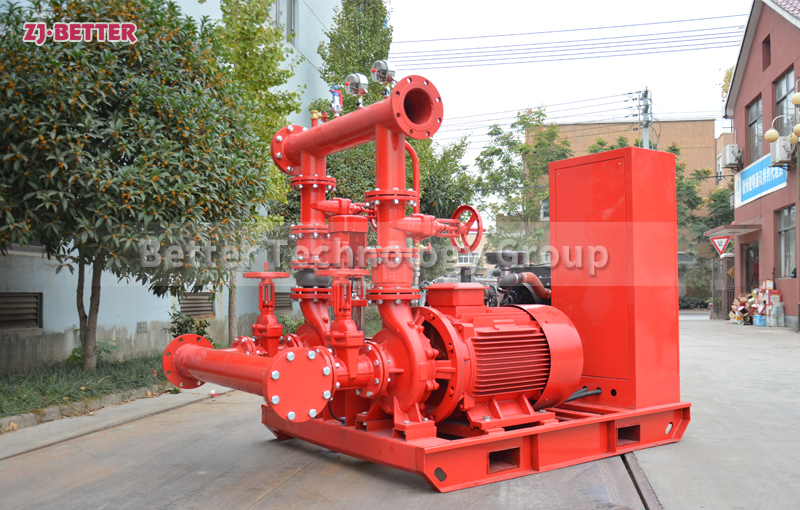
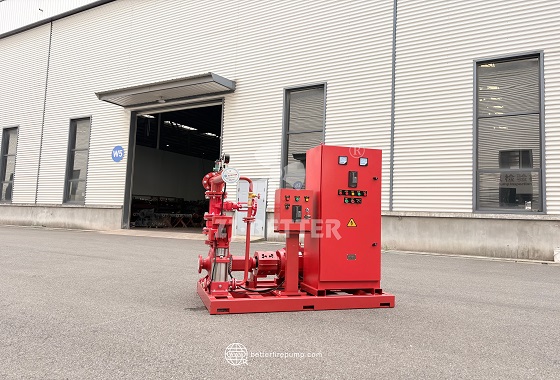
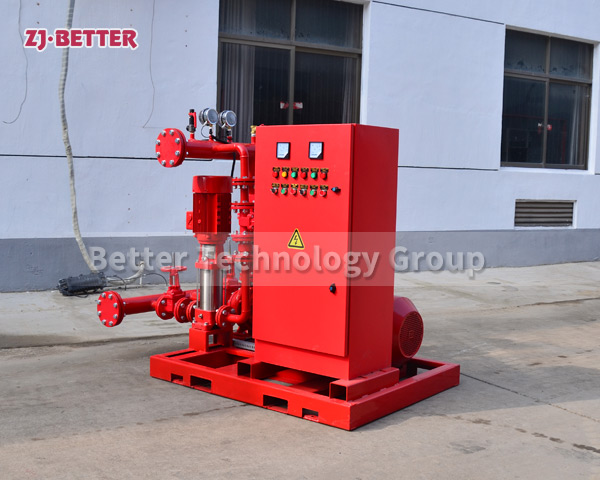
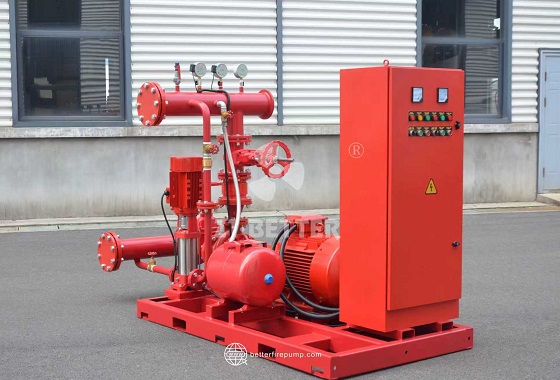
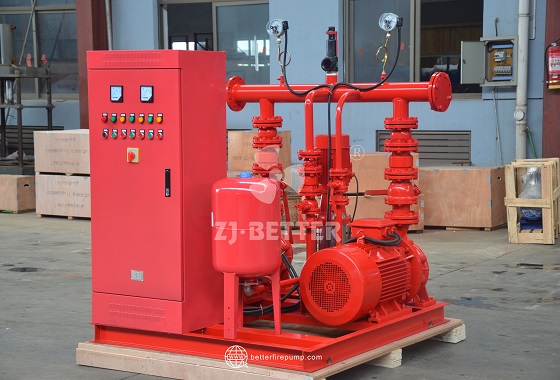
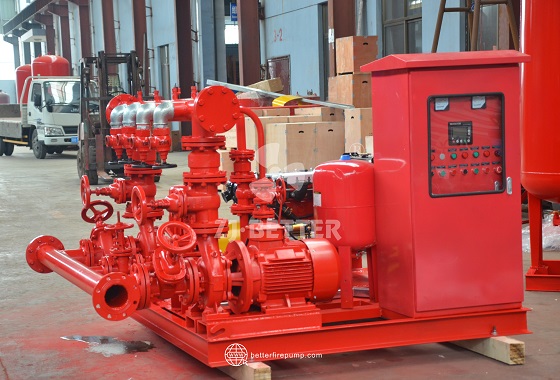
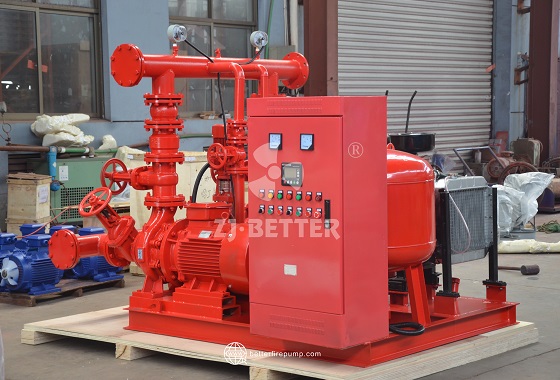
This complete horizontal fire-fighting pump system is driven by an electric motor and integrates a horizontal centrifugal pump, a control cabinet, a pressure tank, and piping accessories. It features a compact design, convenient installation, and flexible configuration, making it suitable for water supply systems in industrial buildings and fixed fire-fighting piping networks.
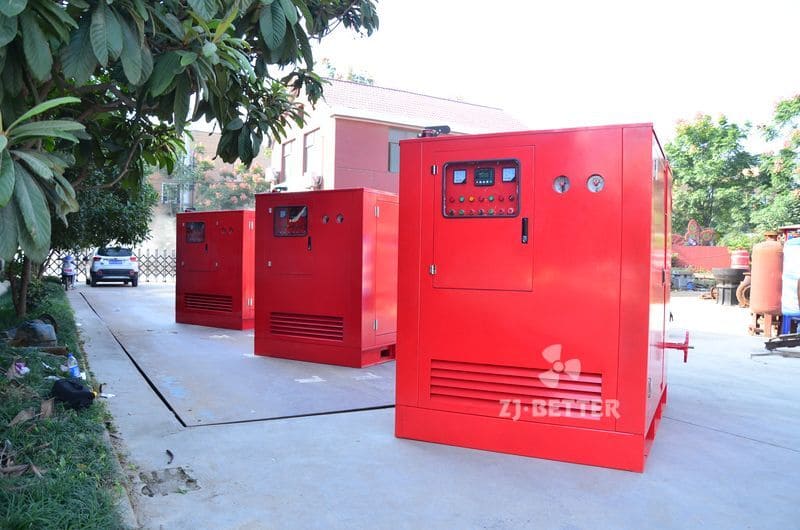
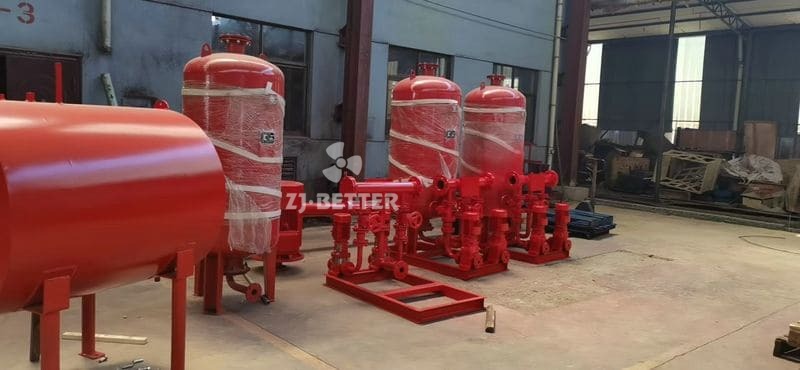
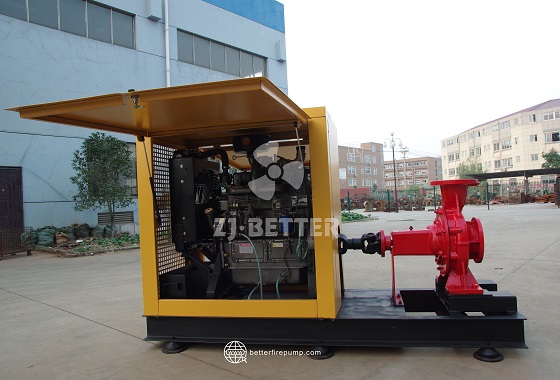
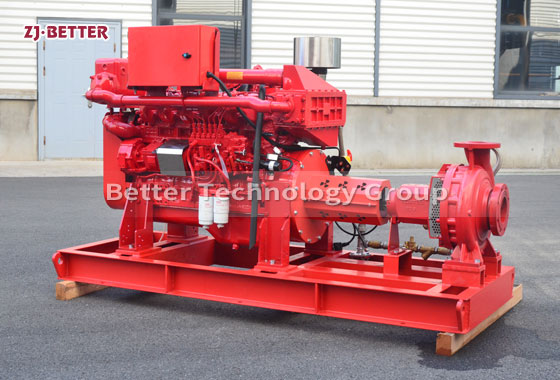
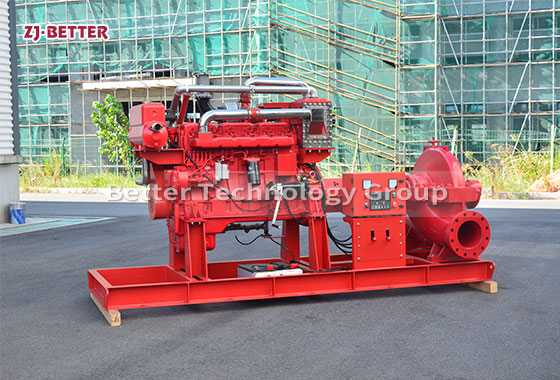
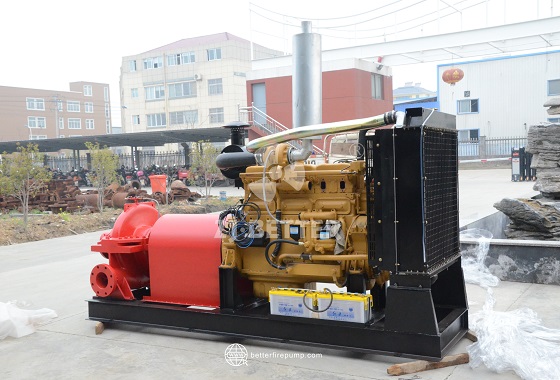
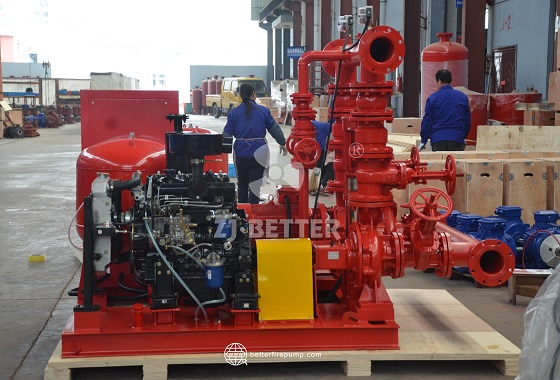
A horizontal fire-fighting pump set is a water supply system designed for fixed fire-protection piping networks, powered by an electric motor. It primarily consists of a horizontal centrifugal fire pump, an electric motor, a common base, a control cabinet, a pressure tank, pressure gauges, and associated piping accessories. By mounting the pump, the drive unit, and auxiliary components onto a single common base, the equipment forms an integrated, self-contained water supply unit. It is suitable for industrial facilities, commercial buildings, warehouses, and other locations requiring a fixed fire-fighting water supply system. The horizontal centrifugal pump operates on a well-established centrifugal principle: the electric motor drives the rotation of an impeller, which imparts energy to the water flow, generating the necessary pressure to deliver water from the fire-fighting source into the piping network. The electric drive configuration offers a stable power supply, ease of operation, and straightforward routine maintenance, making it ideal for fixed fire-pump stations with reliable power access. The pump and motor are mounted together on a common base, which ensures overall equipment stability and facilitates transportation, foundation positioning, and on-site installation. This base-mounted layout consolidates the primary equipment, reducing the labor required for decentralized on-site installation while providing a clear, organized space for piping connections and future maintenance. The accompanying control cabinet can be configured—based on specific project requirements—to provide automatic or manual control, operational status indication, fault alarms, and essential electrical protection, allowing operators to easily monitor the system’s performance. Pressure gauges and pressure-sensing components are used to observe and monitor the pressure within the fire-protection network, providing critical data for operational management. The included pressure tank acts as a buffer, helping to manage minor pressure fluctuations within the network during standby periods; if the system also incorporates a jockey pump (pressure-maintenance pump), the control logic can maintain the network’s standby pressure, thereby preventing the main fire pump from starting up frequently due to minor pressure variations. The equipment’s inlet and outlet piping, valves, and flange connections can be tailored to match on-site pipe specifications and installation requirements, ensuring an efficient and proper connection between the pump unit and the fixed fire-protection piping network. In practical applications, the flow rate, head, operating pressure, and motor power of a fire pump must be selected in accordance with fire protection design requirements. These parameters are determined by considering factors such as water source conditions, pipeline resistance, and system operating parameters, ensuring that the equipment functions within an optimal performance range. Compared to procuring and installing individual components separately on-site, a packaged configuration facilitates standardized equipment selection, factory pre-assembly, and pre-shipment inspection, while also streamlining on-site installation and commissioning. Before the equipment is put into service, it is essential to complete foundation anchoring, electrical wiring, piping connections, verification of valve positions, and testing of control functions. Furthermore, the system must undergo operational checks and regular maintenance in compliance with relevant fire safety standards. Featuring a stable horizontal centrifugal pump design, an electric motor drive, and an integrated assembly—complete with a common base and auxiliary components—this equipment meets the configuration requirements for fire pumps in fixed fire-fighting piping networks. It provides an organized, easy-to-install, and flexibly configured electric water supply solution for industrial and building fire protection systems.