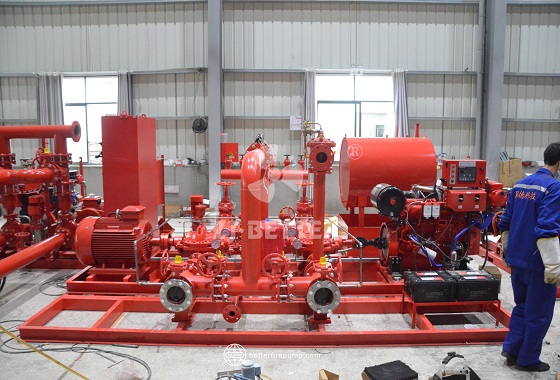
Heavy Duty Industrial Fire Pump for Continuous Firefighting Operations
Heavy-duty industrial fire pump systems have advantages such as large flow rate, high head, continuous and stable water supply, and intelligent control, and are suitable for petrochemical, power energy, and large-scale industrial fire protection projects.
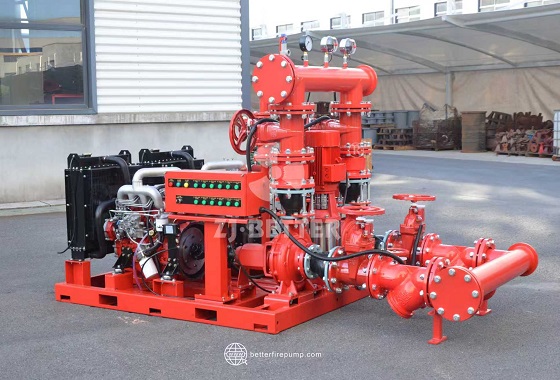
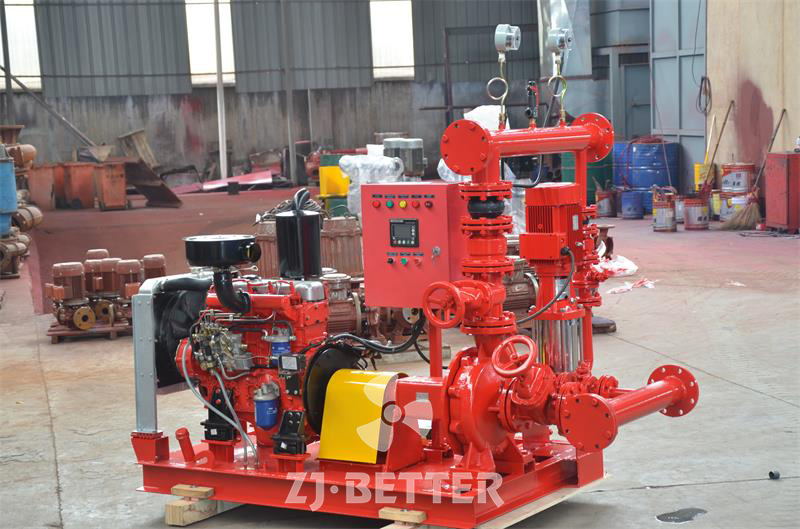
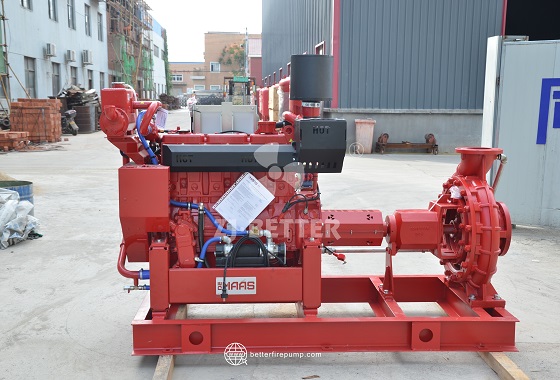
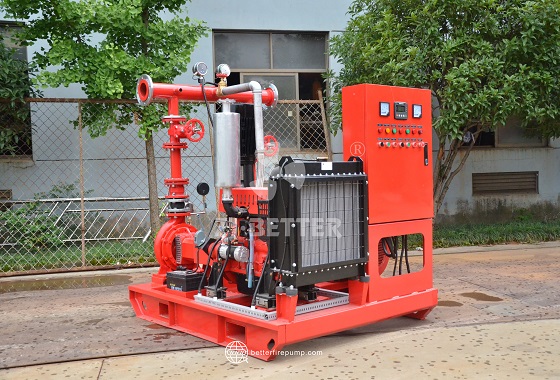
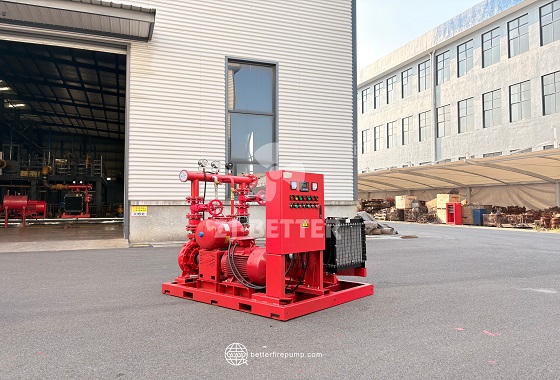
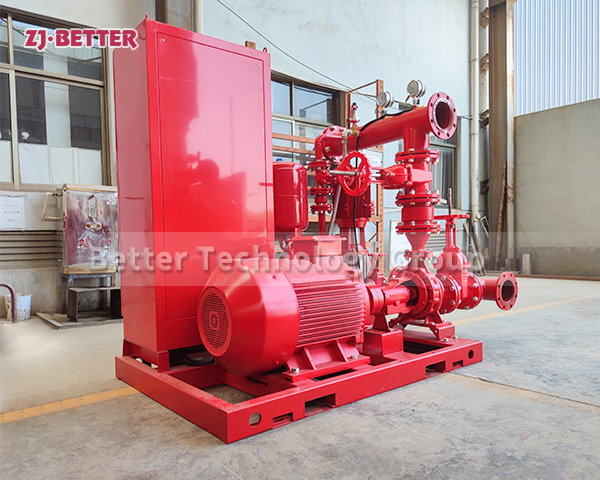
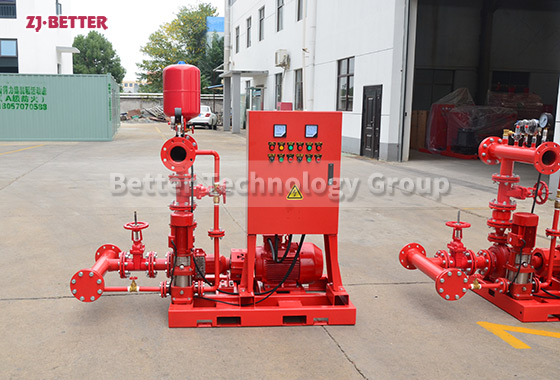
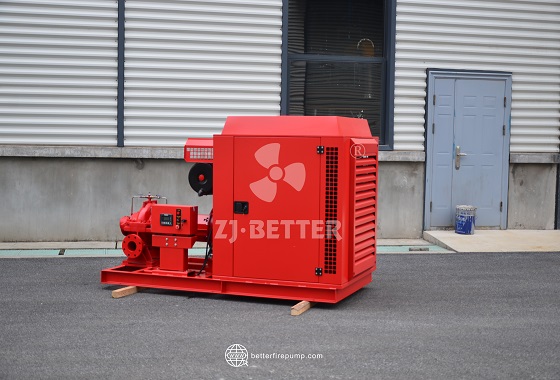
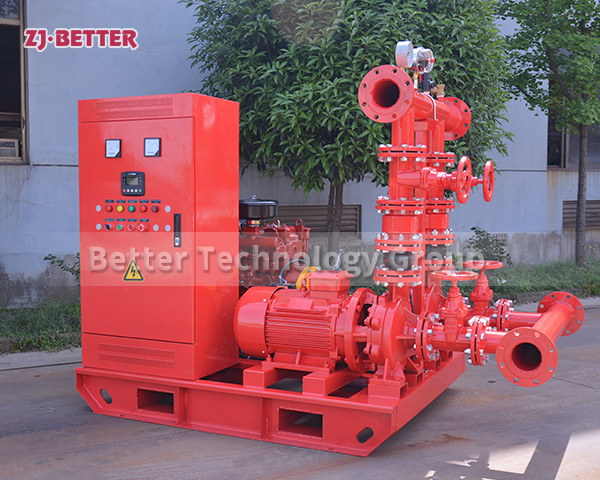
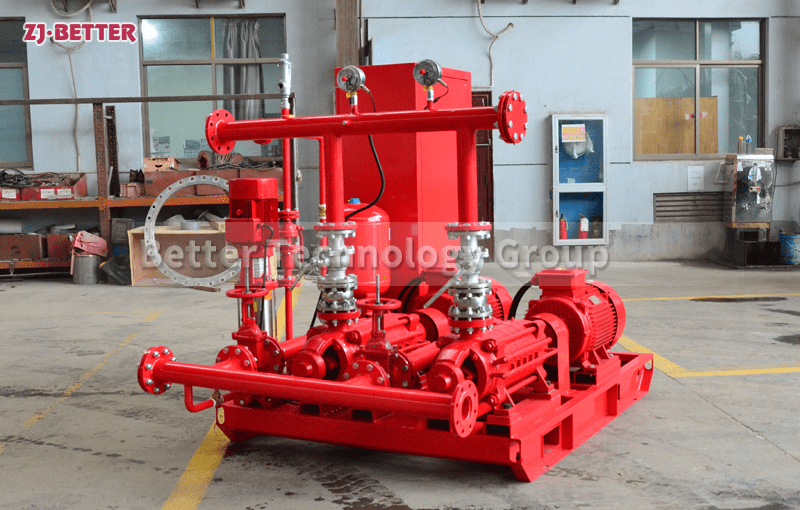
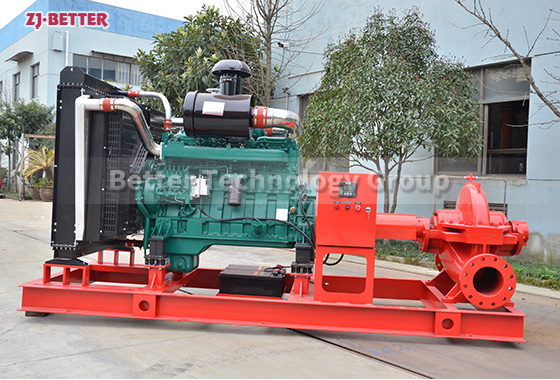
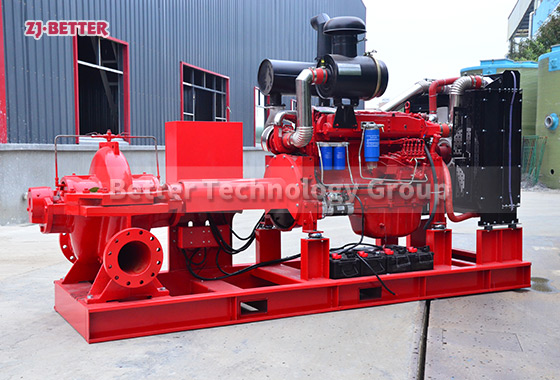
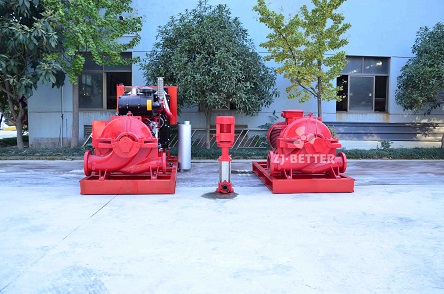
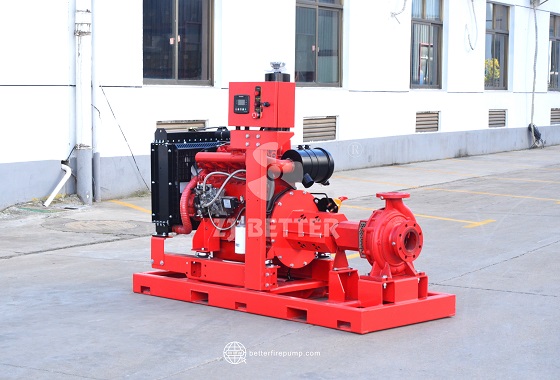
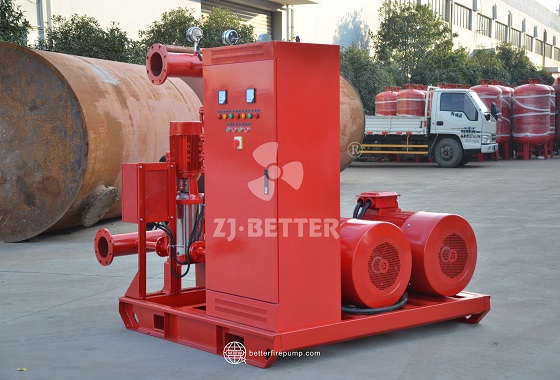
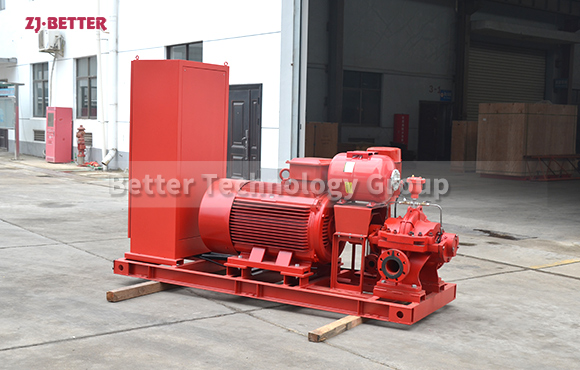
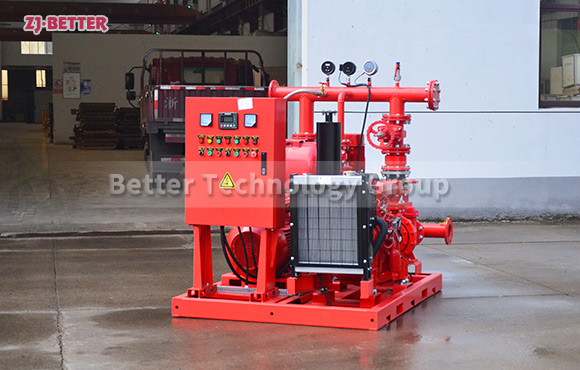
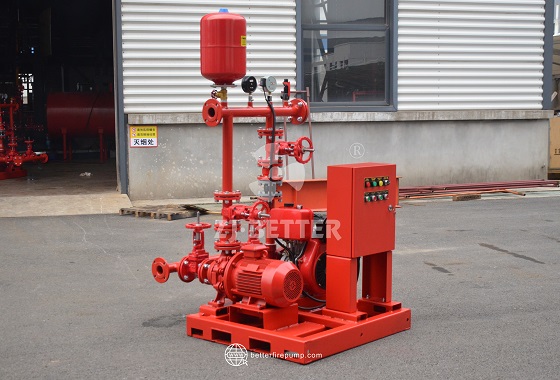
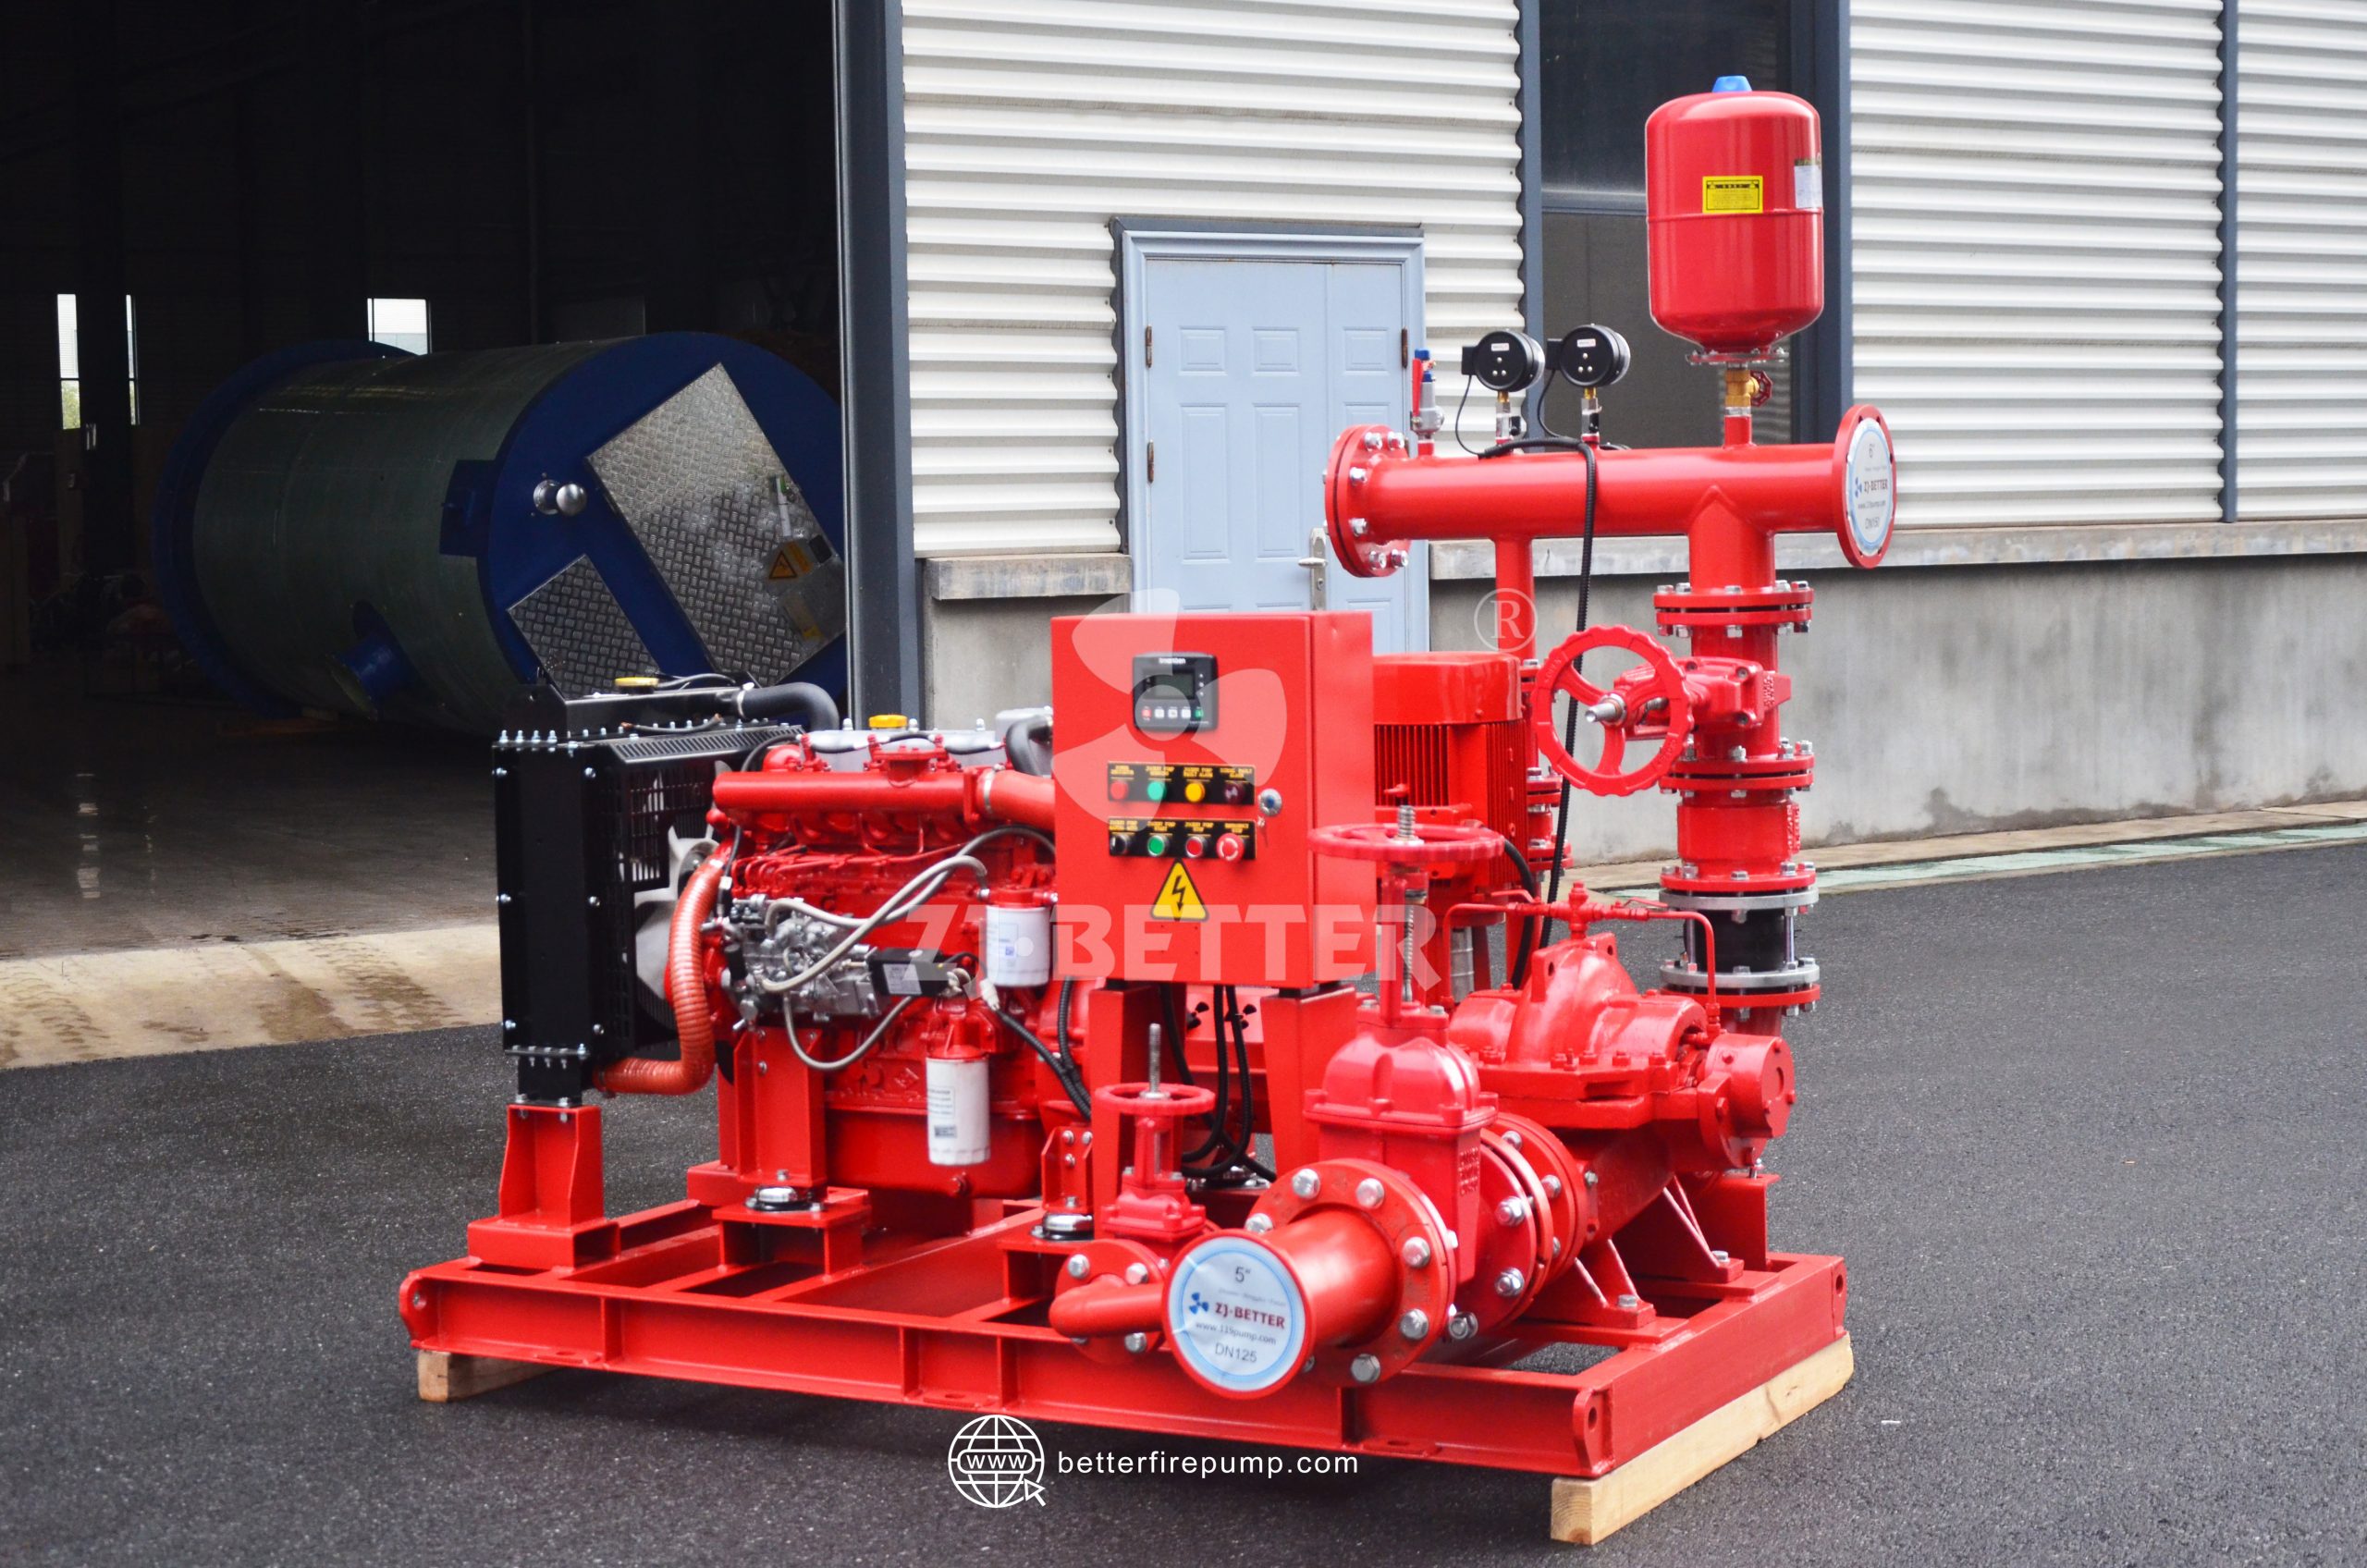
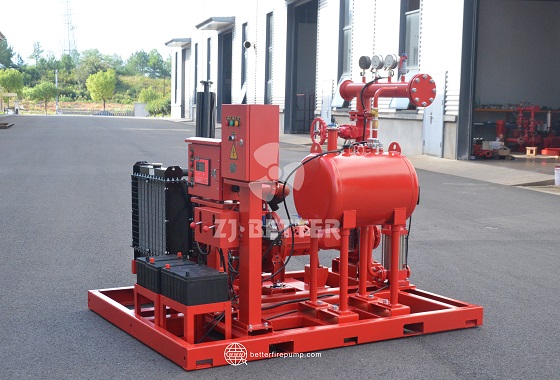
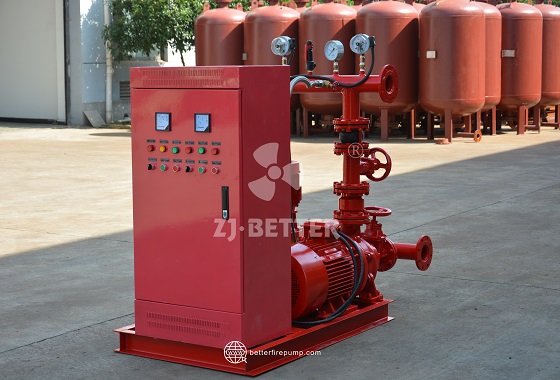
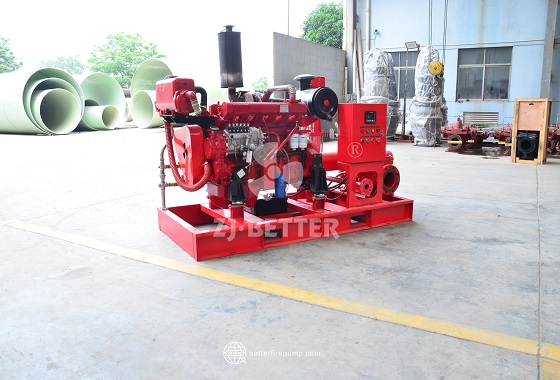
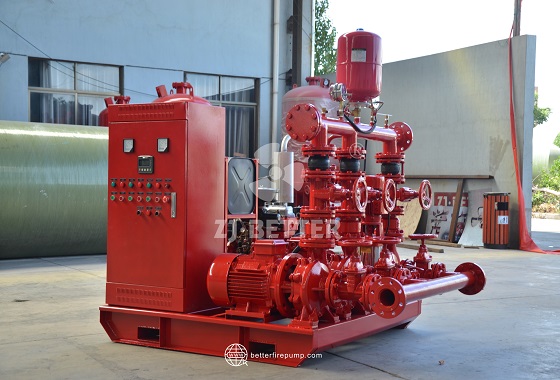
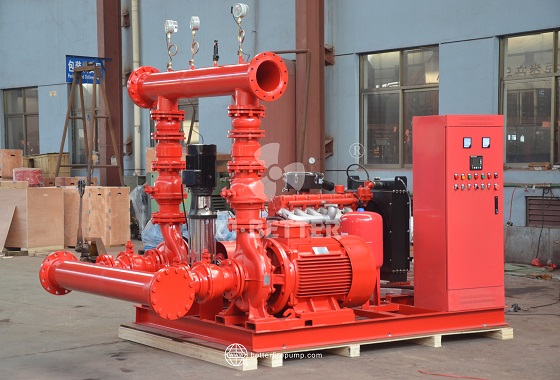
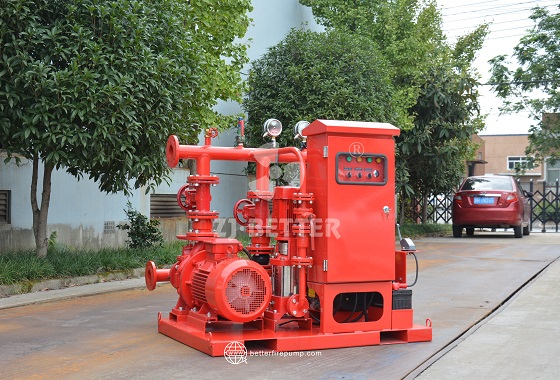
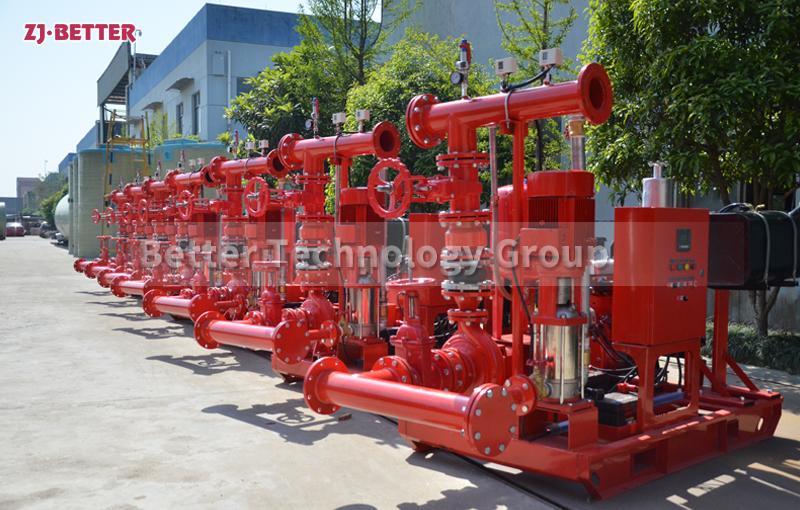
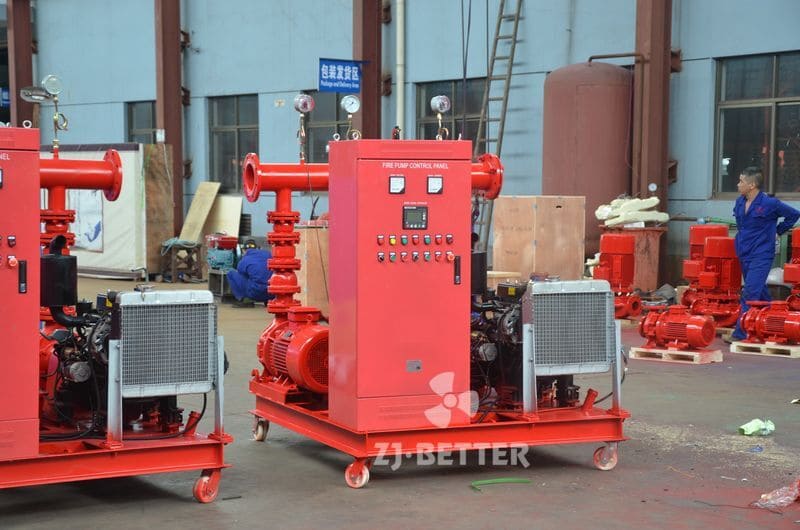
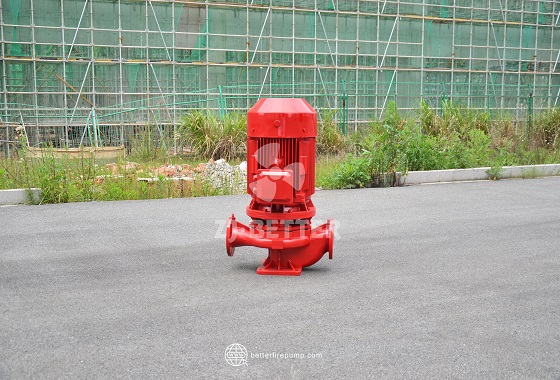
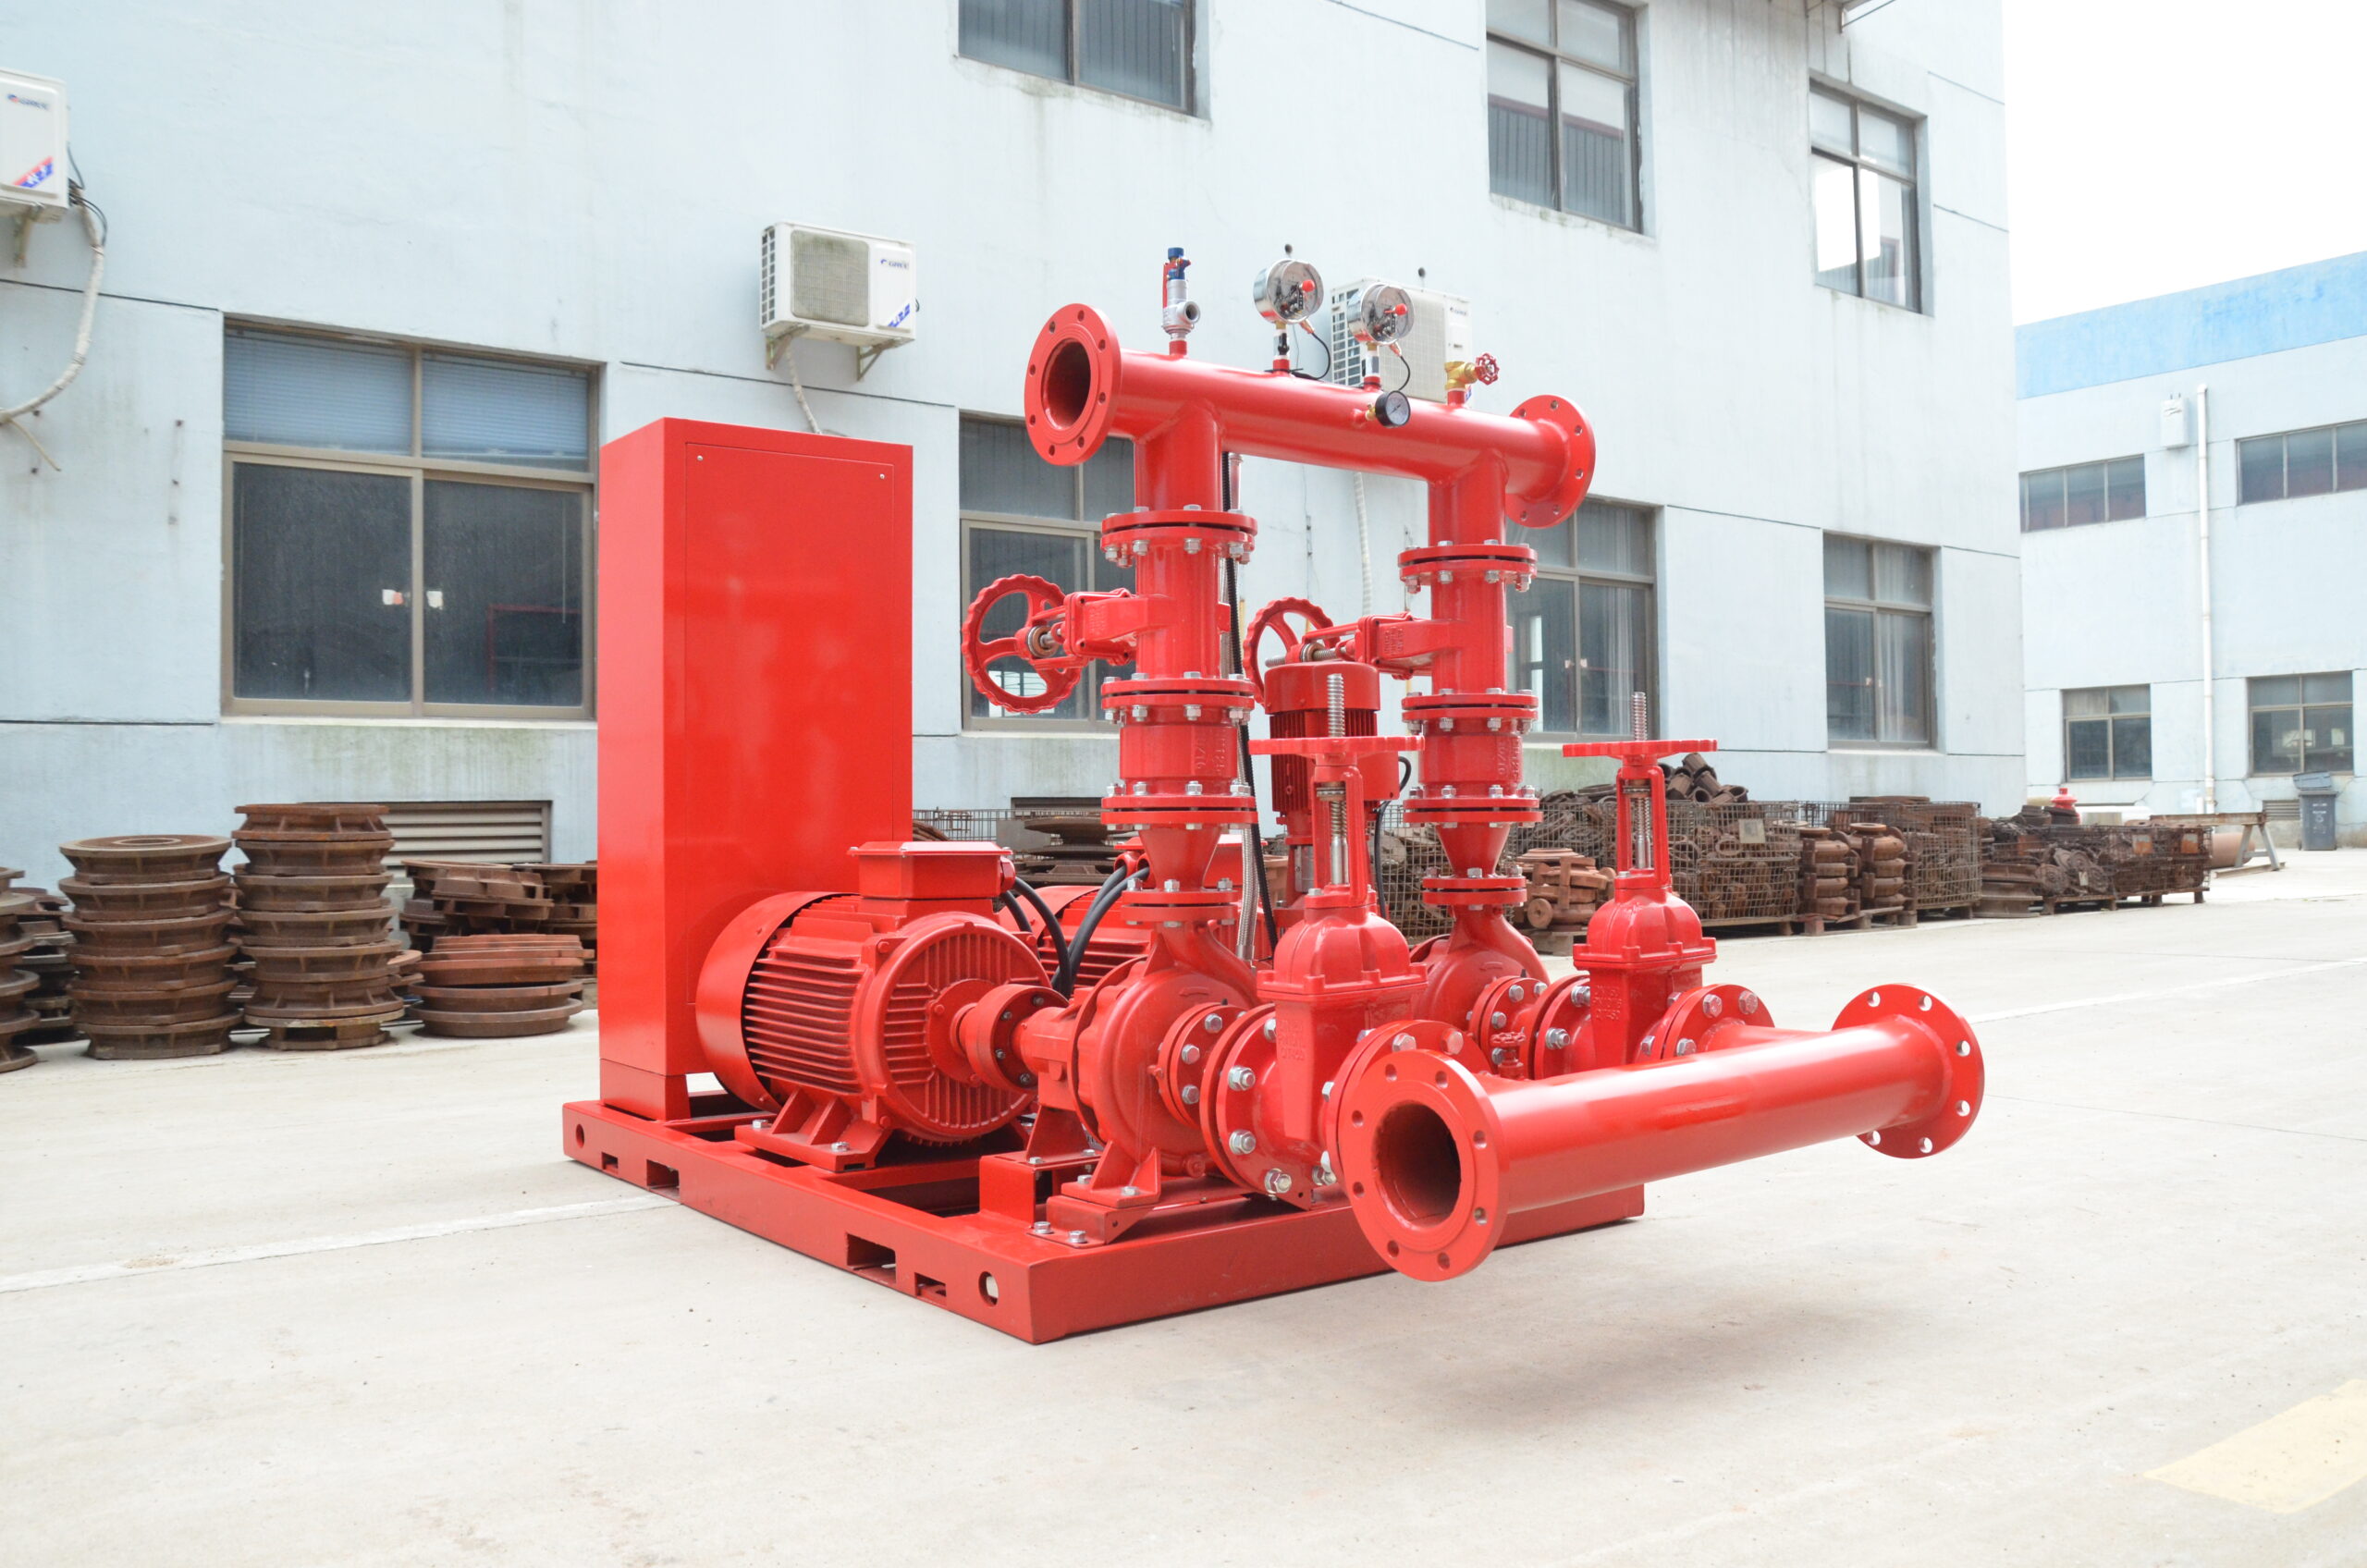
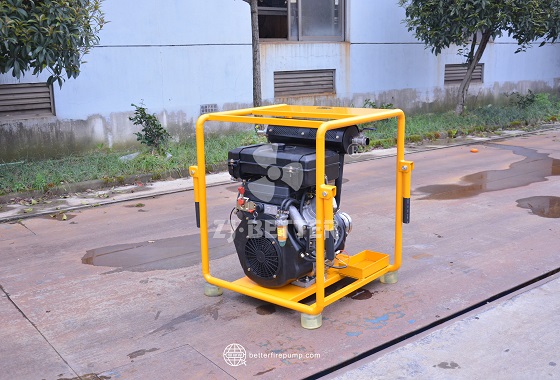
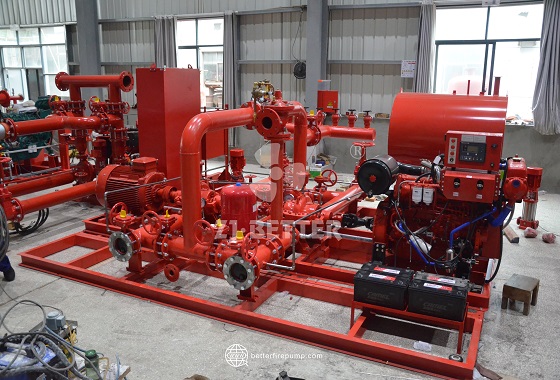
With the continuous expansion of modern industrial projects and the constant improvement of fire safety standards, industrial fire protection systems place higher demands on the stability, continuous operation capability, and high-intensity performance of fire water supply equipment. Especially in high-risk industrial settings such as petrochemicals, power energy, steel smelting, large-scale warehousing and logistics centers, and port terminals, once a fire occurs, fire-fighting equipment not only needs to quickly establish a high-pressure water supply system but must also maintain stable and reliable operation during prolonged continuous firefighting operations. Heavy-duty industrial fire pump systems are crucial fire water supply equipment widely used under these high-standard fire protection requirements. Through the comprehensive integration of high-performance power systems, high-efficiency centrifugal fire pump structures, and intelligent automatic control technology, they achieve the combined advantages of continuous and stable water supply, large-flow, high-pressure water delivery, and long-term operation in complex environments, providing safer, more efficient, and reliable fire water supply guarantees for modern industrial fire protection projects. This fire pump system adopts a heavy-duty structural design, with the entire equipment mounted on a high-strength steel base, effectively withstanding the mechanical pressure and vibration generated by long-term high-load operation. Compared to ordinary fire pump equipment, its structure is more robust and durable, making it particularly suitable for long-term continuous operation and high-intensity fire-fighting environments. In large-scale industrial projects, fire-fighting equipment often needs to be on standby for extended periods and rapidly enter high-intensity operation mode in the event of a fire. Therefore, the overall structural reliability of the equipment is paramount. Heavy-duty industrial fire pump systems significantly improve long-term operational stability and service life through reinforced frame design and the use of durable materials. Regarding the power system, the equipment can be configured with a high-performance diesel engine or an industrial-grade electric motor system to meet different project requirements. The diesel power option possesses complete independent operation capability, ensuring a continuous and stable water supply even in the event of a power outage or power system failure, thus ensuring the normal operation of the fire-fighting system in critical moments. The diesel engine is professionally optimized to maintain stable speed and continuous power output under high temperature, high load, and long-term operating conditions, while effectively reducing fuel consumption and improving overall operating economy. In terms of water supply performance, the heavy-duty industrial fire pump system adopts a high-efficiency centrifugal fire pump structure. Through optimized impeller design, pump casing flow channels, and internal hydraulic balance system, the equipment can achieve high flow rate, high head, and stable pressure output. The system not only meets the stringent requirements of large-scale fire-fighting networks for high-pressure water supply but also enables continuous long-distance water delivery, providing a stable water source for sprinkler systems, fire hydrant systems, and fire monitors. In large-scale industrial fire suppression, a stable and continuous water supply is directly related to fire extinguishing efficiency and fire control effectiveness. This equipment, with its excellent water supply performance, can maintain stable operation for extended periods in complex fire-fighting scenarios. To meet the demands of complex industrial environments, key components are manufactured using high-strength, wear-resistant, and corrosion-resistant materials, including reinforced pump shafts, stainless steel impellers, high-temperature bearings, and high-performance mechanical seals. This durable design effectively resists mechanical wear and corrosion during long-term operation, maintaining stable performance even in humid, high-temperature, dusty, or chemically corrosive environments, thereby reducing equipment failure rates and subsequent maintenance costs. Regarding cooling and heat dissipation, the equipment is equipped with a high-efficiency cooling system and a large-capacity heat dissipation structure, effectively controlling the operating temperature of the power system and ensuring stable operation during prolonged continuous fire suppression. Even under high-temperature conditions in summer or prolonged high-load operation, the system effectively avoids power loss or equipment shutdown due to overheating, thus improving the overall reliability of the fire protection system. The intelligent automatic control system is a crucial component of this equipment. The system can monitor key parameters such as engine speed, water pressure, oil pressure, temperature, and operating status in real time, and automatically adjust the equipment’s operating status according to changes in the fire pipeline pressure. In the event of a fire or pressure drop, the equipment can quickly and automatically start and enter water supply mode, and automatically stop operation after the system returns to normal, thereby reducing energy waste and improving equipment management efficiency. Simultaneously, the system also features fault alarms, automatic protection, and remote monitoring functions, effectively reducing human error risks and enhancing overall operational safety. In terms of energy efficiency, the heavy-duty industrial fire pump system effectively reduces energy consumption while ensuring high-performance water supply through efficient power matching and optimized hydraulic design. Compared to traditional high-energy-consuming fire protection equipment, its long-term operating costs are lower. Furthermore, due to its long maintenance cycle and low failure rate, it can further reduce subsequent maintenance and downtime costs, improving the overall project’s economic benefits. Modular design is also one of the equipment’s key advantages. The equipment adopts an integrated modular layout, centrally mounting the power system, fire pump, control cabinet, and piping system on a unified base. This not only facilitates transportation and on-site installation but also effectively shortens the project construction cycle. Maintenance personnel can quickly complete equipment inspection, lubrication, maintenance, and parts replacement, thereby improving post-management efficiency and reducing equipment downtime. Regarding low vibration and low noise performance, the equipment employs a vibration-damping base, flexible couplings, and an optimized power transmission structure design, effectively reducing mechanical vibration and noise generated during operation. This not only improves the operating environment of the fire pump room but also reduces fatigue damage to the equipment structure caused by long-term vibration, further enhancing equipment stability and service life. In terms of application areas, heavy-duty industrial fire pump systems are widely used in petrochemical projects, power energy bases, large-scale warehousing and logistics centers, ports and docks, steel smelters, municipal fire protection projects, and high-rise building fire protection systems. In these large-scale industrial fire protection scenarios, fire protection systems often need to establish a continuous and stable high-pressure water supply capacity within a short period of time and maintain reliable operation during prolonged firefighting operations. This equipment, with its high-flow, high-lift water supply capacity, heavy-duty structural design, and intelligent control technology, can fully meet the stringent requirements of modern industrial fire protection engineering for high-standard fire water supply equipment. As global industrial safety standards continue to rise, the market demand for high-performance fire water supply equipment is also continuously increasing. The heavy-duty industrial fire pump system, through the comprehensive integration of efficient power technology, stable water supply structure, and intelligent operation management, achieves a comprehensive improvement in fire water supply efficiency, long-term operational reliability, and economy, providing a more efficient, safe, and stable fire water supply solution for the construction of modern industrial fire protection systems.