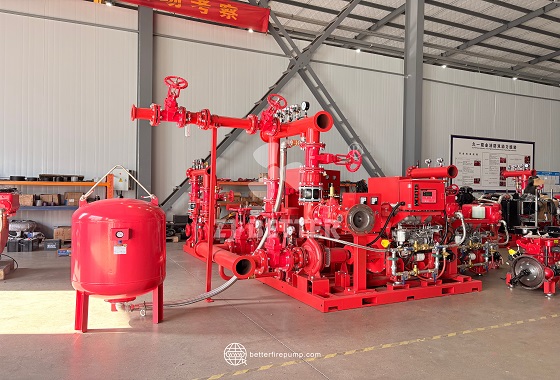
Packaged Diesel Fire Water Supply Equipment with Optimized Pump and Piping Connections
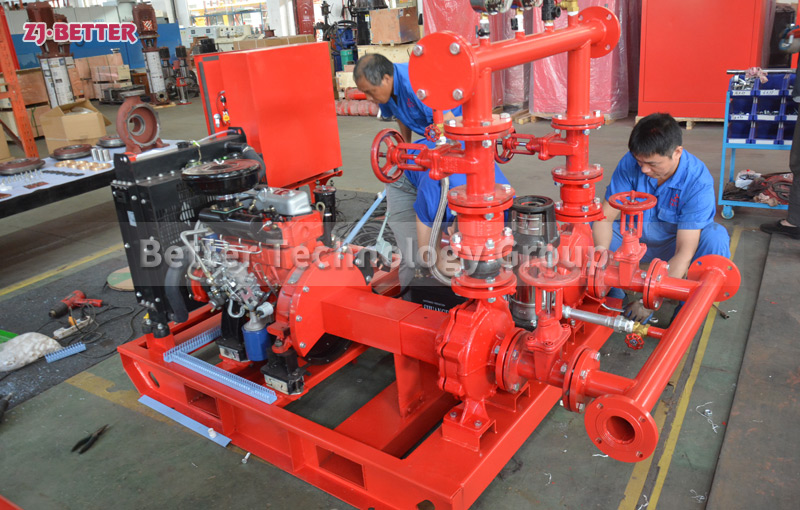
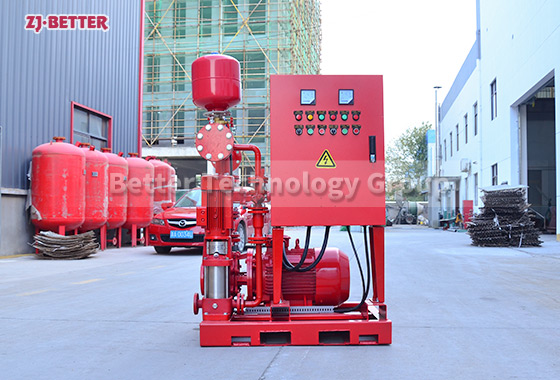
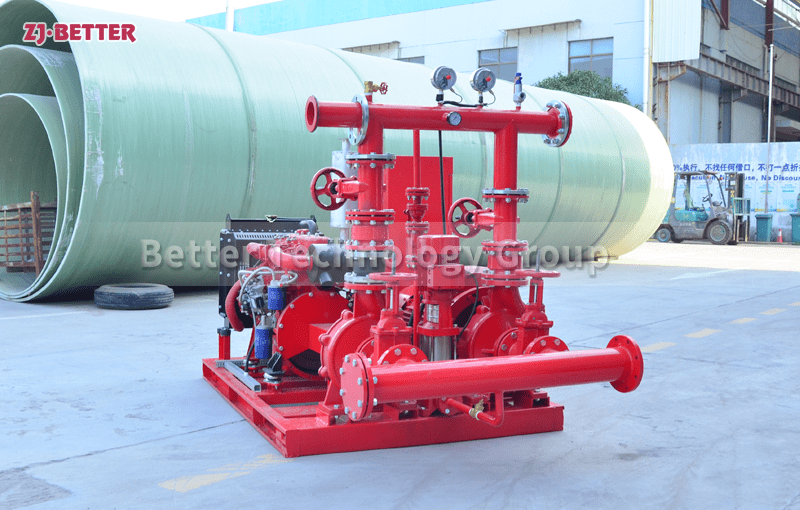
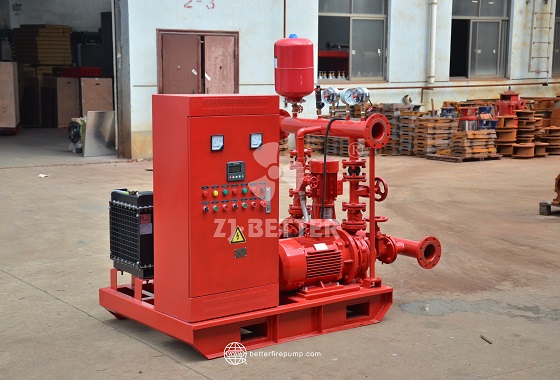
This integrated diesel fire-fighting water supply system combines a diesel engine, fire pump, control cabinet, and piping accessories; by optimizing the connection between the pump unit and the piping, it provides a stable and efficient solution for emergency fire-fighting water supply.
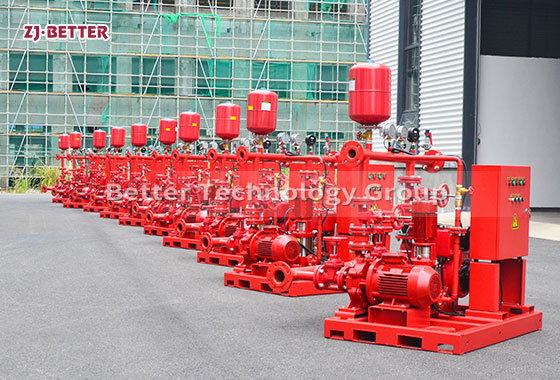
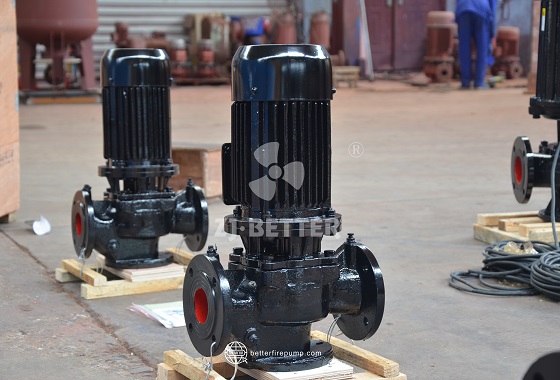
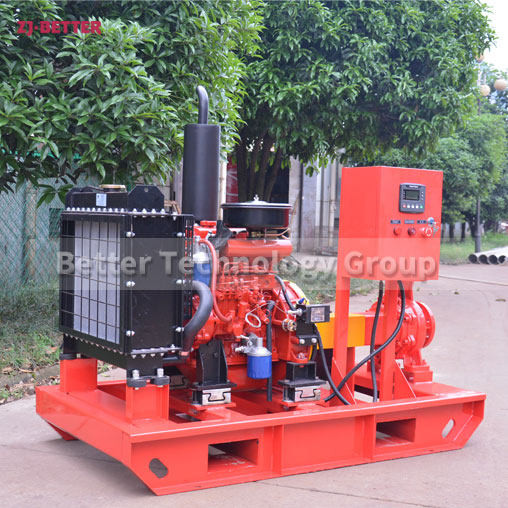
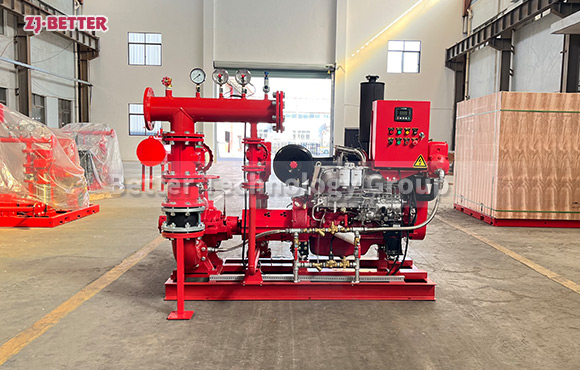
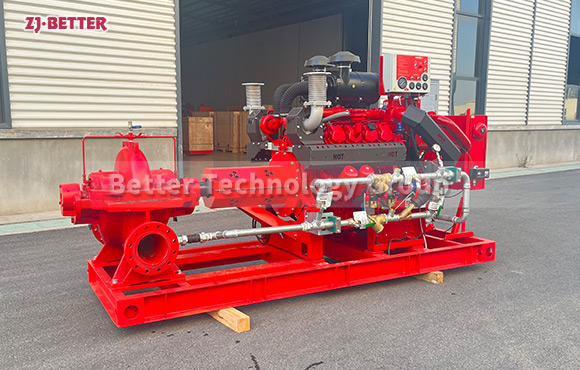
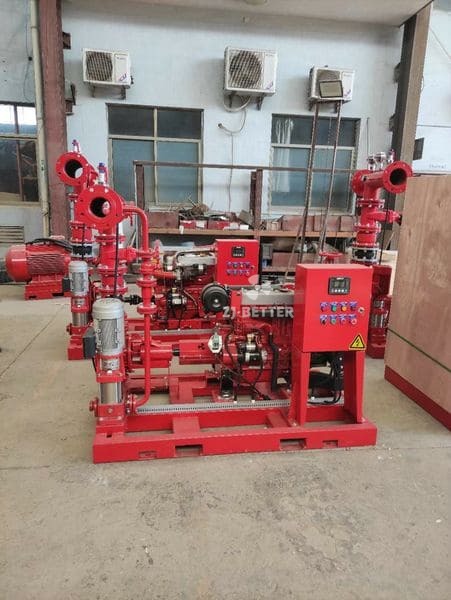
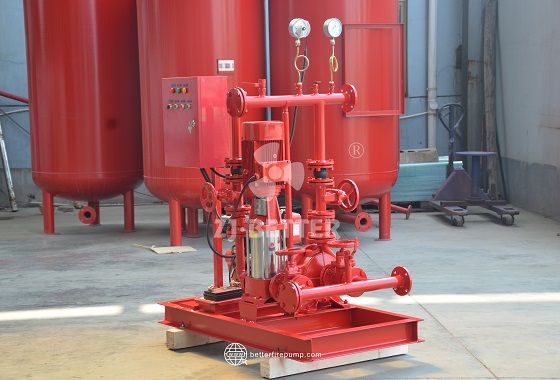
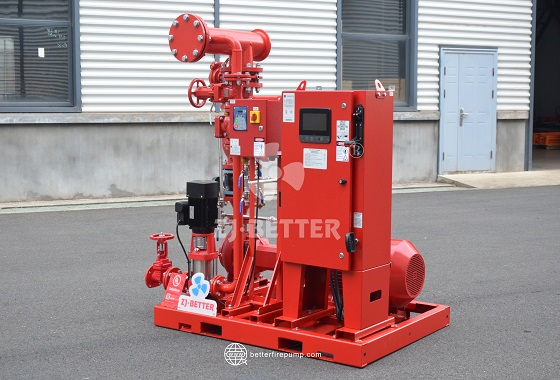
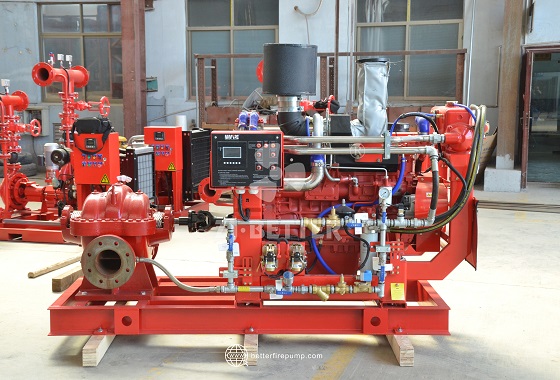
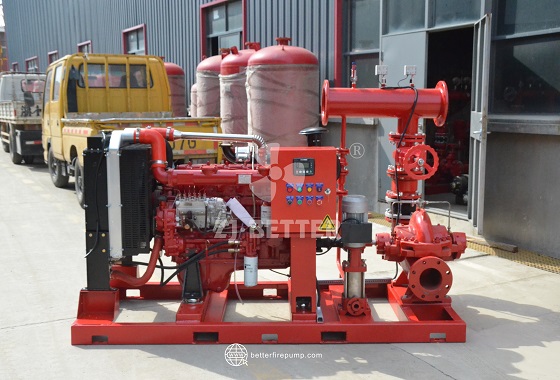
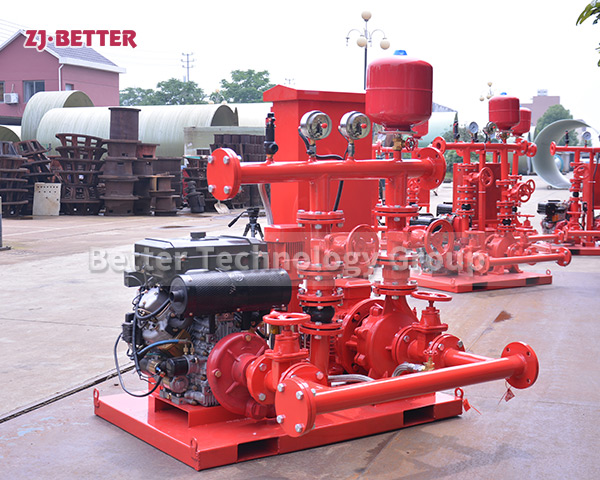
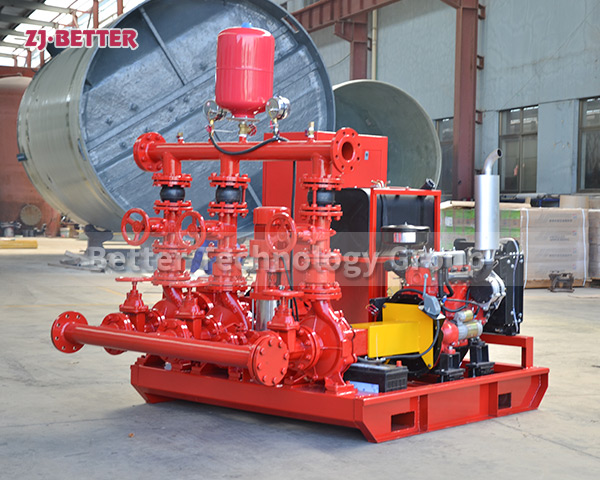
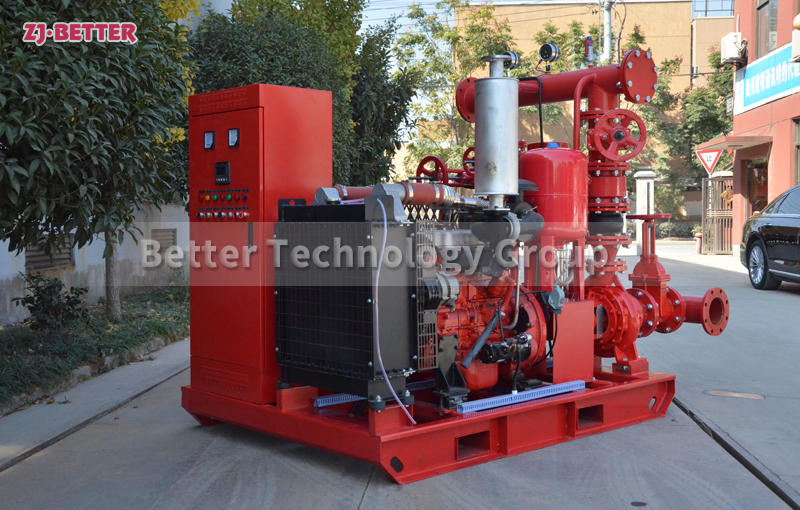
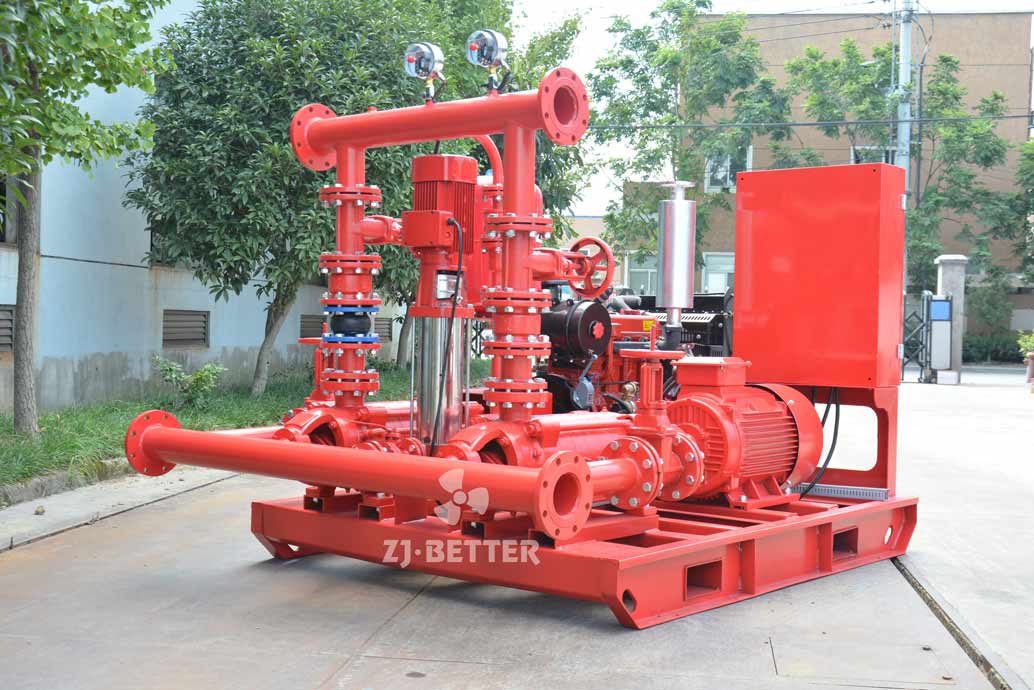
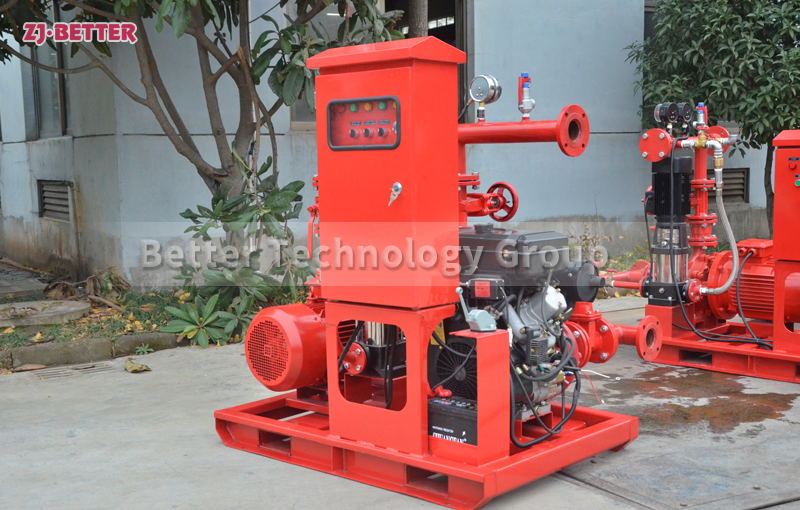
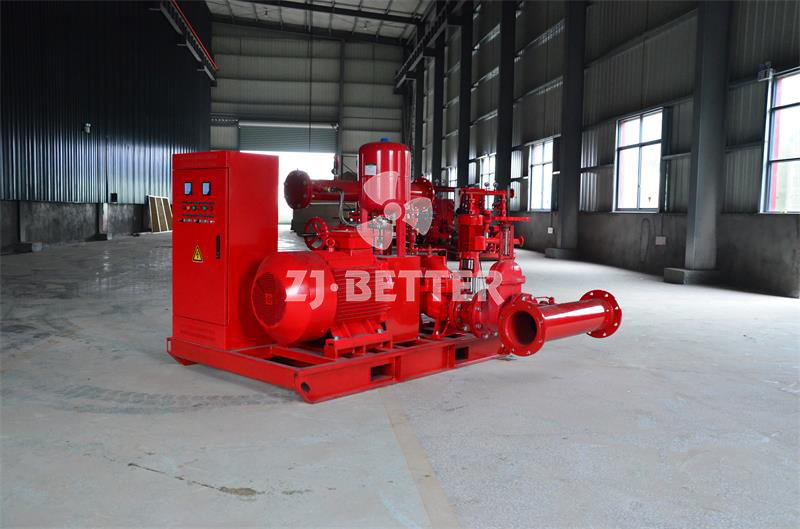
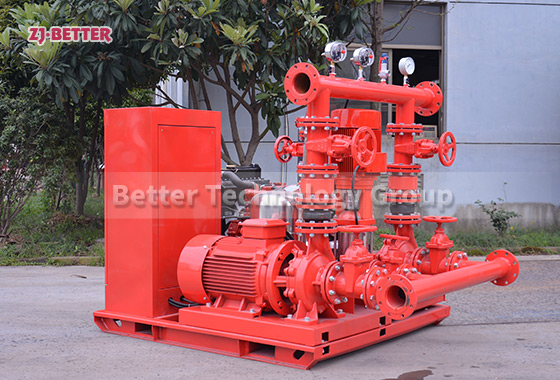
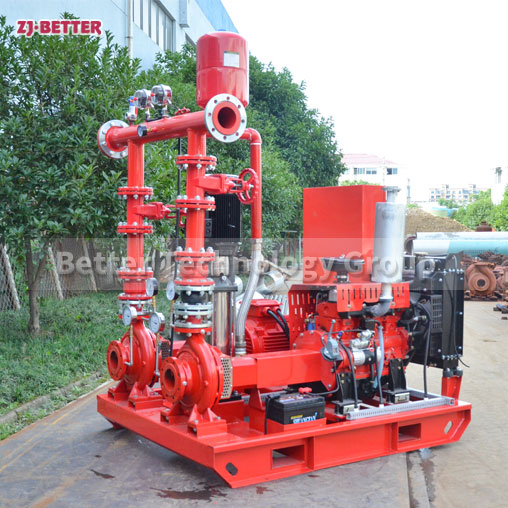
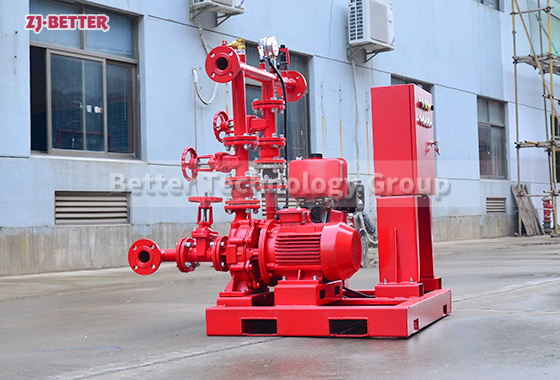
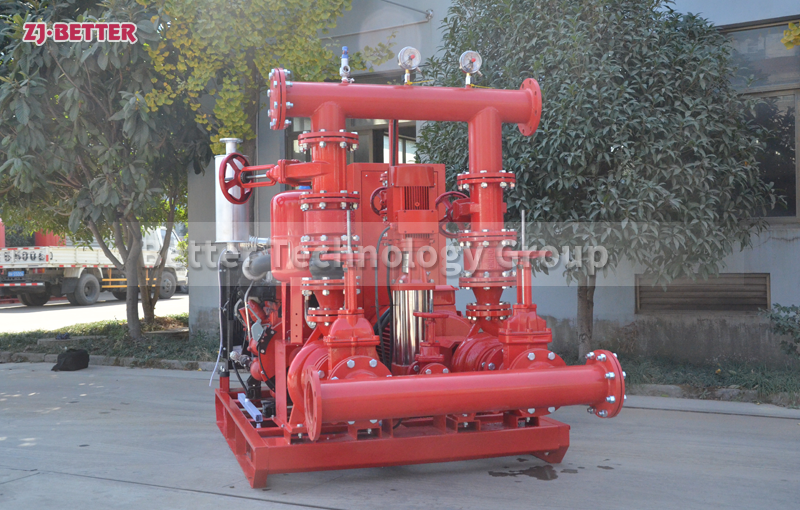
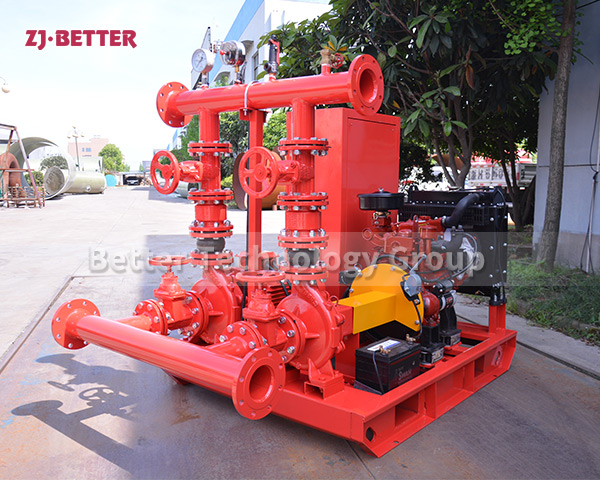
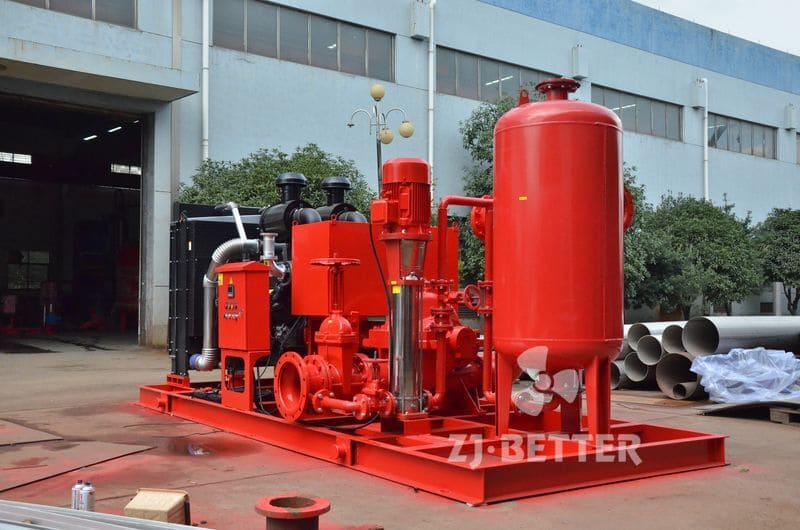
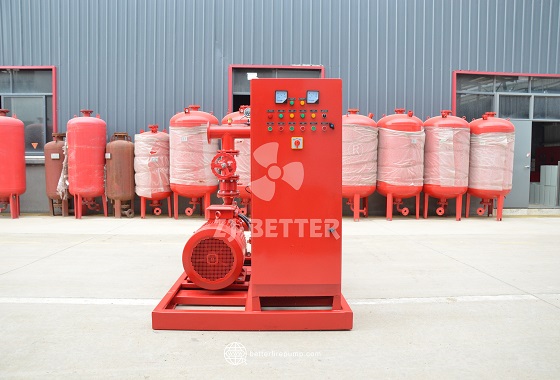
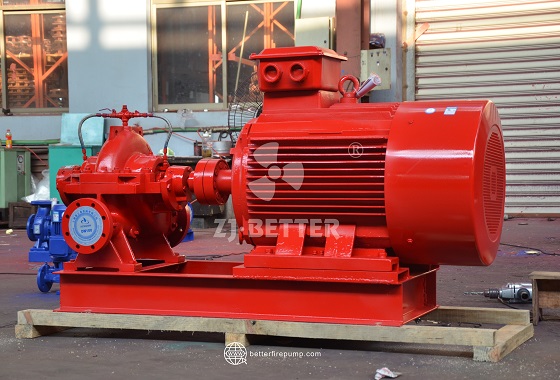
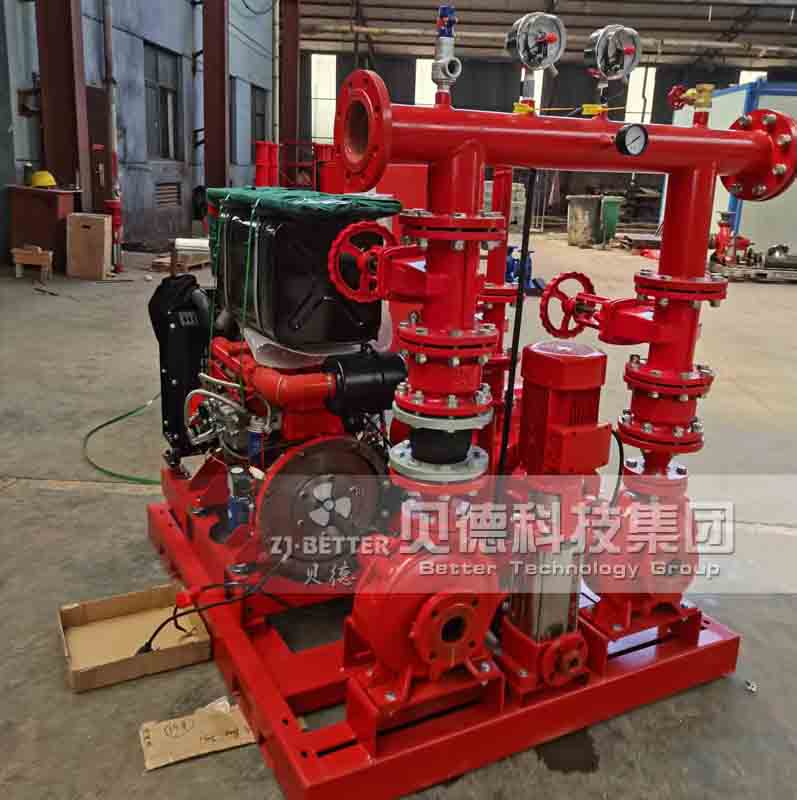
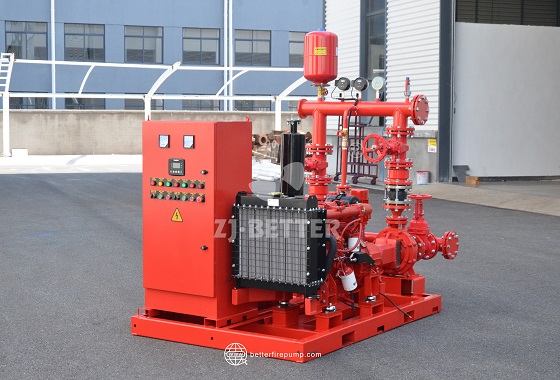
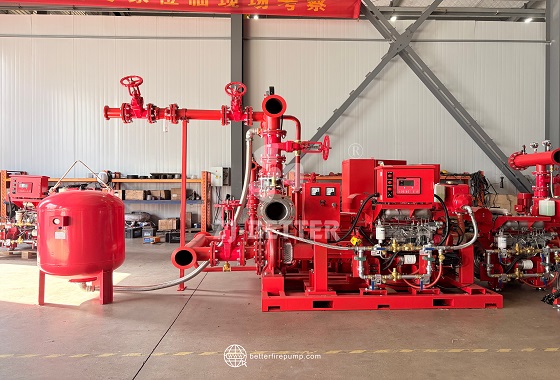
This integrated diesel fire-fighting water supply system consolidates a diesel engine, fire pump, control cabinet, pressure components, and inlet/outlet piping and valves into a single, cohesive unit. This design minimizes the need for complex on-site interconnections between separate components, making the system ideal for industrial plants, logistics warehouses, commercial buildings, docks, and other facilities requiring reliable fire-fighting water supplies. Powered by an independent diesel engine, the system provides stable mechanical drive to the main fire pump, reducing reliance on a fixed power grid. It accommodates various pump types—such as end-suction, horizontal split-case, and single- or multi-stage pumps—to meet specific flow rate, head, and piping network requirements. The system features a centralized base-frame design with an optimized layout of the pump, engine, control cabinet, and piping; this integration facilitates transport, positioning, and installation, as well as ongoing inspection and maintenance. A key feature is the optimized piping configuration—incorporating inlet and outlet pipes, valves, check valves, pressure gauges, pressure sensors, flanges, and flexible joints—which ensures a seamless connection between the pump and the fire-fighting network, reduces on-site assembly of scattered parts, and simplifies pressure monitoring and equipment status management. Depending on project specifications, the system can also include a pressure-stabilizing pump and pressure storage device; these compensate for minor pressure fluctuations in the network, preventing the main fire pump from starting unnecessarily due to slight pressure drops and helping to maintain the network’s standby pressure. The control cabinet manages system operation, offering automatic or manual control modes and monitoring system status via pressure gauges and sensors; it also incorporates electrical protection functions, enabling centralized operation and control of the equipment. This series of complete diesel fire pump units offers a wide range of parameter configurations; product specifications indicate that certain system packages cover flow rates of 30–9000 GPM and discharge pressures of approximately 3–20 Bar. Specific parameters must be selected and matched based on the fire protection system’s design flow rate, head, pipe diameter, pressure rating, water source conditions, and on-site installation environment. By integrating the power system, pumping system, pressure management components, control system, and piping accessories into a unified assembly, the equipment minimizes the coordination challenges associated with the scattered layout of individual components. It also establishes clear interconnections between functional units, thereby facilitating system commissioning, operational monitoring, and routine maintenance. For fire water supply projects in sectors such as industrial manufacturing, warehousing and logistics, and large-scale commercial buildings, properly matching the diesel engine power, pump type, flow rate, head, and piping components to actual operating conditions ensures that the unit’s hydraulic performance aligns with system design requirements, providing a stable emergency water supply for fixed fire piping networks, fire hydrants, and automatic sprinkler systems.